TS7000-user-guide.pdf - 第6页
6 5.3 Air connection: Filtered air supply must be precisel y regulated and should be set between 1-30 psi, depending on material viscosit y. The air supply is not used as the main dispensing forc e. It is o nly required …
12
11. TROUBLESHOOTING
PROBLEM POSSIBLE CAUSE CORRECTION
No Material Flow
Dispense tip is plugged Replace tip
Motor does not receive
signal
Make sure all connections are
secured
Motor running in reverse
Reverse motor cable
connection
Barrel of dispense material
is emptied
Replace with new material
barrel
Material feed pressure is too
low
Increase feed pressure.
Material dried or cured
Replace with new fresh
material
Inconsistent
Shot size
Material pressure
fluctuating
Make sure material pressure is
constant
Valve on time is too short Increased valve on time
Excessive motor reverse
time
Reduce reverse time or turn off
completely.
Air trapped in material Purge valve properly
Feed screw damaged Replace feed screw
Skipped dots Air trapped in material De-air material
Material drools
after the valve
turned off
Air trapped in feed screw
chamber
Purge valve properly
Air trapped in material
reservoir
Remove air from reservoir
Excessive material feed
pressure
Reduce pressure or turn off
pressure when the valve is
idled.
5
5. SETUP INSTRUCTIONS
5.1 Mechanical Mounting:
Normally, the TS7000 valve is used on an automated XYZ table with full
motion control in the three planes. It is very important that the valve be
mounted on the Z-axis gantry in a secure manner that will not allow
loosening during dispense operation. The Z-axis must move in a precise
and repeatable motion for successful dispensing.
The provided mounting bracket, or customer supplied bracket, must be
attached to the Z-axis in a manner that will provide the valve
perpendicular travel to the horizontal plane of the surface on which the
material will be dispensed. The mounting should provide a means of
accurately adjusting the gap between the dispense tip and the substrate
surface such as a touchdown sensing device or a fixed distance standoff.
5.2 Electrical Connection:
The TS7000 series valve requires an electrical connection of two wires
for the DC motor. The motor lead wires are 24” long. The black lead
wire should be connected to the negative or neutral lead from the motor
control voltage source. To verify the connection, check the rotation
direction of the feed screw. When correctly connected, a positive voltage
signal will drive the feed screw in a counter clockwise direction when
viewed from the dispense tip end.
The recommended controller for the TS7000 series valve is the TS500R.
If another controller is used make sure the control voltage signal is
precisely controlled. The signal should be from a regulated power supply
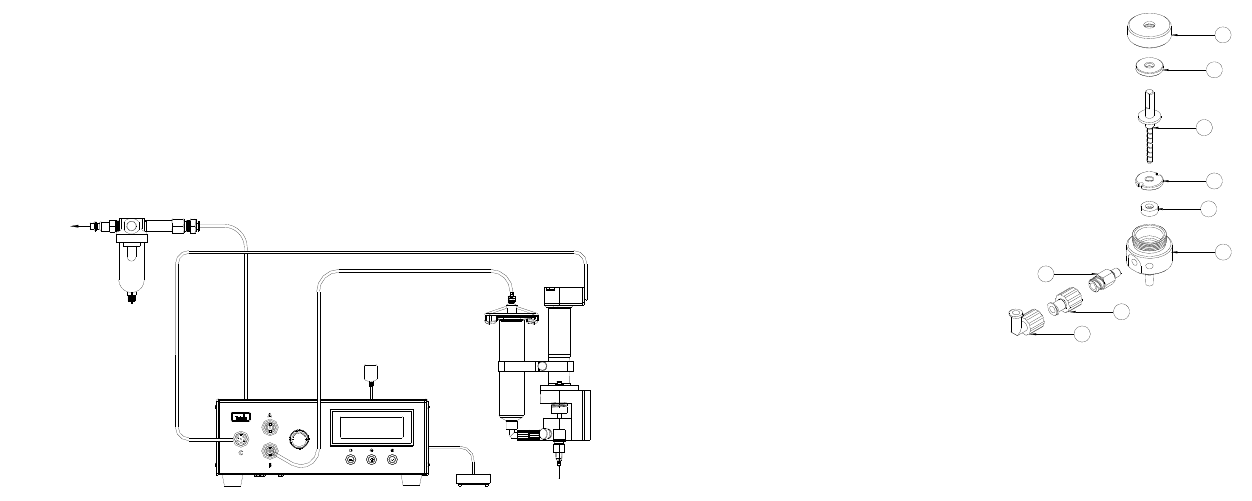
and should be shunted to positive motor stop. Below is a diagram of a
simple braking circuit:
Figure 3.0
6
5.3 Air connection:
Filtered air supply must be precisely regulated and should be set between
1-30 psi, depending on material viscosity. The air supply is not used as
the main dispensing force. It is only required to move the material to the
feed screw chamber.
The valve is supplied with sample of 10 and 30cc air powered syringe
assembly. The syringe of material can be mounted directly onto the
valve inlet fitting. Material can also be supplied from a remotely located
container, such as cartridge systems.
Figure 4.0 Typical Setup Systems
6. DISPENSING APPLICATIONS
6.1 DC Motor Voltage Level:
Voltage controls motor speed (RPM). High voltage produces high motor
speed and low voltage reduces motor speed. Maximum Voltage input is
24 VDC
6.2 Feed screw pitch:
Rate of material dispensed is determined by the pitch of the feed screw. A
high pitch number will produce a low dispense rate and a low pitch
number will produce a higher dispense rate.
6.3 Dispense tip:
The size of the dot diameter or bead width is determined by the dispense
tip. A low gauge number (larger I.D.) will dispense a large diameter dot
or a wide bead. A high gauge number (smaller I.D.) will dispense a
smaller diameter dot or a narrower bead.
Dispense tip sizes smaller than 25-gauge and longer than 1/2" are not
recommended to use with solder paste. A normal rule of thumb to choose
the dispense tip size is that the dot size equal 1.5 times the internal
diameter of the dispense tip.
TS500R CONTROLLER
TS7000 VALVE
TO AIR SOURCE
AIR MUST BE
FILTER AND DRY
11
Figure 7.0
1. Follow steps 1-6 in Section 10.1 “Valve Purging”
2. Follow steps 1- 5 in Section 7.1 “Removing the Cartridge assembly”
3. Remove the Material Inlet Fitting (7) along with the Luer Lock
adapter (8) and Luer Lock Elbow fitting (9) from the Cartridge
4. Remove the Cartridge Cap (1) by turning it counter clockwise
5. Pull the Feed Screw (3) straight out of the Cartridge; Make sure not
to lose the upper bearing washer (2)
6. Using the tweezers (provided in the cleaning kit) to remove the lower
bearing washer (4)
7. Using a cotton swap, carefully remove the seal (5) from the cartridge.
8. Clean all parts using the cleaning brush with any suitable solvent
9. Inspect parts for wear or damage and replace if necessary
10. Re-install the seal (5) into the Cartridge body, make sure the spring
side is facing down
11. Fully press the lower bearing (4) washer into the Cartridge body
12. Insert the Feed Screw (3) into the Cartridge body, make sure not to
damage the seal
13. Install the upper bearing washer (2) on the Feed Screw flange
14. Tighten the Cartridge Cap (1)
15. Install the Material Inlet Fitting (7)
16. Install the Cartridge assembly into valve housing
17. Purge Valve per Section 10.1
1
2
3
4
5
6
8
9
7
10
2. Remove the two bracket mounting screws (5) and pull the valve
housing (7) away from the main housing (6)
3. Install a square drive adapter (include in the 7000-DMPBKIT) to the
flexible coupling (4) and tighten the set screw
4. Install the DMP bracket (include in the 7000-DMPBKIT)into the
main housing (6)
5. Install the DMP valve housing to the valve bracket
10. MAINTENANCE AND CLEANING:
10.1 Valve Purging:
Purging the valve with dispensing conditioner (7105XCON) between
shifts or after every eight hours of dispensing is recommended. The
conditioner cleans any material residue from the material path and
conditions the valve for future use.
1. Release material pressure.
2. Remove barrel of material from the valve.
3. Remove dispense tip
4. Install a barrel of dispensing conditioner (Part number 7105XCON)
to the valve inlet and set air pressure at 8.0 psi.
5. Turn on the valve and let it run until the conditioner is the only
material being dispensed at the valve outlet. If the conditioner is
unable to force the dispense material out the valve outlet then
proceed to the “Thorough Cleaning” section.
6. Turn off valve and release air pressure.
10.2 Thorough Cleaning:
Through cleaning procedures should be done whenever the following occur:
• Dispense material is changed to different type
• Dispense material started to cure in the valve
• Valve has been dispensing for one month.
• Dispense tip clogged frequently
7
6.4 Material feed pressure:
The material feed pressure does affect the amount of material dispensed
through the valve. Optimum feed pressure is dependent upon viscosity of
material dispensed. Only in unusual circumstances should the feed
pressure exceed 30 psi.
6.5 Dispense Material:
The viscosity of the dispense material along with the particulate additives
to the dispense material will also determine the dispense rate. Ability to
dispense may be directly related to the material formulation.
6.6 Dispense cut off:
The best method of stopping material flow at the end of the cycle is to
short the motor (grounding the DC voltage signal through a current
limiting resistor). This method provides a complete rotational brake of the
motor at the shut off point. Another method of stopping material flow is
to reverse the motor rotation by reversing the DC voltage signal. This can
be described as suck-back action. In both cases, a no-drip dispensing
action can be achieved. Turning off the material feed pressure when the
valve is not dispensing will prevent dripping and oozing.
6.7 Dispense tip height:
The distance between the dispense tip and substrate surface is extremely
important. To obtain accurate dot size, the dispense tip height should
remain constant for each dot/bead. If the dispense tip height fluctuates
during dispense process, the dot/bead size will vary. If the dispense tip
touches the dispense surface, clogging will occur.
6.8 Material condition:
The physical condition of the dispense material is very important to
successful dispensing. There are a number of conditions that can prevent
continuous and consistent dispensing such as:
• Freshness: Old material (most materials have a recommended shelf
life) leads to erratic dispensing and frequent clogging, especially with
solder paste. Make sure to check the material shelf life before
starting dispensing.
• Separation: Material with high content of solid particles, such as
solder paste, tends to separate at high pressure. If the dispense
material starts to separate, please replace it with new fresh material.
• Particles sizing: Do not attempt to dispense solder paste with particle
sizes bigger than 75 microns (-200+325 mesh size).