Operation BWP Issue 2.pdf - 第16页
16 Issue 2, Nov 14 Objectiv e OP & BWP 8 – Recov er from common error messages Reference: Machine Opera tor manual Fast track erro r recovery guide, part no. 158 184 Although following the proce dures in the operator…
Issue 2, Nov 14
15
Objective BWP 7 – Consumable best working practices
Reference: Operator best working practices
Experience has shown that there are tips and techniques that can be used to minimise the
disruption caused to production throughput when replenishing consumable materials.
Preparation
Tick off each of the following items as you complete them:
Review the replenishment section in the best working practices manual
Demonstration
Tick off each of the following items as you complete them:
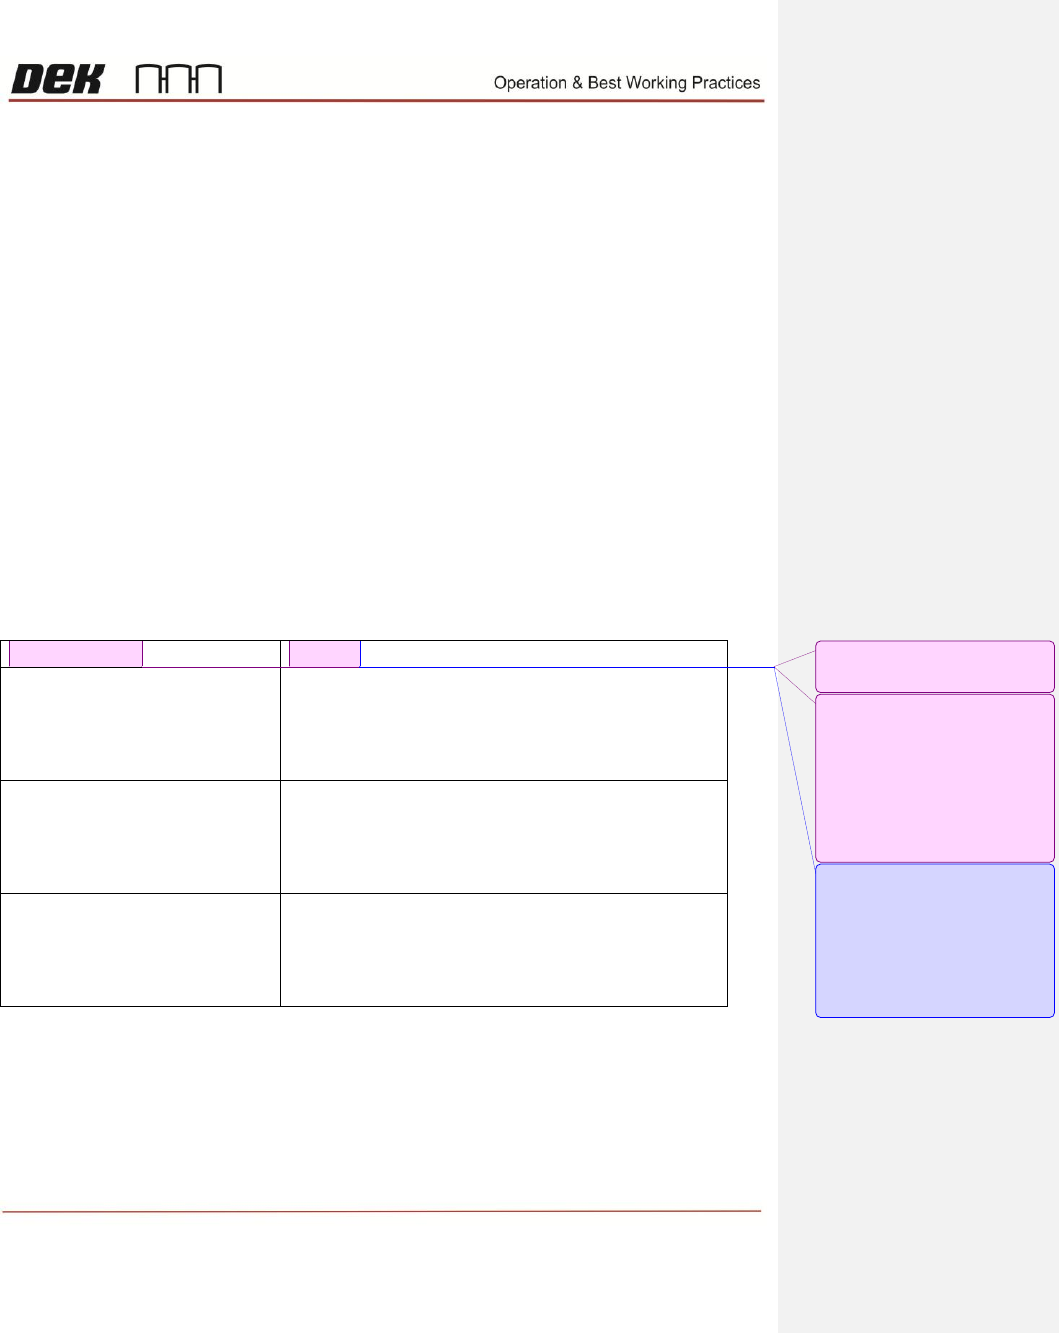
Complete the table below listing the consumable items that you will be responsible
for replenishing
Identify the BWP which you can employ
Consumable
BWP’s
Comment [JS12]: USC Paper, USC
solvent, USC general condition, Print
material
Comment [JS13]: Keep a spare roll
of paper close to machine, when
changing paper check condition of
pipes and cables and usc blades, keep
a funnel close to machine, remove
solvent spills immediately, do not mix
solvent types, make small top ups of
material regularly rather than large top
ups, ensure that adequate quantities of
acclimatised material is readily
available.
Comment [t14]: Page: 11
Plugged in,Switched on,Temperature
matches production data sheet,Hose
routed correctly
Plugged in,Switched on
Free from damage,Clean
Surface clean and free from debris
Spare roll next to machine,Adequate
quantity of paste being acclimatised
16
Issue 2, Nov 14
Objective OP & BWP 8 – Recover from common error messages
Reference: Machine Operator manual
Fast track error recovery guide, part no. 158184
Although following the procedures in the operator manually carefully will prevent most
errors there will be occasions during production when error messages will be observed on
the printer. It is important to quickly determine a) what may have caused the error b)
whether you have the skills to rectify the problem c) whether the problem should be
escalated. Performing this task efficiently will minimise machine downtime and loss of
production.
Preparation
Tick off each of the following items as you complete them:
Refer to the error messages listed in the operator manual
Your instructor will simulate all of the common errors listed below
Demonstration
Having completed the preparation phase, now complete the actions below. Tick off each
item as you complete them:
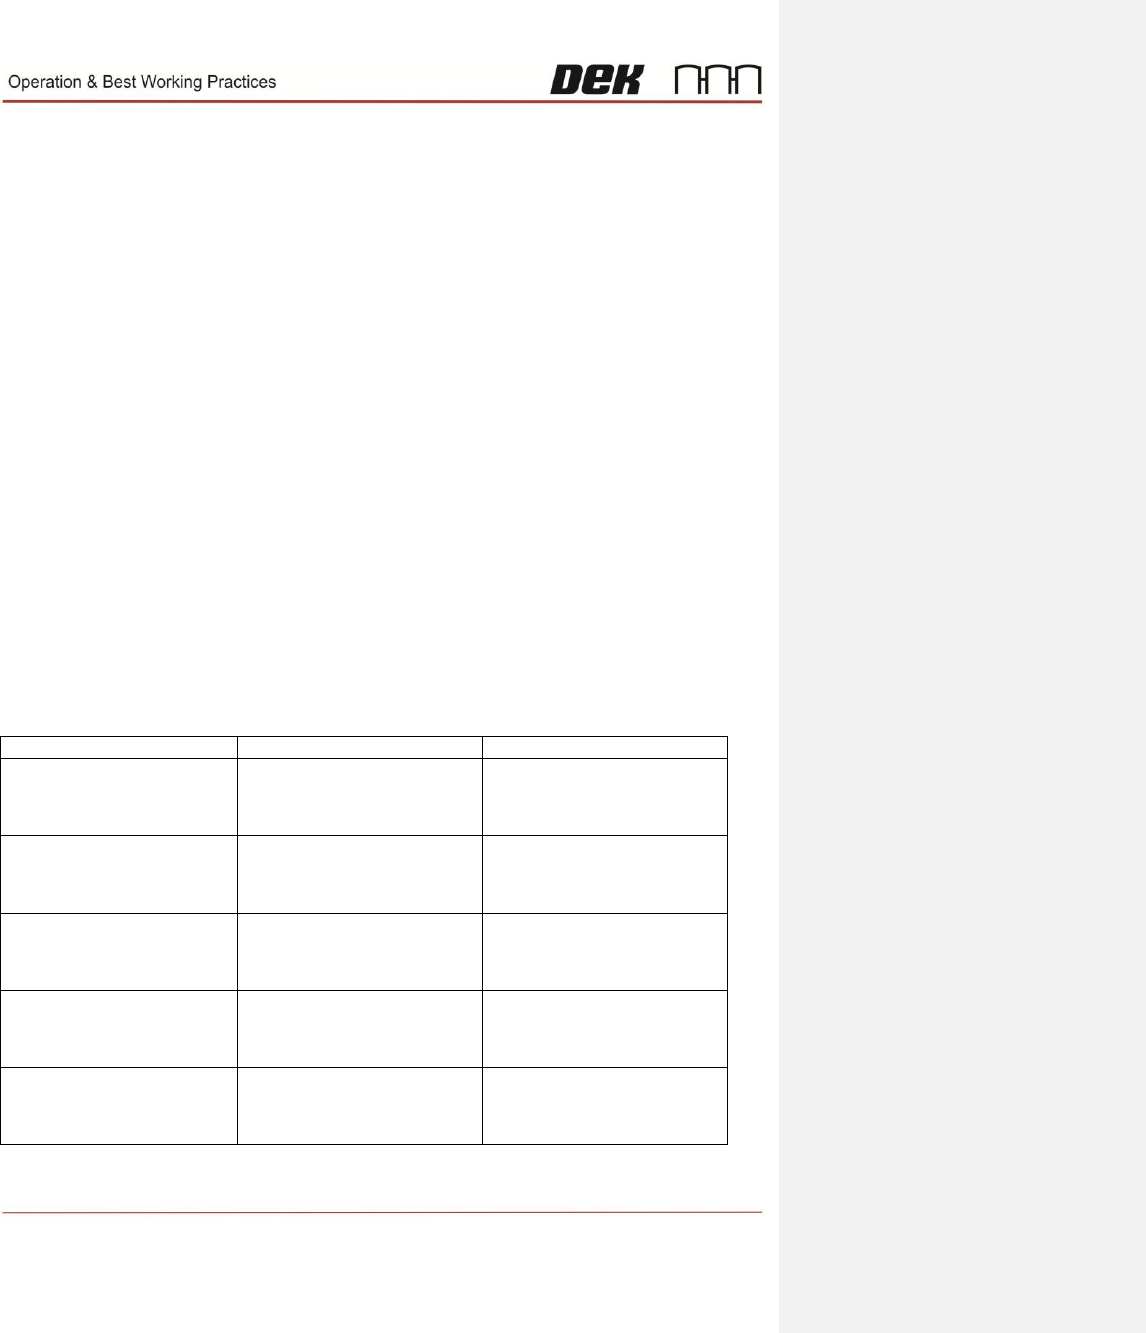
Whilst referring to the fast track recovery guide complete the table below providing
the most likely cause of these common error messages and the recovery actions
Recover from at least one simulated error
Message
Cause
Remedy
Fiducial not found
Screen cleaner out of
position
Rail lifted error
System power down
Board transfer fault
Issue 2, Nov 14
17
Objectives OP 9 - Identify common print defects
Reference: Fast track process recovery guide, part no. 158546
Although following the procedures in the operator manual carefully will prevent most print
defects there will be occasions during production when print defects occur.
It is important that the operator understands which areas under their control can have a
direct influence over the print quality and how to identify a defect and quickly rectify the
problem.
Preparation
Tick off each of the following items as you complete them:
Discuss with you instructor the specifications of an acceptable quality print (refer to
your companies guidelines if available)
Your instructor will discuss a series of common print defects and identify the likely
operational causes as detailed in the recovery guide
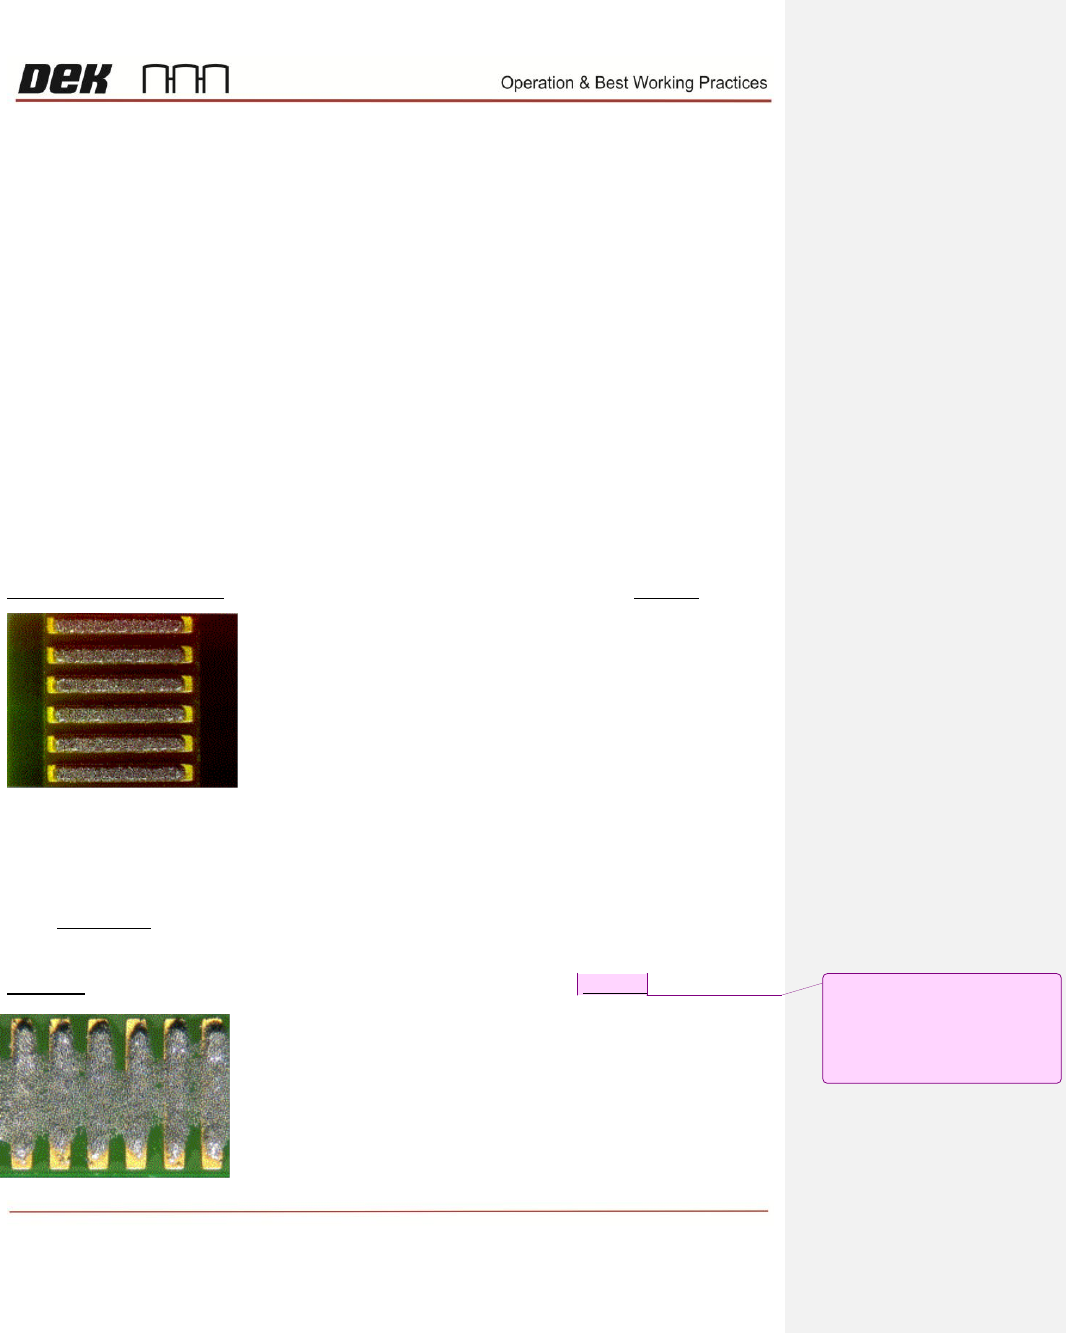
The Perfect Solder Print Causes
Good alignment
No gaps between board and stencil
Good board support
Good stencil support (ProFlow)
Good stencil (good design, undamaged, Clean)
Good material (condition, temp etc)
Correct parameter settings (match process design)
Demonstration
Shown below are some common solder print defects. Suggest some common
operational causes of these defects
Bridging Causes
Comment [JS15]: Solder Paste too
hot
Tooling too high or missing
Board warped
Misalignment
Stencil damaged
Damaged squeegees / ProFlow