Horizon Generic Tooling.pdf - 第3页
MACHI NE PROG RAMMI NG STAGE 5 A - M AGNET IC PILL ARS TOO LING User Manual 1.19 15. Sel ect Conti nue (F1). Cleaner moves to the Home position and the print carria ge moves to the rear of the machi ne. The message ‘T ab…
MACHINE PROGRAMMING
STAGE 5A - MAGNETIC PILLARS TOOLING
1.18 User Manual
8. Setting up the board stop position is automatically done using the board
dimensions previously set in the product file. If they need adjustment to re-
position the board stop for any reason, ie any routing on the board edge or
a badly positioned image on the stencil, this can be done now. If adjustment
is necessary continue with Step 9. If adjustment is not necessary go to Step
14.
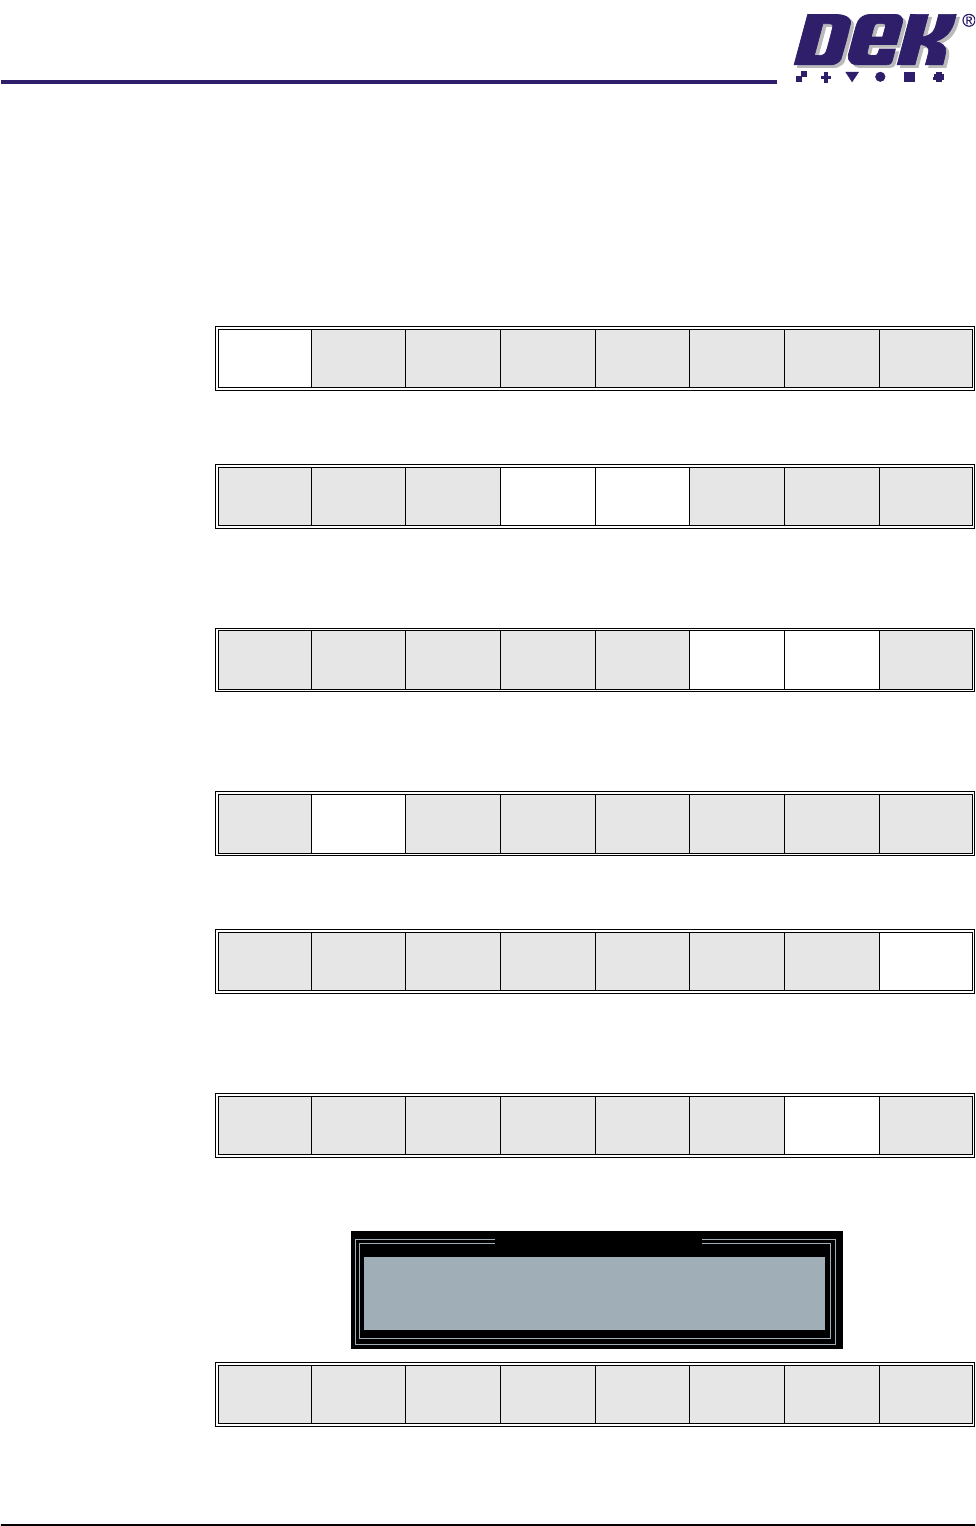
9. Select Adjust (F1).
10. Use the Next and Previous keys (F4 - F5) to highlight each parameter.
11. Use the Incr. and Decr. keys (F6 - F7), or the forward slash key (/) on the
keyboard, to change the parameter value.
12. Select Save (F2). The message ‘Saving fiducial data - Please wait Board
data file saved’ is displayed.
13. Select Exit (F8).
14. Select Generic Tooling (F7). The print carriage moves to the front of the
machine.
The following window and menu bar is displayed:
NOTE
If contaminated squeegees are fitted, these should be replaced at this point.
Adjust
Open
Cover
Home
Cleaner
Board
Stop
Full
Width
Load
Width
Generic
Tool ing
Exit
Save Next Previous Incr. Decr. Exit
Save Next Previous Incr. Decr. Exit
Save Next Previous Incr. Decr. Exit
Save Next Previous Incr. Decr. Exit
Adjust
Open
Cover
Home
Cleaner
Board
Stop
Full
Width
Load
Width
Generic
Tooling
Exit
Generic Tooling Warning
WARNING Paste may drip into the machine
Remove Squeegees NOW
Continue
Open
Cover
Exit
MACHINE PROGRAMMING
STAGE 5A - MAGNETIC PILLARS TOOLING
User Manual 1.19
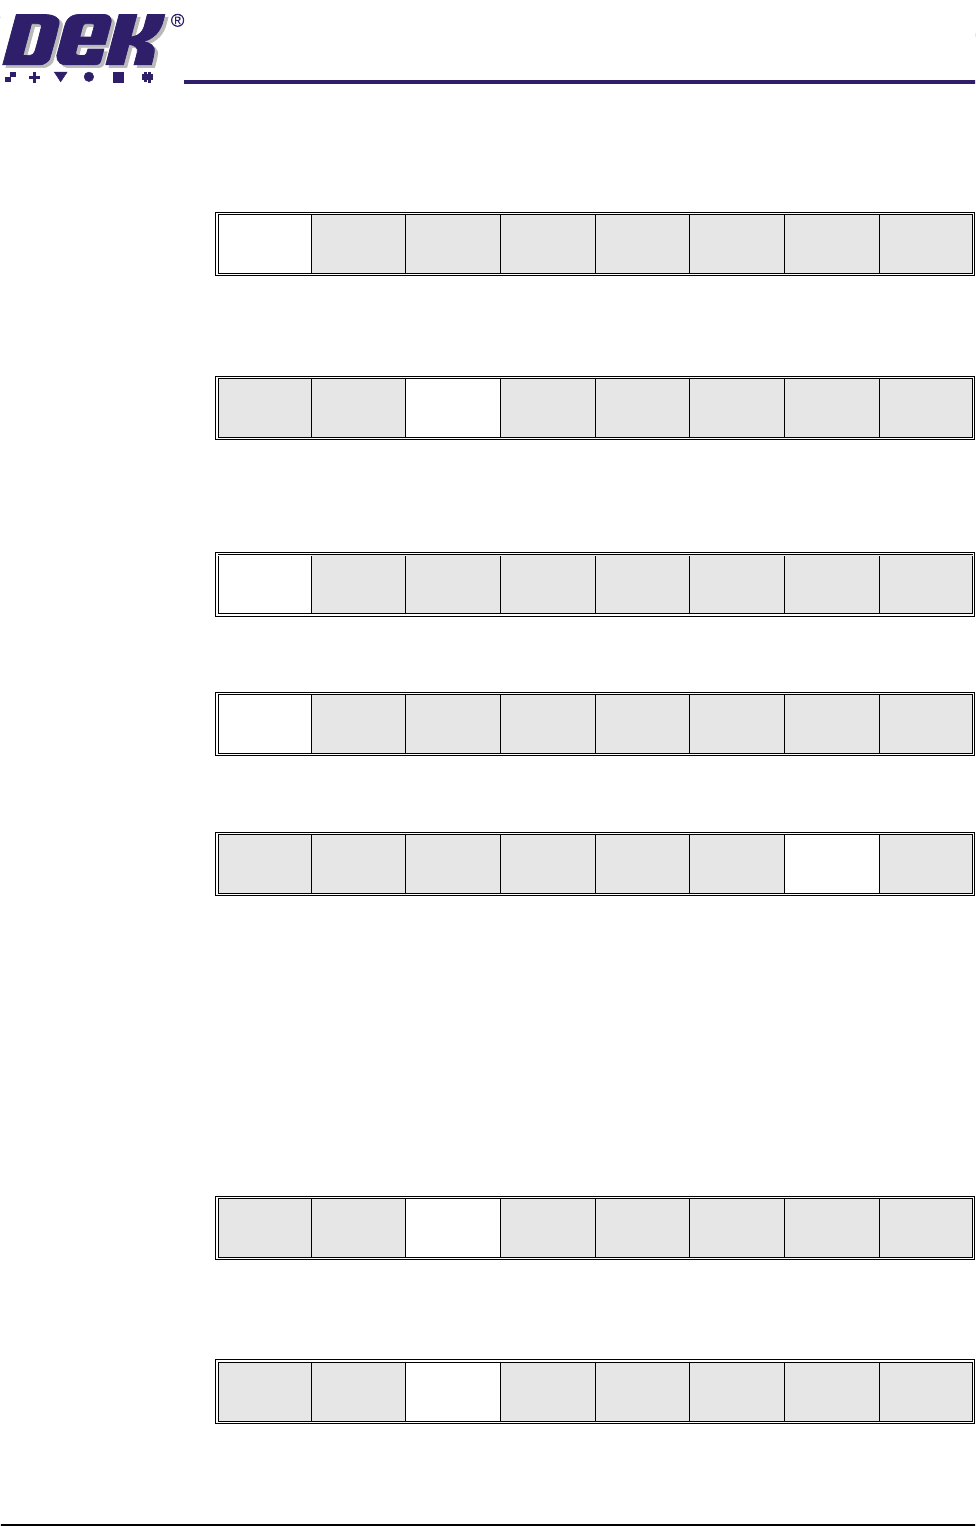
15. Select Continue (F1). Cleaner moves to the Home position and the print
carriage moves to the rear of the machine. The message ‘Table at Home
Height’ is displayed.
16. Select Transprt Height (F3). The message ‘Table at Transport Height’ is
displayed.
17. Place a board on the input sensor of the upline conveyor of the machine.
18. Select Load (F1).
19. Select Auto Board (F1).
20. Select Open Cover (F7).
21. Either:
a. Open the front printhead cover.
or
b. Raise the printhead shutter.
22. Position the outermost magnetic support pins on the rising table under the
board.
23. Select Board Clamps (F3) to open the clamps.
24. Remove the board from the rails and select Board Clamps (F3) to close the
clamps.
25. Complete the positioning of the magnetic support pins.
26. Place the board back on the rails over the tooling.
Continue
Open
Cover
Exit
Load
Transprt
Height
Board
Clamps
Change
Screen
Open
Cover
Exit
Load
Vision
Height
Home
Height
Board
Clamps
Change
Screen
Open
Cover
Exit
Auto
Board
Manual
Board
Exit
Unload
Vision
Height
Home
Height
Board
Clamps
Change
Screen
Open
Cover
Exit
Board
Clamps
Exit
Board
Clamps
Exit
MACHINE PROGRAMMING
STAGE 5A - MAGNETIC PILLARS TOOLING
1.20 User Manual
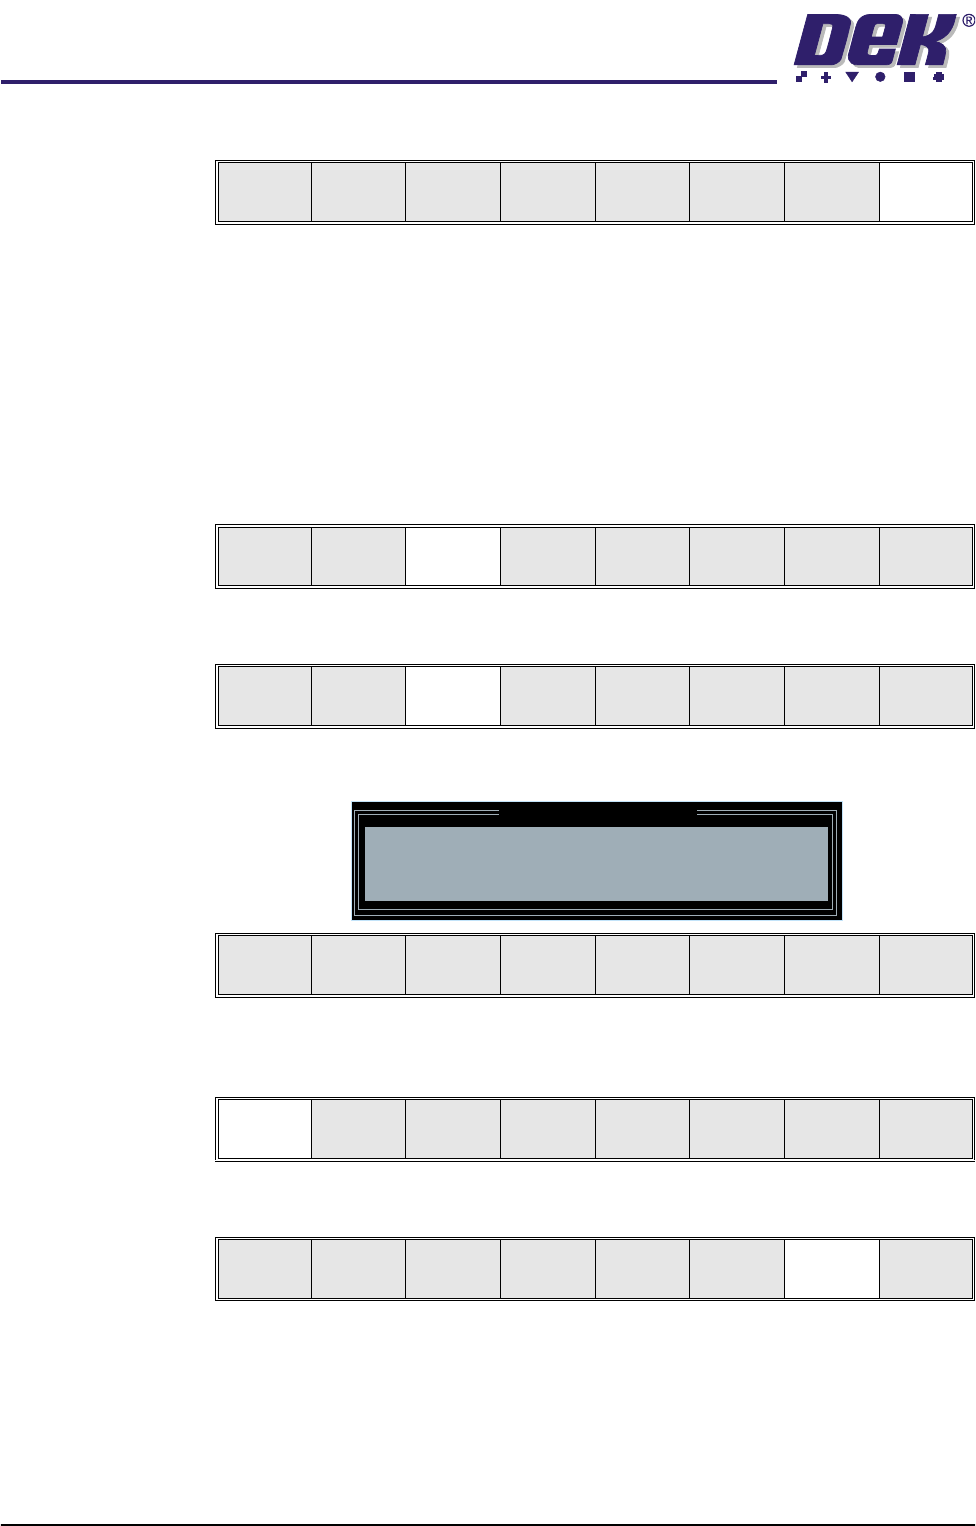
27. Select Exit (F8).
28. Either:
a. Close the front printhead cover.
or
b. Lower the printhead shutter.
29. Press the System button.
30. Select Vision Height (F3). The message ‘Table at Vision Height. Check
Tooling Clearance’ is displayed.
31. Select Contact Height (F3).
The following window and menu bar is displayed:
32. Select Continue (F1). The message ‘Table at Contact Height. Check
Tooling Clearance’ is displayed.
33. Select Open Cover (F7).
34. Either:
a. Open the front printhead cover.
or
b. Raise the printhead shutter.
Board
Clamps
Exit
Unload
Vision
Height
Home
Height
Board
Clamps
Change
Screen
Open
Cover
Exit
Contact
Height
Tra nsp r t
Height
Change
Screen
Open
Cover
Exit
Contact Height Warning
WARNING Check for obstructions between
the Rails and the Screen
Continue
Open
Cover
Exit
Continue
Open
Cover
Exit
Vision
Height
Open
Cover
Exit