User-Manual-NeoDen-IN12-Reflow-oven.pdf - 第21页
20 heating sp eed Decrease transfer spee d and temperature Excessive fines Top layer temperature out of limit Reduce top heat an d increa se b ottom zone temperature Tin balls Due to dry too fast Decrease transfer cha in…
19
different areas, the setting temperature of PCBs with few pads is correspondingly
lower. There is also a certain connection with the amount of boards released per unit
time. However, in normal production, the soldering machine has its own adjustment
system for general PCB board changes. The soldering machine can be used for normal
production at the recommended temperature during training, unless the heat absorption
of the PCB changes significantly.,then need do adjust accordingly.
7.Temperature Testing Way
♦Attach the temperature thermocouple sensor to a same or similar size PCB to observe
the soldering. Put the PCB to the conveyor chain,then generate the temperature
profile,compare to the recommended temperature profile. If it is same or similar to the
self-adjusting profile, then you can start production, otherwise, according to the
temperature profile, adjust the temperature control area to increase and decrease the set
temperature by about 5 degrees in large temperature difference area, or do
comprehensive adjustment of whole machine to get a temperature profile that can be
used for production work.
♦When starting to put PCB or abruptly change the number of PCB, there is a
difference between the actual temperature and setting temperature. The difference
will turn to normal range when putting the PCB with constant speed for a while.
8. Double sided board soldering instruction
♦Use hot air reflow soldering can finish double-side component soldering. Double-
side soldering design means components are in double-side of the PCB need to
soldering. Double side soldering includes double-side soldering tin and single-side
soldering tin and another side drying glue, as for single-side soldering tin and
another side drying glue, it is easier. First, finish one side’s soldering tin as the
same as single-side, then finish another side tape glue drying in low temperature,
finish double-side SMT craft, after that carry on the next step plug-in or tin process
on craft. Double-side soldering is generally treated as below follows:
♦Start the reflow oven, set up the transfer chain speed controller, finish the A side
components reflow soldering with normal soldering craft.
♦Upend the PCB, repeat normal procedure to mount the component, adopt top
heating strategy to let the B side reflow soldering, but the upend A side has been
reflow soldering, the compounds in thick liquid volatilize, the melting point of tin
is higher than the solder paste, which in order to keep the A side components not
fall out.
9. Trouble shooting
9.1 Soldering analysis
Problem
Possible causes
Solutions be available
Incomplete
reflow
Inadequate heating
lower the transfer chain speed
Shadows from components
a. Increase the transfer chain speed
b. Increase bottom heat
Due to the middle layer of copper foil
Decrease transfer chain speed and increase
temperature
Inadequate
moist
PCB, components without enough solder
paste
Pre-paste to components and PCB
No enough moist time
Increase the temperature of heating zone
PCB bend
Exceeding upper and lower temperature
difference limits
Reduce temperature difference between
preheating zone and bottom temperature zone
Increase transfer chain speed
PCB
discoloration
Exceeding tin temperature on the board,
exceeding temperature gradient or
Increase transfer chain speed
Decrease the preset zone temperature
20
heating speed
Decrease transfer speed and temperature
Excessive fines
Top layer temperature out of limit
Reduce top heat and increase bottom zone
temperature
Tin balls
Due to dry too fast
Decrease transfer chain speed and temperature
Solder pasting is unqualified or PCB re-
paste
Use PCB after cleaning and drying
Flux coking
Over heating
Add transfer chain speed, lower temperature
Components
wrong position
PNP wrongly, the tin on the solder pad is
irregular or asymmetrical, drying too fast
causes airflow to blow components
Check place position
Check the shape and thickness of tin
Lower transfer chain speed and temperature
Tin bridging
Misposition
Check position
Tin migration
Moist overtime
Increase the belt speed
Lower pre-setting temperature
Solder skips
The solder paste is not enough on pad,
the unevenness of the micro-component,
the PCB coplanarity problem
Thickened tin paste coating
Try to make the solder on the pad even
Check component pin stability
PCB over heat
Heating speed too fast
Decrease transfer chain speed and temperature
Analysis on the cause of the solder joints not shining
In the SMT soldering process, customers will have requirements for the brightness
of the solder joints. It is often just a subjective consciousness of the customer. We
can only get the conclusion of the brightness through comparison. Because there is
no standard for the brightness of the solder joints; roughly speaking, the reasons
for the non-bright solder joints are as follows:
1. There will be difference between the solder paste with or without silver.
Customers should explain their soldering requirements to the supplier when
choosing solder paste.
2. The tin powder in the solder paste is oxidized.
3. The flux in the solder paste has an additive that causes a matting effect.
4. After soldering, there are rosin or resin residues on the surface of the solder
joints, which is a phenomenon we often see in actual work. Especially when
choosing rosin-type solder paste, although rosin-type flux will make the solder
joints slightly brighter than no-clean flux, the presence of its residues often affects
this effect. It is more obvious in larger solder joints or IC foot parts; if it can be
cleaned after soldering, I believe the gloss of solder joints should be improved.
5. The preheating temperature of reflow soldering is low, and there are non-volatile
residues on the surface of the solder joint.
The main reasons for solder joints not full are as follows:
1. The activity of the flux in the solder paste is not enough, and the oxidized
substances on the PCB pads or SMD solder joints are not completely removed.
2. The moisture retention of the flux in the solder paste is not good.
3. PCB pads or SMD soldering positions have serious oxidation.
4. During reflow soldering, the preheating time is too long or the preheating
temperature is too high, cause the failure of flux activity in the solder paste.
5. If the solder paste has not been fully stirred or the flux and tin powder have not
been fully fused. If, there will be insufficient tin on some solder joints.
6. Reflow zone temperature too low.
7. Insufficient amount of solder paste at the solder joint.
9.2 Precautions
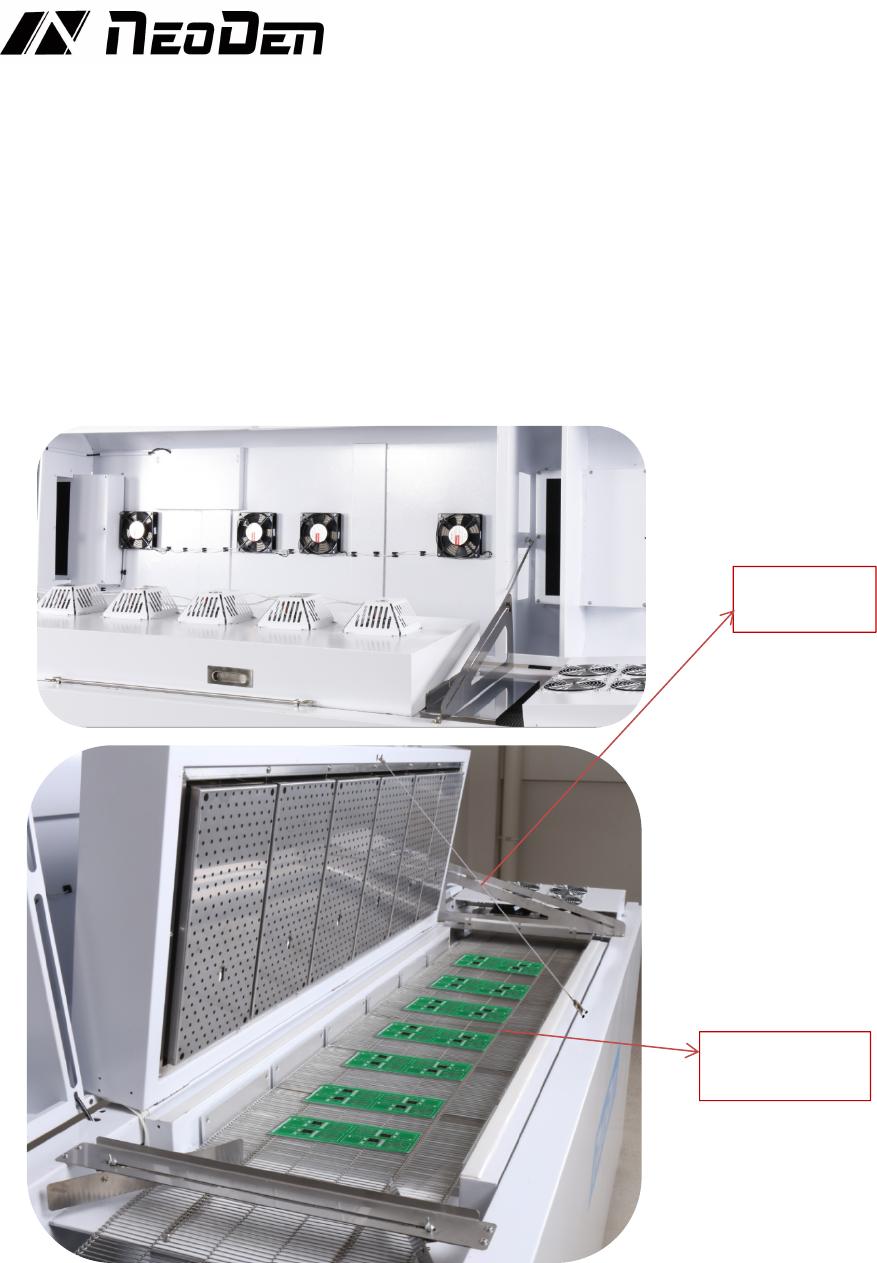
*Keep a certain distance of more than 100mm when PCB size exceeds 100mm.
*If the PCB length is longer than the ESD tray, the ESD tray needs to be replaced by
21
other suitable carriers to place the soldered PCB.
*It is not recommended to open the incubator when it is not necessary. If it must be
opened, the incubator must be supported by a support rod before the next work can be
carried out.
*The upper cover and incubator can only be opened after the bottom caster is lay down.
*The power board and control board should not be touched when the power is on.
*The change of chain speed will affect the plate surface temperature, so after adjusting
the chain speed, be sure to retest the plate surface temperature curve, and adjust the
temperature setting according to the actual test results.
9.3Machine maintenance
♦Replace the filter element assembly regularly
Support Rod
keep distance of
more than 100mm