773564-01_861-862-865_mounting_instructions_en_ge_ch.pdf - 第12页
M8 5.2) 5.3) 12 5.4) 5.1) 5 Check points for mechanical mounting Kontrollpunkte bei mechanischer Montage 机械安装检查要 机械安装检查要 点 点 M5 / M6 90 o
11
Part from customer
Accessories from Leine Linde (to be ordered
separately, see page 20)
Tools for mounting
Kundenkomponente
Zubehör von Leine Linde (separate Bestellung,
siehe Seite 20)
Montagewerkzeug
客户部件
莱纳林德附件 (需单独订 购,参见第 20 页)
安装工具
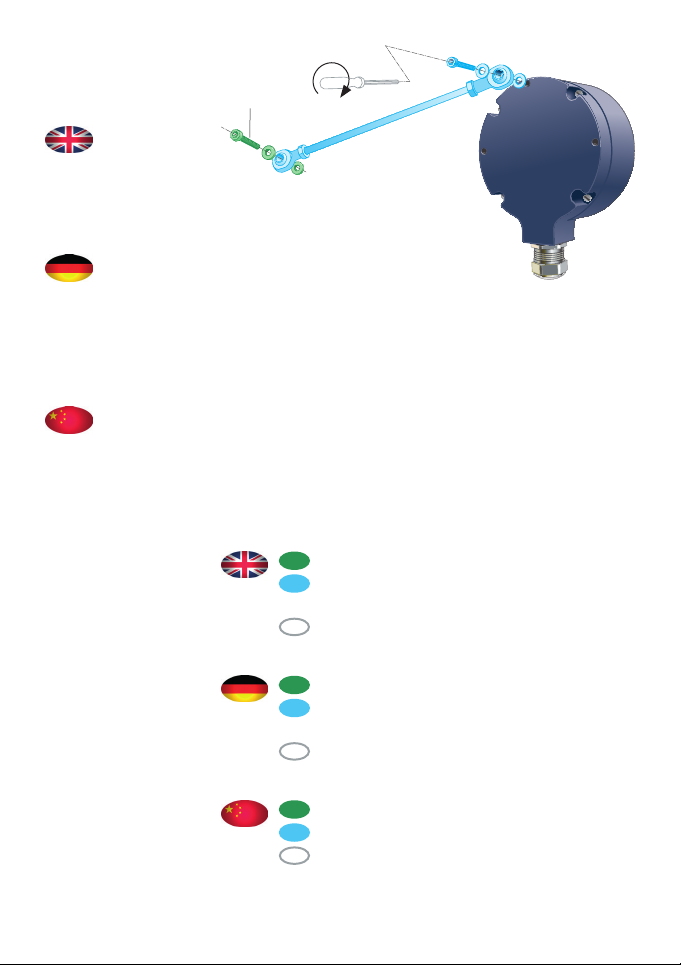
4.3
Alternative
mounting of
torque arm
Alternative
Montage der
Drehmoment-
stütze
可选安装扭臂可选安装扭臂
M5
M5: 5.5 Nm
M8
5.2)
5.3)
12
5.4)
5.1)
5
Check points
for mechanical
mounting
Kontrollpunkte
bei mechanischer
Montage
机械安装检查要机械安装检查要
点点
M5 / M6
90
o
13
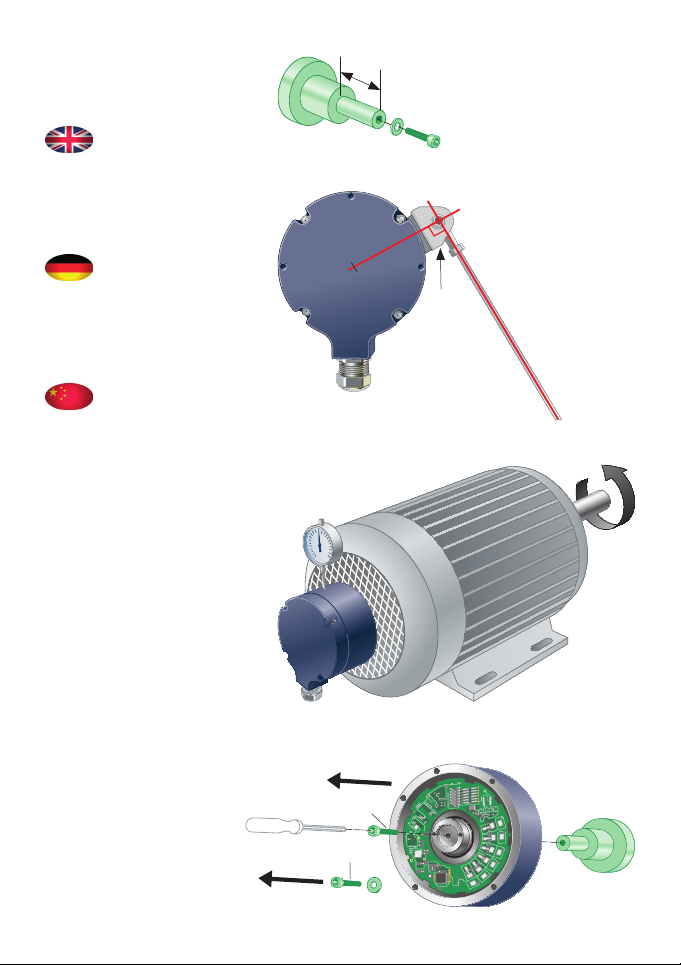
5.1 Check that the dimensions of the mating shaft
match the specifications in the encoder’s data
sheet. Fix the encoder with an M5 or M6 screw
(ISO 4762) with minimum 9 mm thread in use.
5.2 Fix the encoder with an insulated torque arm.
It must be fitted at 90 degrees angle to the direc-
tion of the bracket, for optimum accuracy of
measurement.
5.3 Check the encoder’s radial runout with slow
rotation of complete assembly. The runout
should not exceed 0.1 mm, as this may shorten
the encoder’s service life or influence the system
accuracy.
5.4 Dismounting; Use M8 screw, if necessary, to
detach the encoder.
5.1 Sicherstellen, dass die Abmessungen der Gegen-
welle den Angaben im Drehgeber-Datenblatt
entsprechen. Drehgeber mit einer M5- bzw. M6-
Schraube (ISO 4762) mit mindestens 9-mm-
Gewinde befestigen.
5.2 Drehgeber mit einer isolierten Drehmoment-
stütze befestigen. Um eine optimale Messgenau-
igkeit erzielen zu können, muss die Drehmo-
mentstütze im 90-Grad-Winkel zur Befestigung
montiert werden.
5.3 Radialversatz des Drehgebers bei langsamer
Rotation und fertiger Montage überprüfen. Der
Versatz darf 0,1 mm nicht überschreiten, da
sonst die Lebensdauer des Drehgebers verkürzt
bzw. die Systemgenauigkeit beeinträchtigt
werden kann.
5.4 Demontage: Bei Bedarf beim Drehgeberwechsel
M8-Schraube zum Lösen verwenden.
5.1 检查连接轴的尺寸是否符合编码器数据表中的
规格。使用 M5 或 M6 螺丝 (ISO 4762) 配合最
小 9 mm 螺纹来固定编码器。
5.2 使用绝缘扭矩臂固定编码器。安装角度必须和
托架方向成 90 度,以确保最佳的测量精度。
5.3 通过完整组件的慢速旋转来检查编码器的径向
偏移。偏移不应超过 0.1 mm,否则将缩短编码
器的使用寿命或影响系统的精度。
5.4 如有需要,使用 M8 螺丝以在更换时拆卸编码
器。