ELA Generic Tooling.pdf - 第27页
MACHI NE PROG RAMMI NG STAGE 5 D - MULTIFLEX TOOLING User Manual 1.41 bel t s ’ is disp layed. Whilst the r ear rail i s moving the message ‘Rail moving...’ is displ ayed. 27. Sel ect Generic T ooling (F7). The pri nt ca…
MACHINE PROGRAMMING
STAGE 5D - MULTIFLEX TOOLING
1.40 User Manual
17. Use the Incr. and Decr. keys (F6 - F7), or the forward slash key (/) on the
keyboard, to change the parameter value.
18. Select Save (F2). The message ‘Saving fiducial data - Please wait Board
data file saved’ is displayed.
19. Select Exit (F8).
20. Select Full Width (F5). The message ‘Checking for a board on the belts’
is displayed. Whilst the rear rail is moving the following message ‘Rail
moving...’ is displayed.
21. Select Open Cover (F2).
22. Raise the machine shutter, lower drop down panel.
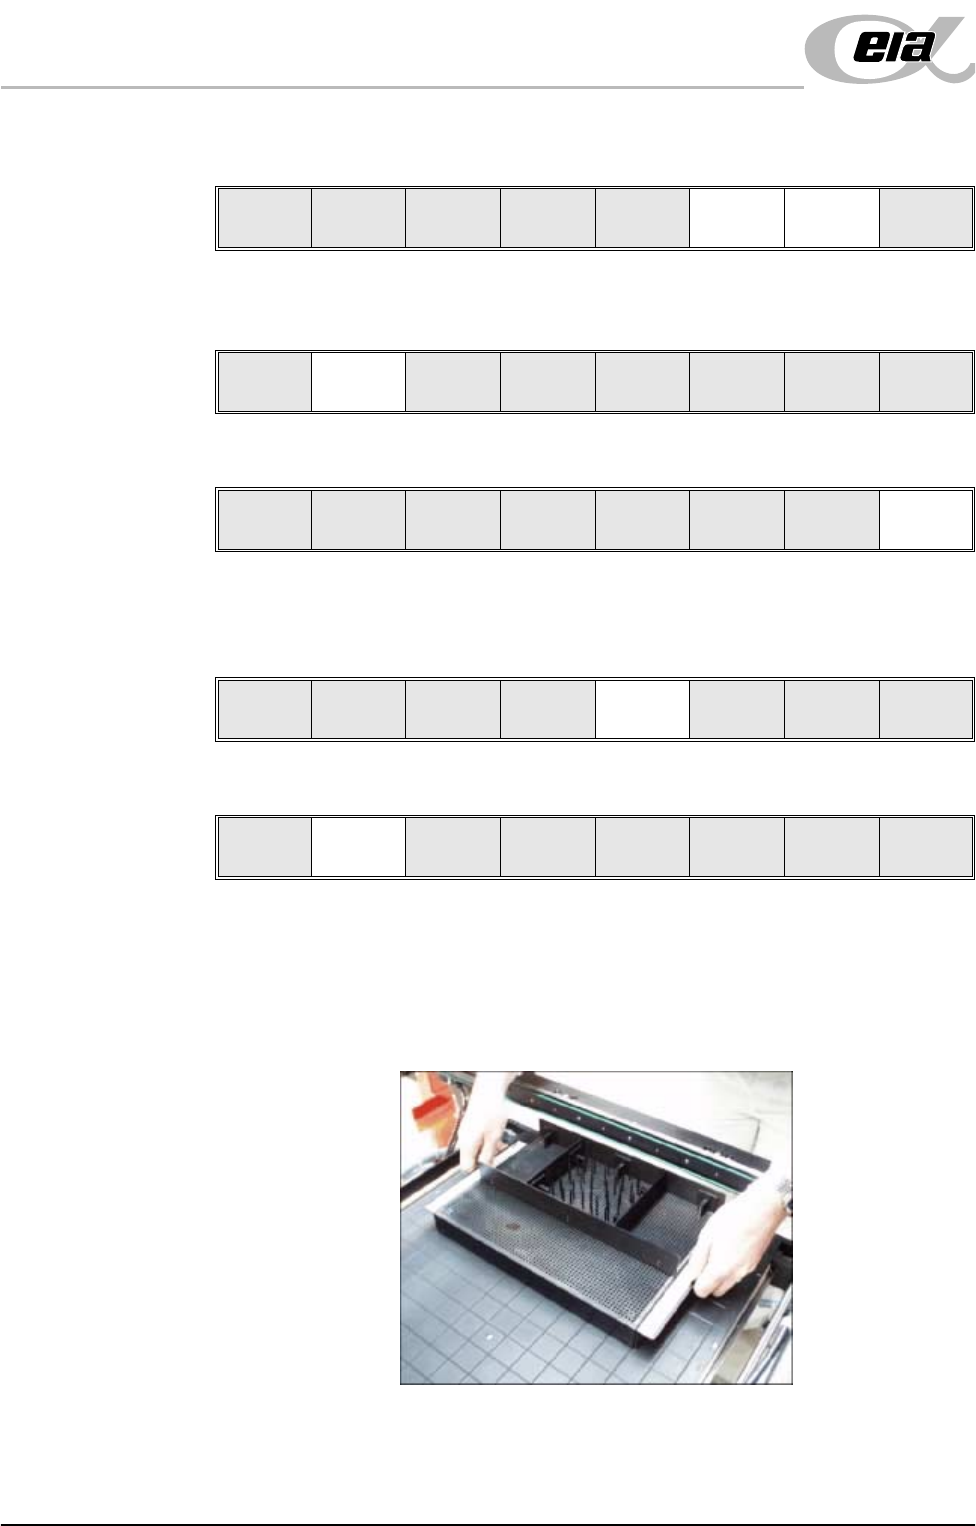
23. The MultiFlex tooling can now be fitted into the appropriate location holes in
the tooling plate. Ensure that the tooling is placed into the correct set of
holes, taking regard of the type of screen being used and hence the position
of the fixed rail.
24. Raise the drop down panel, lower the machine shutter.
25. Press the System button.
26. Select Board Width (F5). The message ‘Checking for a board on the
Save Next Previous Incr. Decr. Exit
Save Next Previous Incr. Decr. Exit
Save Next Previous Incr. Decr. Exit
Adjust
Open
Cover
Home
Cleaner
Board
Stop
Full
Width
Load
Width
Generic
Tooling
Exit
Adjust
Open
Cover
Home
Cleaner
Board
Stop
Board
Width
Load
Width
Generic
Tooling
Exit
MACHINE PROGRAMMING
STAGE 5D - MULTIFLEX TOOLING
User Manual 1.41
belts’ is displayed. Whilst the rear rail is moving the message ‘Rail
moving...’ is displayed.
27. Select Generic Tooling (F7). The print carriage moves to the front of the
machine.
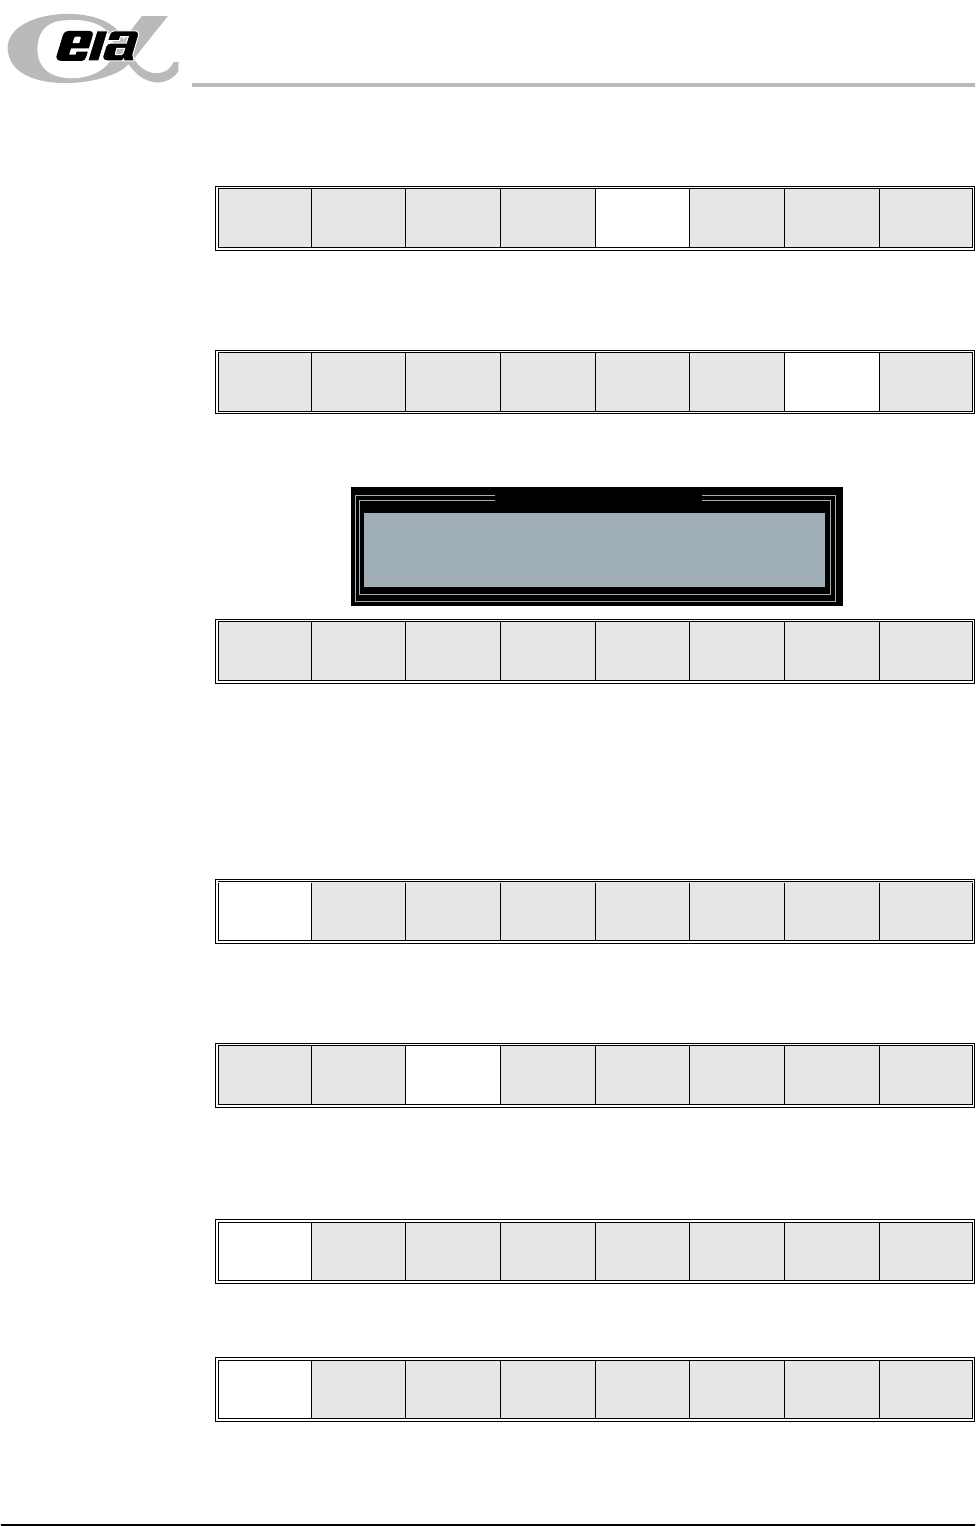
The following window and menu bar is displayed:
NOTE
If contaminated squeegees are fitted, these should be replaced at this point.
28. Select Continue (F1). Cleaner moves to the Home position and the print
carriage moves to the rear of the machine. The message ‘Table at Home
Height’ is displayed.
29. Select Transprt Height (F3). The message ‘Table at Transport Height’ is
displayed.
30. Place a board on the input sensor of the upline conveyor of the machine.
31. Select Load (F1).
32. Select Auto Board (F1).
33. Select Vision Height (F3). The message ‘Table at Vision Height. Check
Adjust
Open
Cover
Home
Cleaner
Board
Stop
Board
Width
Load
Width
Generic
Tooling
Exit
Adjust
Open
Cover
Home
Cleaner
Board
Stop
Full
Width
Load
Width
Generic
Tooling
Exit
Generic Tooling Warning
WARNING Paste may drip into the machine
Remove Squeegees NOW
Continue
Open
Cover
Exit
Continue
Open
Cover
Exit
Load
Transprt
Height
Board
Clamps
Change
Screen
Open
Cover
Exit
Load
Vision
Height
Home
Height
Board
Clamps
Change
Screen
Open
Cover
Exit
Auto
Board
Manual
Board
MACHINE PROGRAMMING
STAGE 5D - MULTIFLEX TOOLING
1.42 User Manual
Tooling Clearance’ is displayed.
34. Select Contact Height (F3).
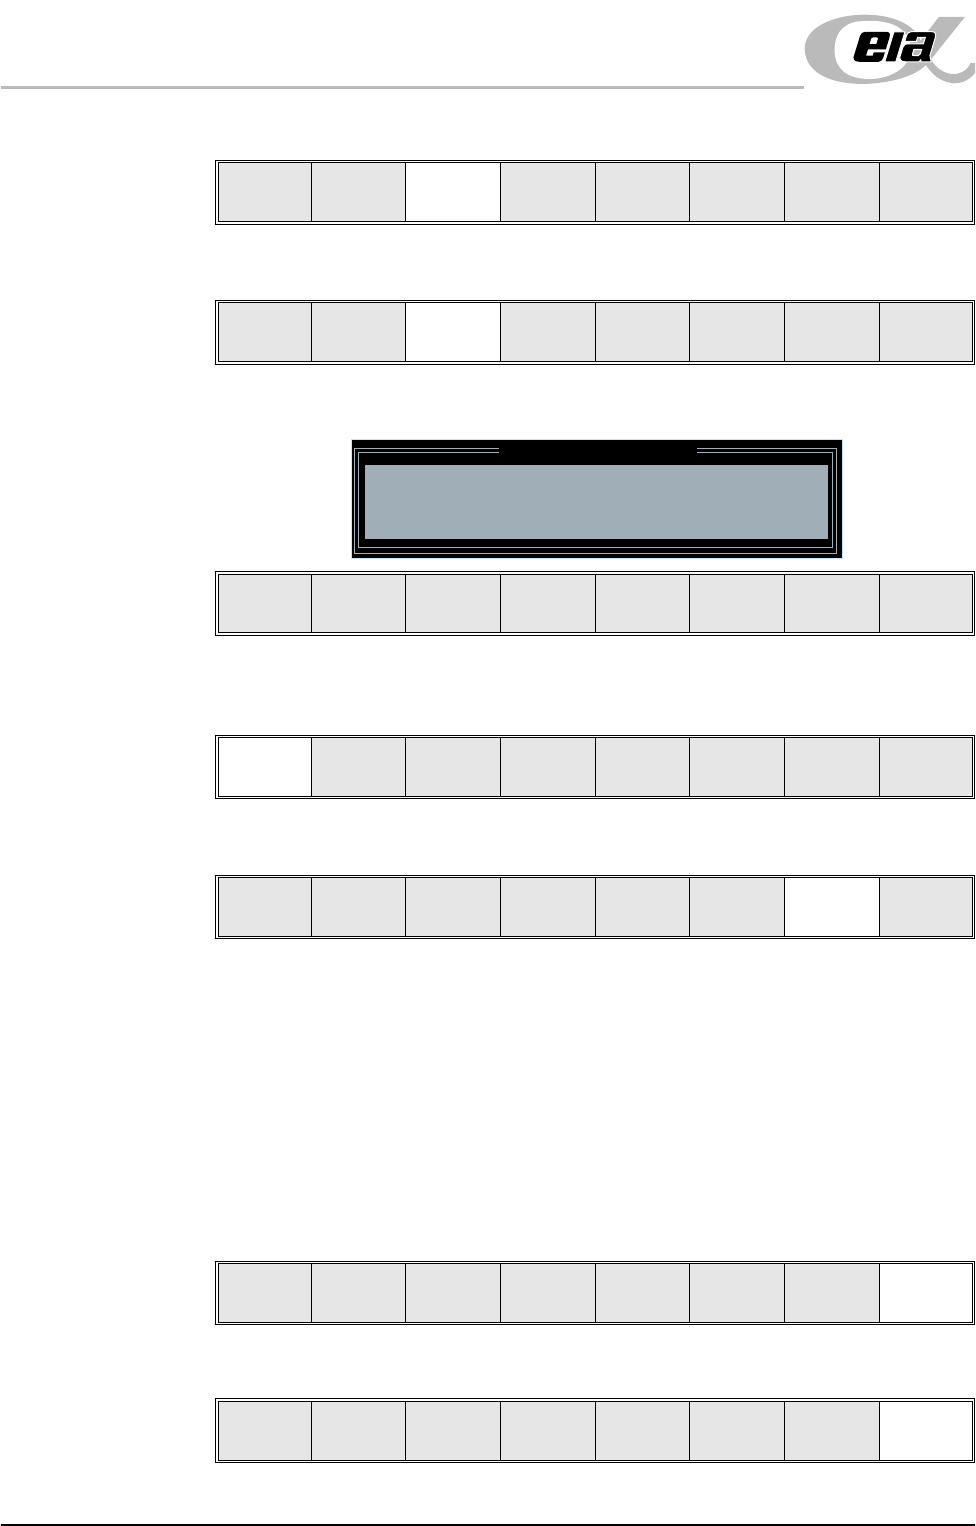
The following window and menu bar is displayed:
35. Select Continue (F1). The message ‘Table at Contact Height. Check
Tooling Clearance’ is displayed.
36. Select Open Cover (F7).
37. Raise the printhead shutter.
38. Check that the setup of the tooling is adequate for the board, adjust as
necessary.
NOTE
If adjustment is required, this can be carried out at Transport Height.
39. Lower the printhead shutter.
40. Press the System button.
41. Select Exit (F8).
42. Select Exit (F8).
Unload
Vision
Height
Home
Height
Board
Clamps
Change
Screen
Open
Cover
Exit
Contact
Height
Transpr t
Height
Change
Screen
Open
Cover
Exit
Contact Height Warning
WARNING Check for obstructions between
the Rails and the Screen
Continue
Open
Cover
Exit
Continue
Open
Cover
Exit
Vision
Height
Open
Cover
Exit
Exit
Vision
Height
Open
Cover
Exit