Printer 600 Board Support Tooling Module.pdf - 第12页
19.12 Technical Reference Manual Chapter Issue 2 May 03 %2$5'6 833257722/,1* 02'8/( )250)/(;7 22/,1* Pneumatic Schematic Mains Air Connection 5 bar (min) To Pneumatic Manifold Filter Regulator Assembly Pres…
%2$5'6833257722/,1*02'8/(
)250)/(;722/,1*
Chapter Issue 2 May 03 Technical Reference Manual 19.11
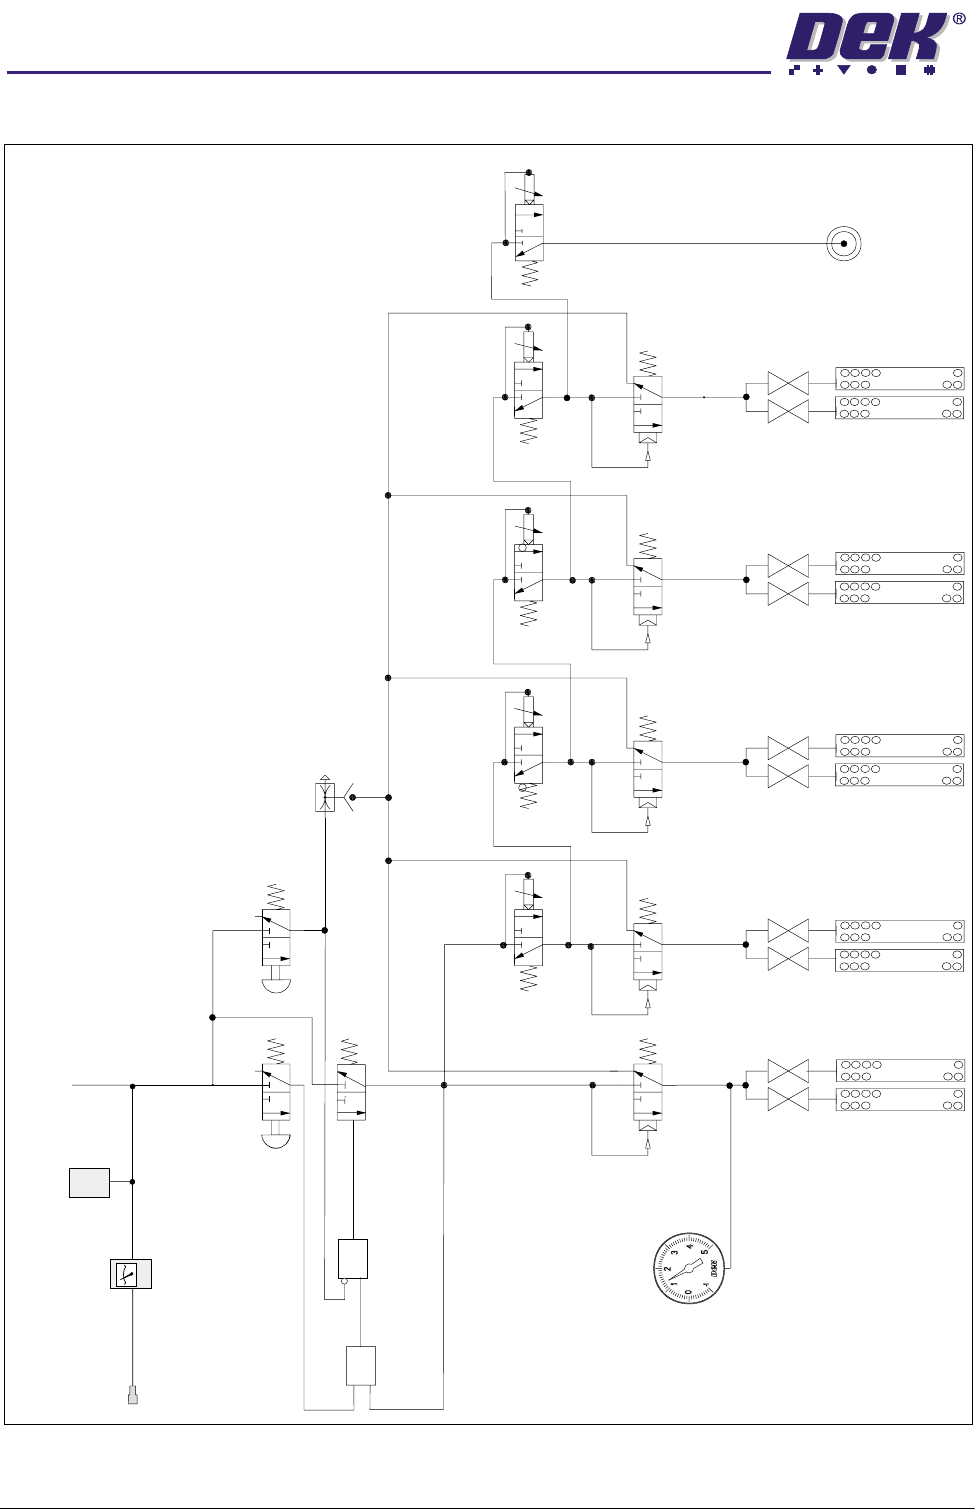
The timers are connected in series and four of these can each control a pair of
tooling modules. Each of the four timers introduce a 20 second cumulative
delay in raising the FormFlex pins. The first pair of tooling modules are
connected directly to the operator switch consequently, the FormFlex pins in
these modules begin to rise as soon as the switch is operated.
The fifth timer is the final timer to operate and controls the pneumatic indicator,
displaying to the operator that all the FormFlex pins have risen.
Once the FormFlex pins have conformed to the new product profile, the
FormFlex setup plate is removed. The remainder of the machine setup is
completed and the machine is set to Run. The FormFlex pins remain in this
configuration until a product changeover is required.
If due to any board or component variation a FormFlex pin is displaced, any
displacement is spread across the other 43 FormFlex pins in that module.
To reset the FormFlex pins for another product, the internal reset switch is
operated. Air pressure is applied to the vacuum ejector to produce vacuum
which is applied to the tooling module.
Pressure is removed from the butyl rubber tube and vacuum is applied, return-
ing the tube to its original profile. Fluid returns to the butyl rubber tube releasing
pressure on the cut-off valve stem allowing the stem to return under spring
force. The valve stem releases the fluid supporting the FormFlex pins enabling
the pins to lower.
19.12 Technical Reference Manual Chapter Issue 2 May 03
%2$5'6833257722/,1*02'8/(
)250)/(;722/,1*
Pneumatic Schematic
Mains Air
Connection
5 bar (min)
To
Pneumatic
Manifold
Filter
Regulator
Assembly
Pressure
Sensor
Ball Valves
Tooling Modules
P
A
R
P
A
R
P
A
R
P
A
R
2
1
3
2
1
3
2
1
3
1
2
3
4
5
6
7
8
9
10
Pneumatic Indicator
Air Pilot
Operated Valves
2
1
3
tttt
P
A
R
Pneumatic Timers
Zn
Zn
Zn
Zn
Zn
2
1
3
t
OR
NOT
Vacuum Ejector
Operator Switch
(Non-Latching Manual Valve)
Reset Switch
(Non-Latching Manual Valve)
13
2
2
2
2
3
3
3
3
1
1
1
1
2
3
1
Yes Gate
Pressure/Vacuum Gauge
%2$5'6833257722/,1*02'8/(
)250)/(;722/,1*
Chapter Issue 2 May 03 Technical Reference Manual 19.13
Air Supply
WARNING
COMPRESSED AIR. COMPRESSED AIR SHOULD NEVER IMPINGE UPON THE
BODY. PORTS, PIPES, ETC MUST NEVER BE BLOCKED BY HAND. BEFORE
CONNECTING ANY PNEUMATIC EQUIPMENT TO A COMPRESSED AIR SUPPLY,
ALL MOUNTINGS, FITTINGS, PIPEWORK AND ELECTRICAL CONNECTIONS
SHOULD BE REMOVED FOR SAFETY. NO PIPEWORK ALTERATIONS OR
REMOVAL OF FITTINGS SHOULD BE ATTEMPTED WITH AIR SUPPLIES
CONNECTED.
Air Pressure For the FormFlex tooling to operate correctly the system requires air at the
following pressure:
• Minimum pressure - 5.0 bar
• Maximum pressure - 8.0 bar
Air Quality The air should be to quality class 2.3.3, where:
2 (dirt) = 1 micron
3 (water) = -20°C pressure dewpoint
3 (oil) = 1mg/m³
Tooling Module
WARNING
HARMFUL SUBSTANCES. CLEANING WIPES AND CLEANING SOLUTIONS MAY
CONTAIN SUBSTANCES HAZARDOUS TO HEALTH. OBSERVE ALL
MANUFACTURERS’ HEALTH AND SAFETY GUIDELINES. ALWAYS WEAR
APPROVED PROTECTIVE CLOTHING WHEN CLEANING THE MACHINE.
The FormFlex tooling system consists of 6 tooling modules, additional tooling
modules are available up to a maximum of 10 modules. Overall dimensions of
each module is 544mm x 25mm with a unit height of 66mm. The module is
connected to the manifold assembly mounted on the manual tooling plate. The
front module has dowel registration fitted and all the modules are held magnet-
ically to the manual tooling plate.
Pin Array Assembly The pin array assembly houses the 44 x 6mm diameter FormFlex pins at a
staggered pitch of 20mm and the fluid cut-off valve. The pin array assembly is
connected to the sequencer and peripherals assembly via the manifold assem-
bly. Each FormFlex pin is fitted with a replaceable graphite impregnated
polyurethane cap enabling Formflex to fully support brittle components and to
facilitate the electrostatic discharge properties of the unit.
Fluid Cut-off Valve The fluid cut-off valve controls the fluid flow to the FormFlex tooling pins. Once
the pins have conformed to the board, component or stencil the valve seals the
fluid supply to the channel beneath the FormFlex pins locking the pins in
position.
Cut-Off Valve
Override Pin
The cut-off valve override pin is used to release sticky cut-off valve stems either
causing the FormFlex pins to remain fully raised or fully lowered. One pin is
supplied with each FormFlex tooling set, (for further details see Fault Finding
later in this chapter).