Printer 600 Board Support Tooling Module.pdf - 第25页
%2$5'68 33257722/,1* 02'8/( )250)/(; 722/,1* Chapter Issue 2 May 03 Technical Reference Manual 19.25 NOTE If only five to oling modules ar e utilized, do not use manifold connections 1 or 2 . 14. Sec ure th…
19.24 Technical Reference Manual Chapter Issue 2 May 03
%2$5'6833257722/,1*02'8/(
)250)/(;722/,1*
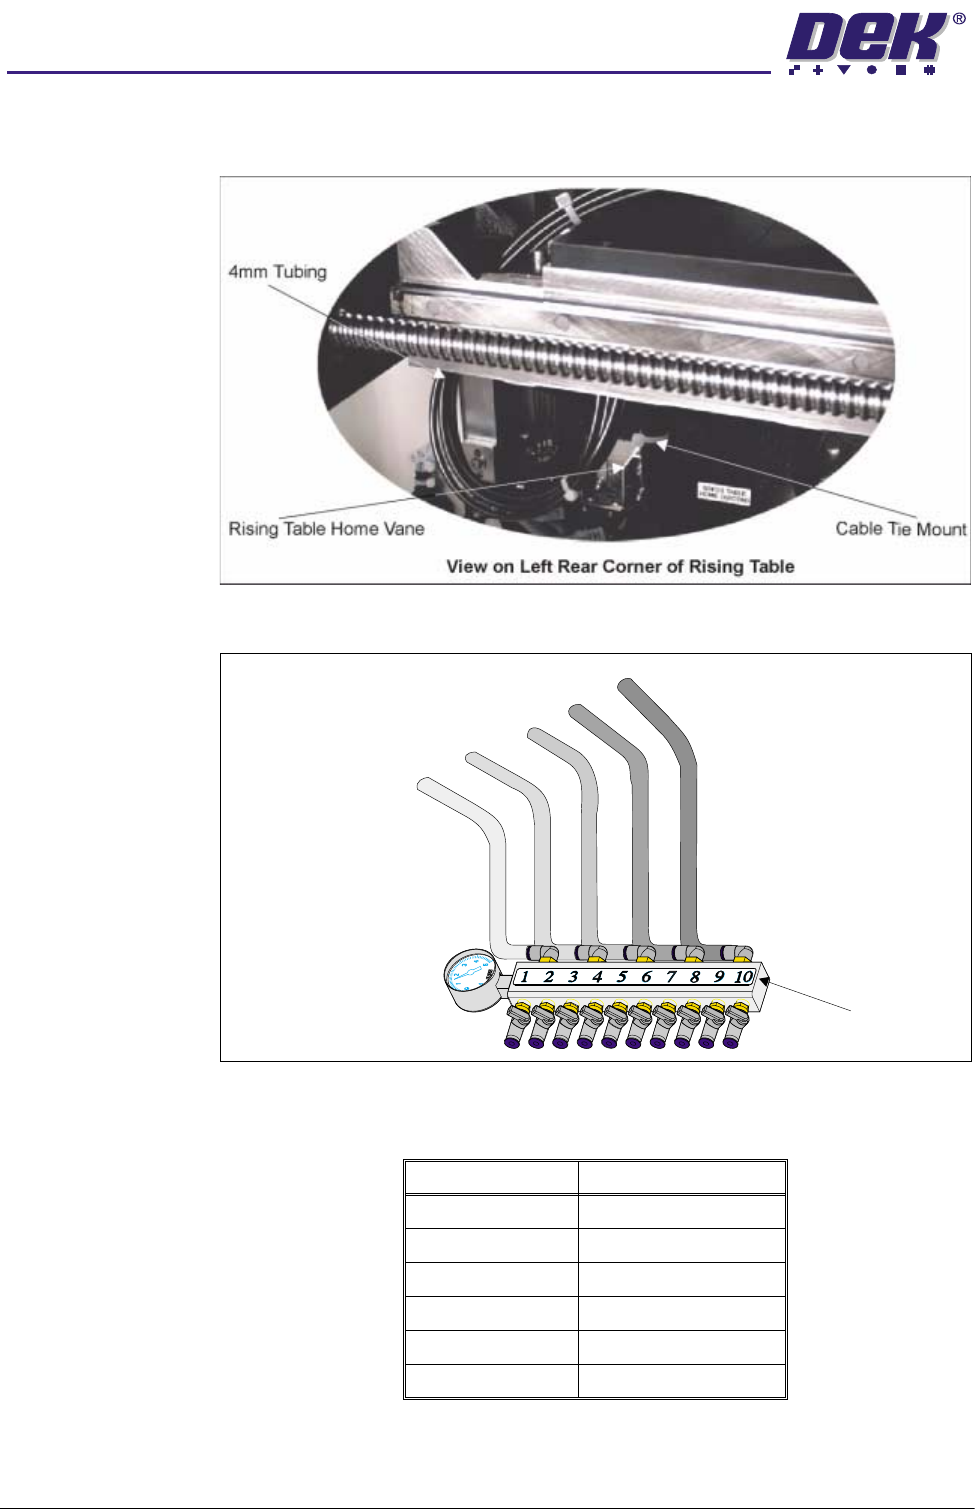
11. Secure the pipes with a cable tie attached to the mount above the rising table
home vane.
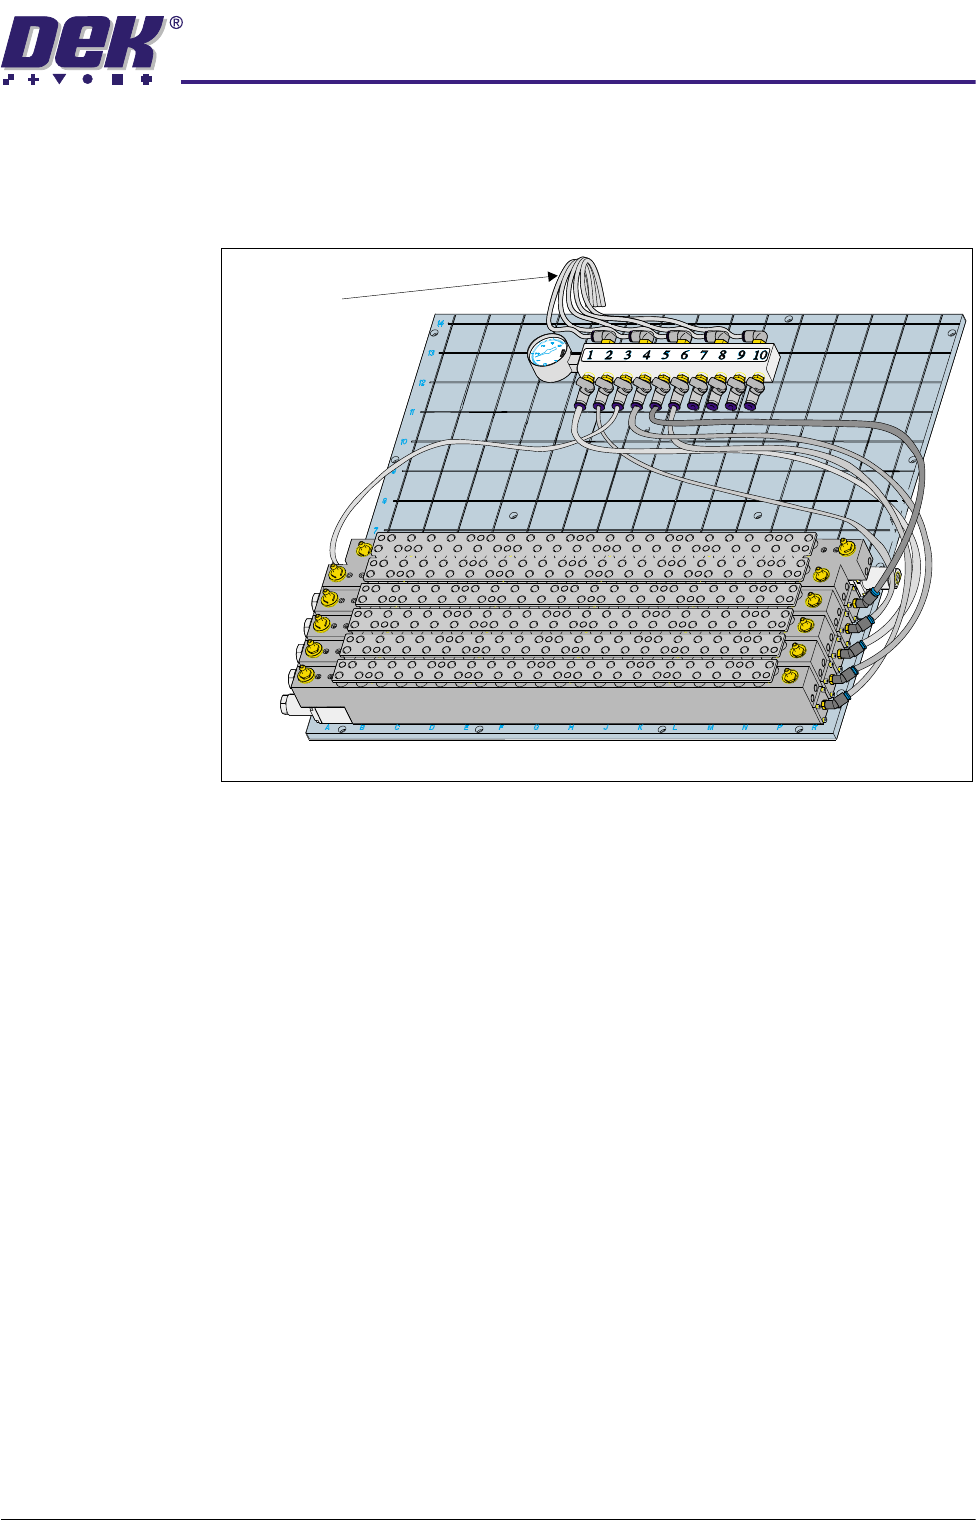
12.Connect the pipes to the manifold assembly (see diagram below).
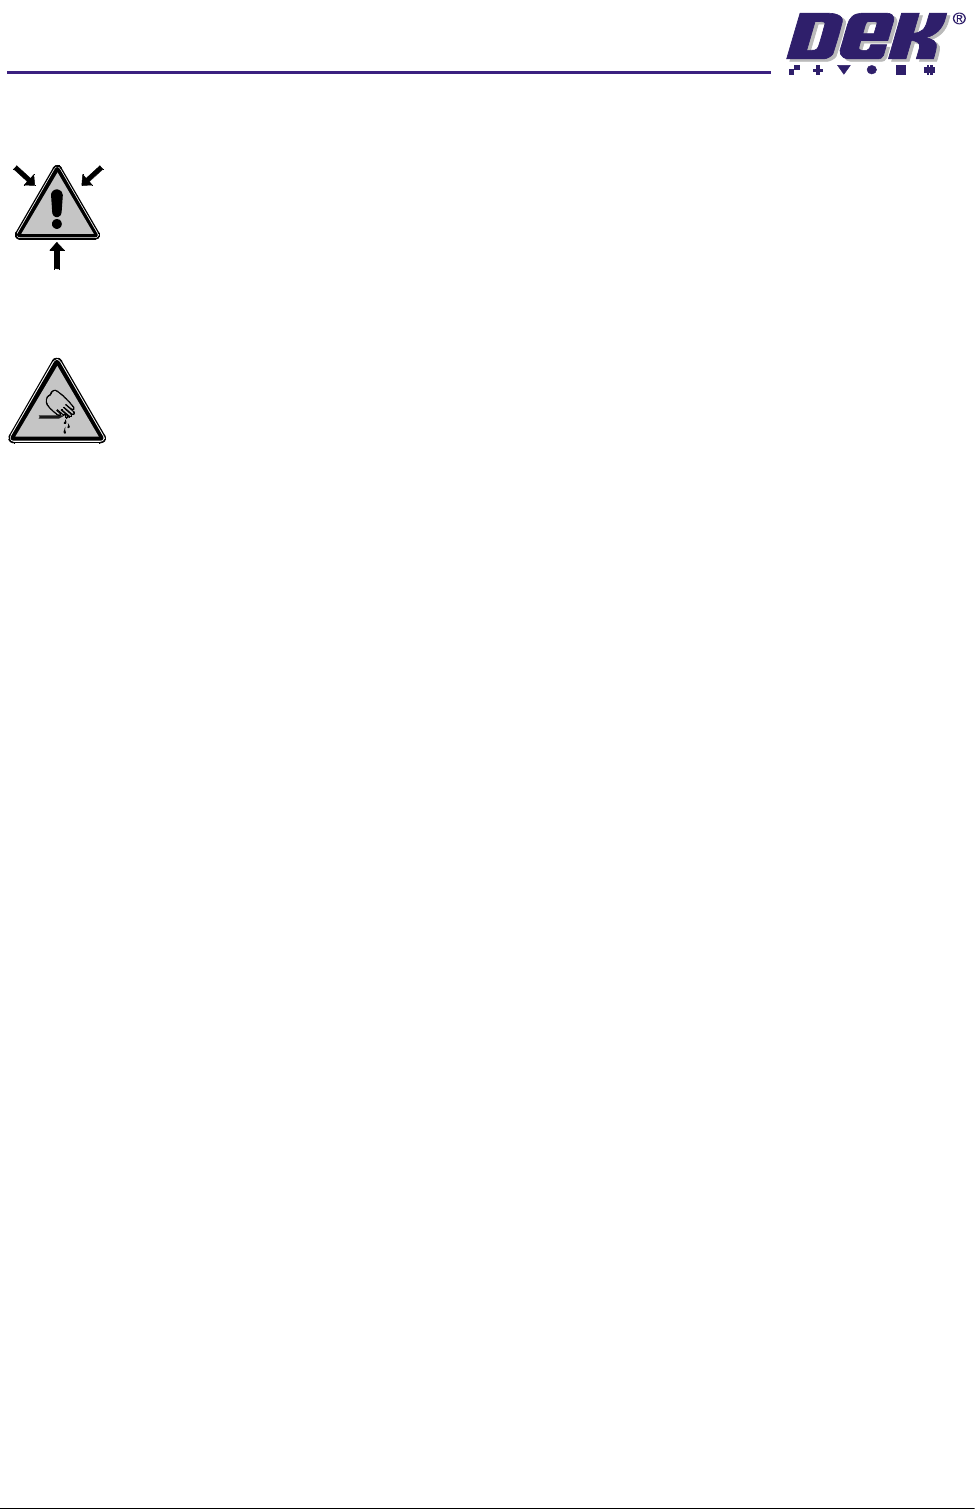
13.Connect 4mm diameter tubing from the manifold assembly to the tooling
modules (see table and diagram below).
Module Number Manifold Connection
19/10
25/6
31
42
57/8
63/4
Pipe 1 From Sequencer
Pipe 2 From Sequencer
Pipe 3 From Sequencer
Pipe 4 From Sequencer
Pipe 5 From Sequencer
Manifold Assembly
%2$5'6833257722/,1*02'8/(
)250)/(;722/,1*
Chapter Issue 2 May 03 Technical Reference Manual 19.25
NOTE
If only five tooling modules are utilized, do not use manifold connections 1
or 2.
14.Secure the tubing with a cable tie attached to a magnetic cable tie mount.
Ensure the tubing does not foul the moving rail.
15.Power up the machine and select Board Width.
16.Carry out FormFlex Pin Pressure procedure in Adjustments and Settings
section of this chapter.
17.Carry out FormFlex Setup in the Machine Programming chapter of the User
manual.
Plan View on Manual Tooling Plate
4mm Tubing From
Pneumatic
Control/Sequencer Panel
19.26 Technical Reference Manual Chapter Issue 2 May 03
%2$5'6833257722/,1*02'8/(
)250)/(;722/,1*
Removing FormFlex Tooling
WARNING
COMPRESSED AIR. COMPRESSED AIR SHOULD NEVER IMPINGE UPON THE
BODY. PORTS, PIPES, ETC MUST NEVER BE BLOCKED BY HAND. BEFORE
CONNECTING ANY PNEUMATIC EQUIPMENT TO A COMPRESSED AIR SUPPLY,
ALL MOUNTINGS, FITTINGS, PIPEWORK AND ELECTRICAL CONNECTIONS
SHOULD BE REMOVED FOR SAFETY. NO PIPEWORK ALTERATIONS OR
REMOVAL OF FITTINGS SHOULD BE ATTEMPTED WITH AIR SUPPLIES
CONNECTED.
WARNING
BOARD CLAMPS. EXTREME CARE MUST BE EXERCISED WHEN WORKING IN
THE TOOLING AREA OF THE MACHINE TO AVOID INJURY. THE FOILS ON THE
FRONT AND REAR BOARD CLAMPS ARE VERY SHARP.
1. From the Run menu select Setup.
2. Select Change Tooling.
3. Select Full Width.
4. Power down the machine.
5. Disconnect and remove the 4mm tubing from between the manifold assem-
bly and the tooling modules.
6. Disconnect the 4mm pipes to the manifold assembly.
7. Remove the manifold assembly and tooling assemblies from the manual
tooling plate.
8. Gain access to the rear of the machine.
9. Remove the cable tie from above the rising table home vane and release
the 4mm tubing from the left hand hole in the rising table casting.
10.Coil the 4mm tubing on top of the sequencer and peripherals assembly,
ensuring the tubing does not foul any moving part of the machine.