ITT-Cannon-RF50-Catalog.pdf - 第46页
Cannon 50 Ohm Connectors ASSEMBL Y INSTRUCTIONS A A I I - - 2 2 2 2 7 7 S S M M A A S S t t r r a a i i g g h h t t C C o o n n n n e e c c t t o o r r s s , , C C r r i i m m p p T T y y p p e e f f o o r r B B r r a a …
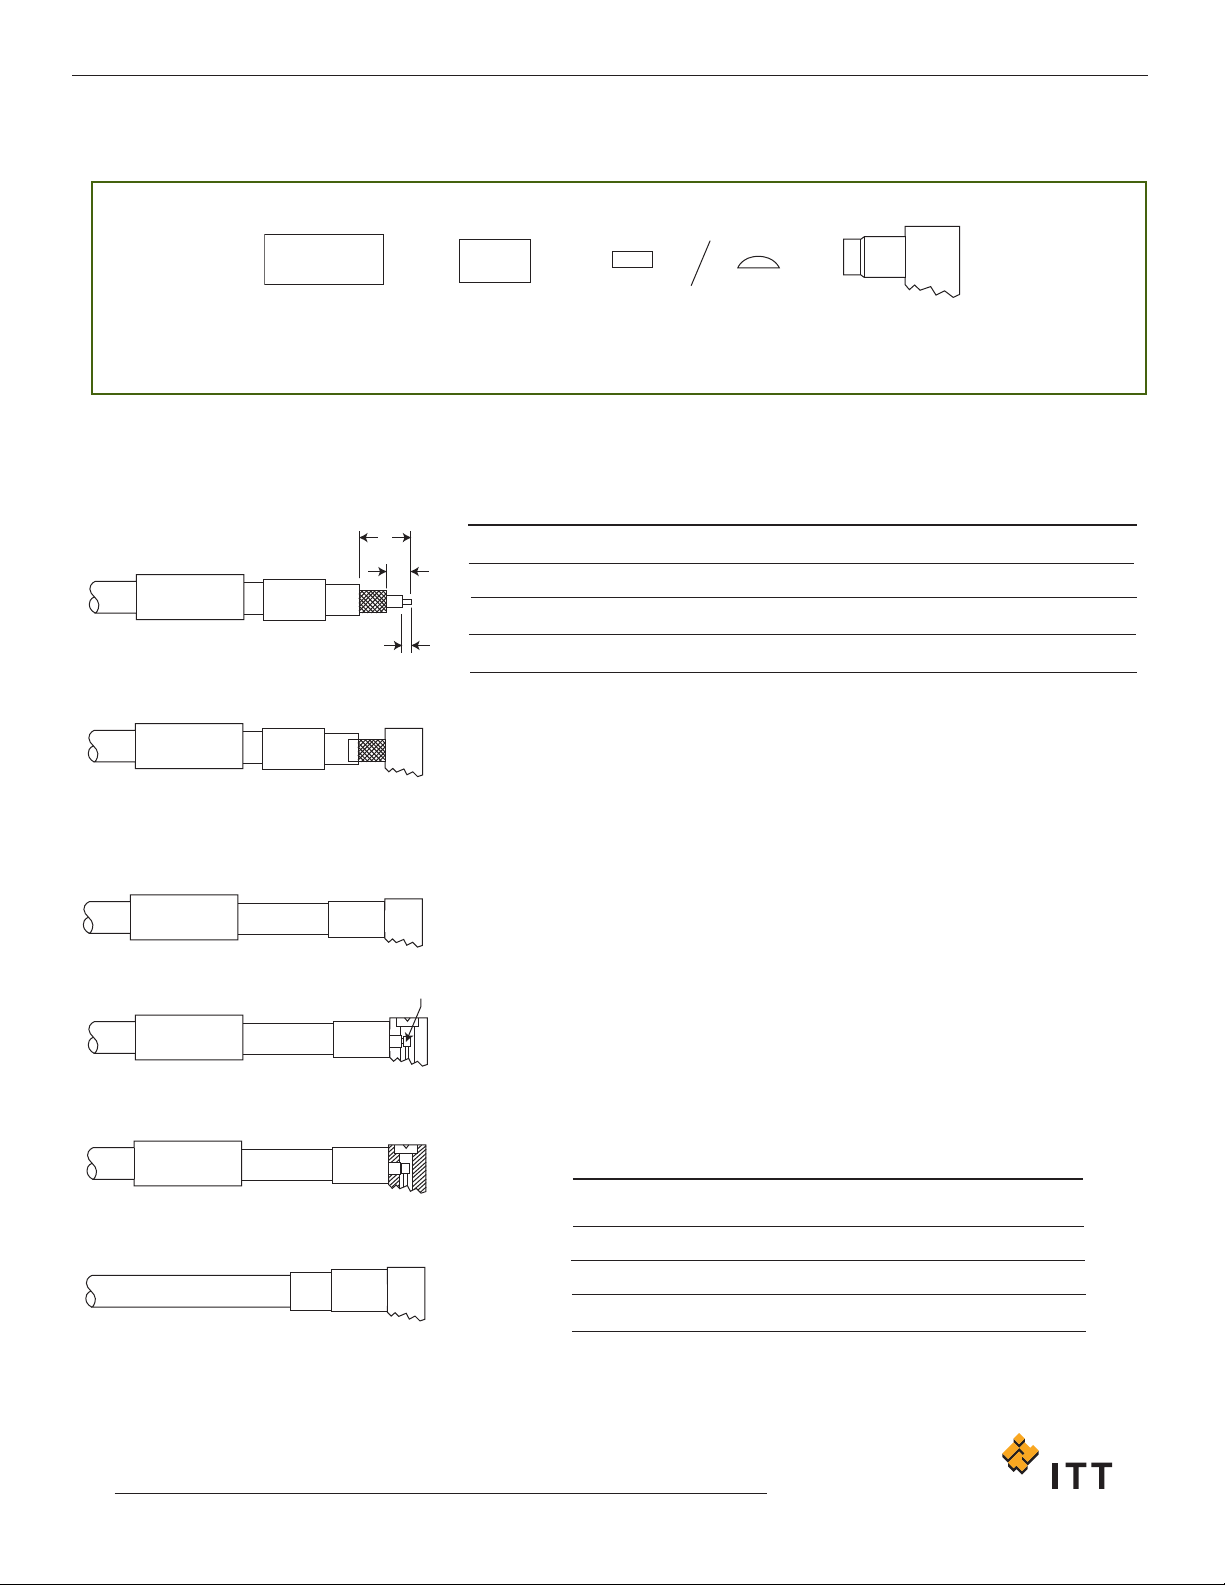
AAII--112299,, AAII--228866 && AAII--669966 SSSSMMBB // SSSSMMCC RRiigghhtt AAnnggllee CCoonnnneeccttoorrss,,
CCrriimmpp TTyyppee ffoorr BBrraaiiddeedd CCaabbllee
HEAT
SHRINKABLE
T
UBING
CRIMP
FERRULE
INSERT OR CAP
REAR BODY
A
B
C
SOLDER
1. Slide heat shrinkable tubing and ferrule on to cable.
2. Trim cable to dimensions shown:
3. Tin center conductor. (DO NOT OVER TIN).
4. Slide body over cable dielectric and under the braid until braid is flush
against underside of rear body
. Ensure center conductor is located in the
forked end of the contact. NOTE: When using cables with inflexible jackets it
is permissible to make two 3,00 (.118) longitudinal slits in the outer jacket.
5. Slide ferrule flush against the body and crimp in position using Cannon’s
Crimp Tool and suitable Die Set (see table).
6. Using a small soldering iron solder center conduct to contact. NOTE: The
center conductor should not protrude beyond the contact or touch the body.
Solder should not protrude beyond the slotted section of the contact.
7.
Press insert into place or locate the cap in rear of body and dimple or lightly
punch to ensure it is locked into position (recommended tool, flat pin ø 3,07
+/- 0,05) (.121 +/- .002).
8. Slide heat shrinkable tubing over ferrule flush against body and heat until
tubing shrinks down.
Only common cable retention features are shown in detail. V
arious body
configurations can apply.
Assembly Instruction No.
AI-129
AI-286
AI-696
A
5,56 (.219)
6,35 (.250)
6,22 (.245)
B
2,77 (.109)
2,77 (.109)
2,54 (.100)
C
1,19 (.047)
0,79 (.031)
1,14 (.045)
Cable Numbers
RG196/U
RG316/U
RD316
Cable Code
3196
3188
3875
Die Size
2,67 (.105)
3,25 (.128)
3,84 (.151)
Die Set
T1025/1
T1025/4
T1025/9
Cannon 50 Ohm Connectors ASSEMBLY INSTRUCTIONS
45
www.ittcannon.com
Dimensions shown in mm (inch)
Specifications and dimensions subject to change
STEP
1-2
STEP 4
STEP 5
STEP
8
STEP 7
STEP 6
Cannon 50 Ohm Connectors ASSEMBLY INSTRUCTIONS
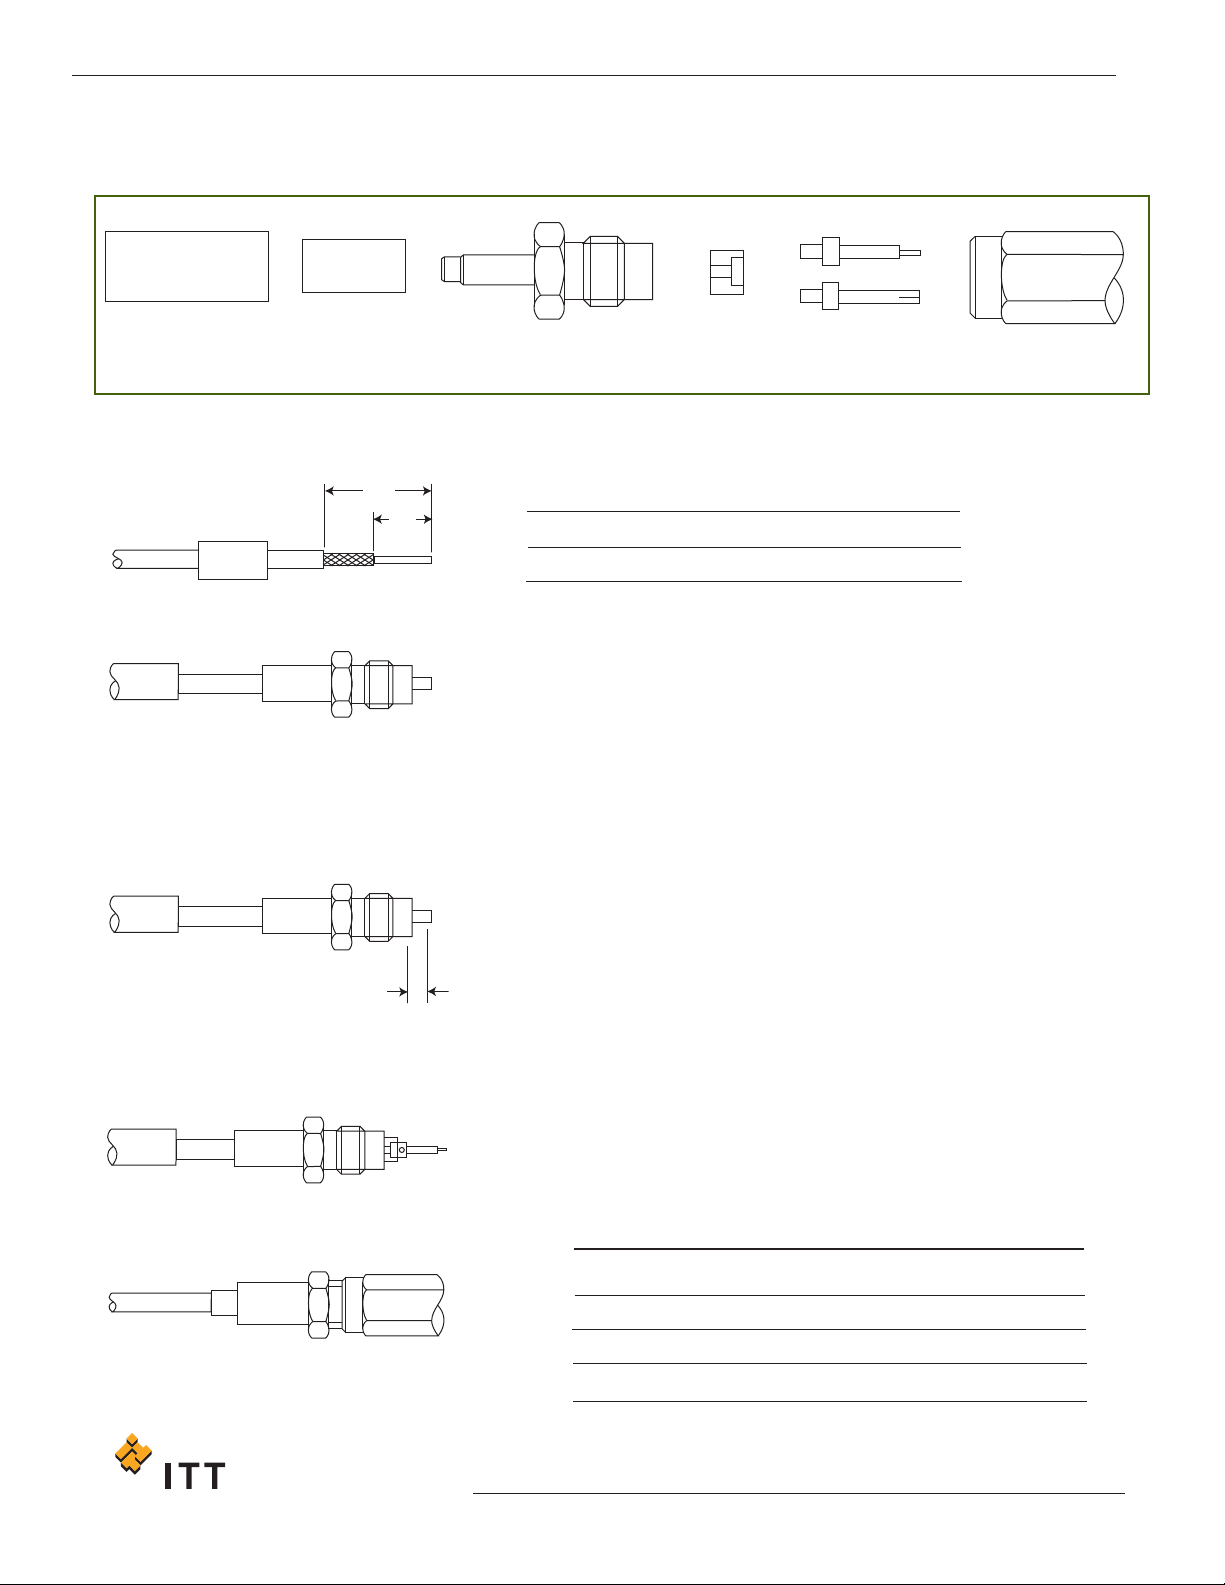
AAII--222277 SSMMAA SSttrraaiigghhtt CCoonnnneeccttoorrss,, CCrriimmpp TTyyppee ffoorr BBrraaiiddeedd CCaabbllee,,
CCaappttiivvee CCoonnttaacctt
HEAT SHRINKABLE
TUBING
CRIMP FERRULE REAR BODY INSULATOR CONTACT FRONT BODY
`
C
B
A
1. Slide ferrule and heat shrinkable tubing on to cable.
2. Trim cable to dimensions shown:
3. Slide body over cable dielectric and under the braid until the braid is flush
against the rear of the hexagonal nut. NOTE: When using cables with
inflexible jackets, it is permissible to make two 3,17 (.125) longitudinal slits
in the outer jacket.
4. Slide ferrule flush against the body and crimp in position using Cannon’s
Crimp Tool and suitable Die Set (see table).
5. Trim back dielectric and center conductor to dimensions shown.
6.
Tin center conductor (DO NOT OVER TIN).
7. Assemble insulator over center conductor with counterbore in direction shown.
8.
Place a small solder preform made from 0,26 - 0,31 (.010 - .012) dia.(28 swg)
multi-core solder in rear of contact.
9.
Assemble contact on center conductor
, heat to make solder connection
ensuring shoulder of contact is flush against rear insulator. Do not allow solder
to protrude outside spill hole.
10. Insert crimped assembly into back end of body and tighten to a torque of 0.70
- 0.80 Nm (100-110 in. ozs.).
11. Slide heat shrinkable tubing over ferrule and apply heat until tubing shrinks
down.
Cable Numbers
RG142/U
RG316/U
RD316
Cable Code
3196
3188
3875
Die Size
2,67 (.105)
3,25 (.128)
3,84 (.151)
A
15,00 (.590)
B
9,00 (.354)
C
3,00 (.118)
Die Set
K29263
K29263
T1025/9
46
www
.ittcannon.com
Dimensions shown in mm (inch)
Specifications and dimensions subject to change
STEP 1-2
STEP 3
STEP 5
STEP 9
STEP 10
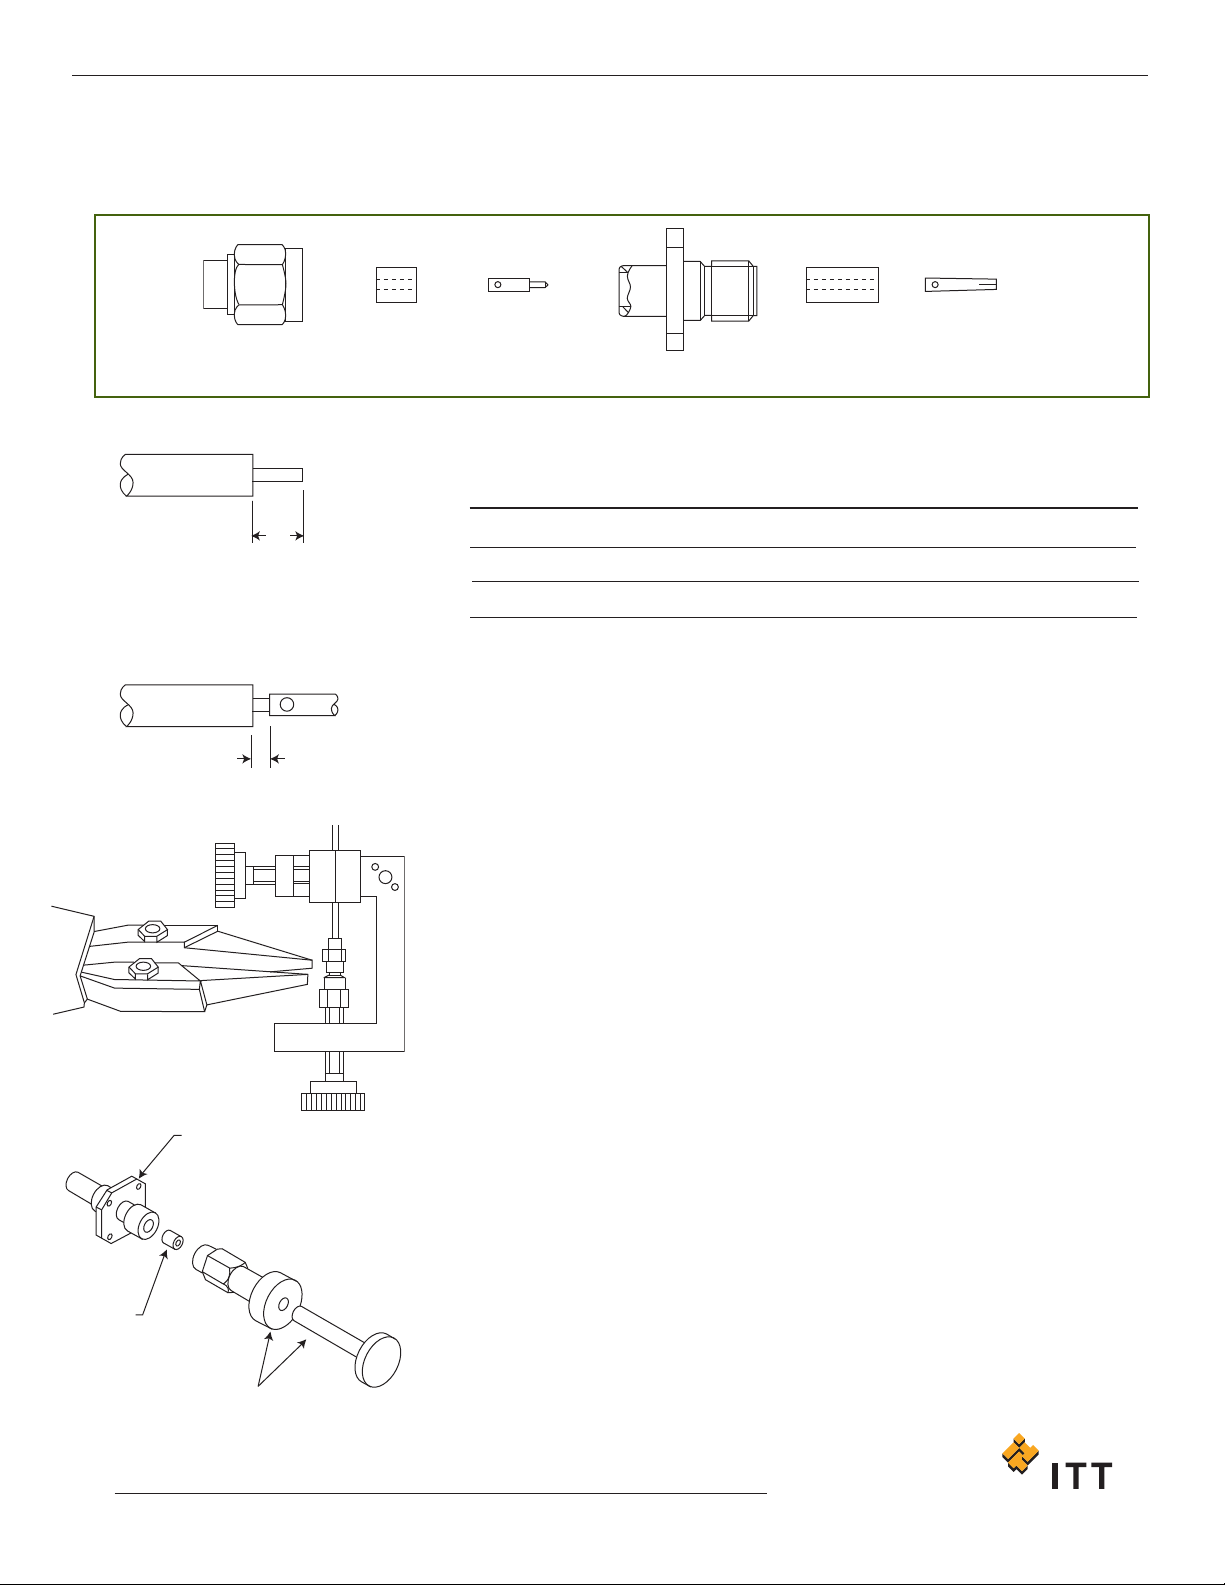
AAII--225522 && AAII--227788 SSMMAA SSttrraaiigghhtt CCoonnnneeccttoorrss,, DDiirreecctt SSoollddeerr
((SSeeppaarraattee CCeenntteerr CCoonnttaacctt)) TTyyppee ffoorr SSeemmii--RRiiggiidd CCaabbllee
PLUG BODY INSULATOR CONTACT JACK BODY INSULATOR CONTACT
A
B
CONNECTOR
INSULATOR
DIELECTRIC
INSERTING TOOL
1. Cut cable end square. Trim the cable outer conductor and dielectric as
shown taking care not to nick the center conductor. Deburr outer conductor at
point of cut.
2. Tin center conductor (DO NOT OVER TIN).
3. Solder contact to center conductor ensuring that dimension shown is
maintained. Remove any excess solder.
4. Clean housing area of outer conductor with abrasive paper and clean in a
suitable agent.
5. Place connector assembly in Assembly Jig T1848, or other suitable clamping
arrangement, with contact in locator tool as shown.
Tighten screw to secure cable between inserts then tighten locator to seat cable
firmly. Place solder ring around cable adjacent to connector body and heat the
connector body using an appropriate heat source (solder tongs with variable
control). Apply sufficient heat for solder to flow but using minimum heat cycle.
6. Using dielectric insertion Tool T2508 (for plugs) or T2509 (for jacks), press
insulator into body
. Assembly is now ready for use.
N.B. Various body configurations can apply.
Assembly Instruction No.
AI-252
AI-278
Configuration
Plug
Jack
A
3,18 +/- 0,25 (.125 +/- .010)
2,54 +/- 0,25 (.100 +/- .010)
B
0,38 (.015)
0,38 (.015)
Cannon 50 Ohm Connectors ASSEMBLY INSTRUCTIONS
47
www.ittcannon.com
Dimensions shown in mm (inch)
Specifications and dimensions subject to change
STEP 1 - 2
STEP 3
STEP 5
STEP 6