03238396-01-01 High Flow Vacuum (TQ).pdf - 第18页
5 TECHNICAL REFERENCE 5.1 SYSTEM OVERVIEW 18 STANDALONE MANUAL HIGH FLOW VACUUM (TQ) 12/2020 5.1.1.4 Pump Assembly The assembly consists of the following: ● Pump ● Vac Pump Enable Controller (VPEC) ● Mounting Plate and B…
5 TECHNICAL REFERENCE
5.1 SYSTEM OVERVIEW
STANDALONE MANUAL HIGH FLOW VACUUM (TQ) 12/2020 17
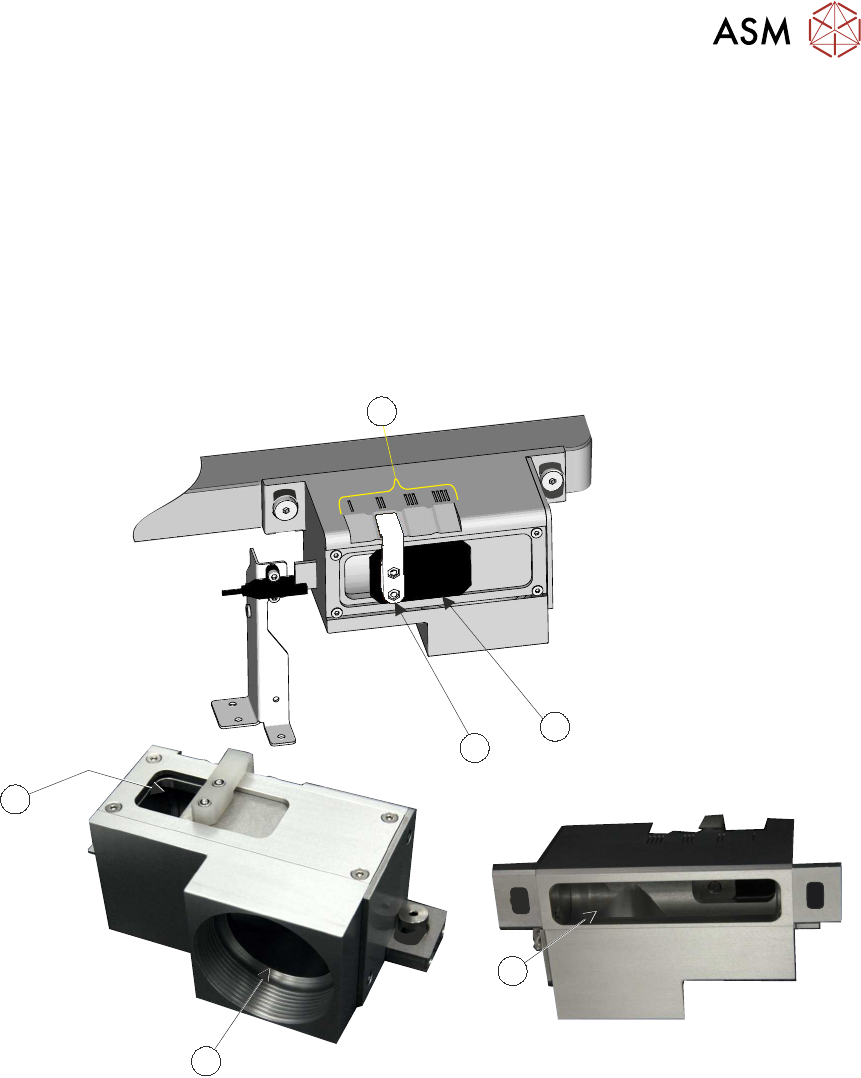
5.1.1.3 Flow Controller
The support tooling is assembled into a box arrangement that creates a vacuum chamber to hold
the product during printing. The flow of air in the support tooling is fed through channels under the
tooling plate to the vacuum inlet port (3). The flow controller is a manually set device that controls
the evacuated air flow back to the pump via outlet (4).
By opening the control aperture (5), the vacuum flow in the support tooling decreases; closing the
aperture increases the flow. The sliding baffle plate (1) has a positive action when moved, the
handle (2) latches into a position as indicated (6).
The product size, through holes and aperture opening, affect the ability to hold the product during
printing and separation. By carrying out trials the user can determine the optimum set up for the
product; this increases the efficiency of the process.
2
6
1
3
5
4
5 TECHNICAL REFERENCE
5.1 SYSTEM OVERVIEW
18 STANDALONE MANUAL HIGH FLOW VACUUM (TQ) 12/2020
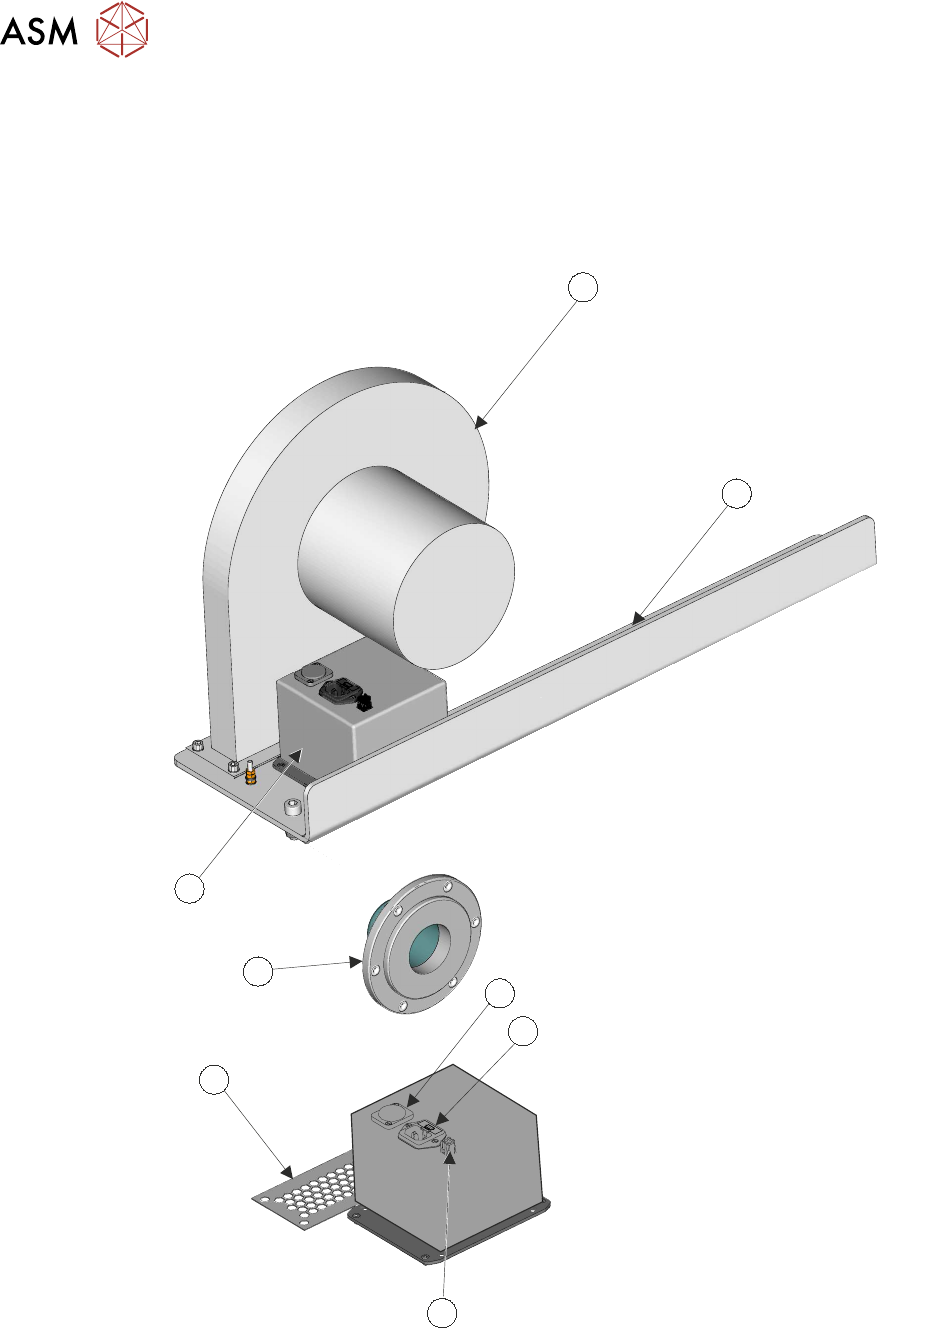
5.1.1.4 Pump Assembly
The assembly consists of the following:
●
Pump
●
Vac Pump Enable Controller (VPEC)
●
Mounting Plate and Beam
1
2
3
4
6
7
8
5
Refer to the electrical schematic.
Power to the pump (1) comes from the M71 power supply to the 5A fused input plug (4).
In the VPEC unit (8) an enable signal DOUT 7 from ESIO#3 latches CON 1 contactor relay. The
associated control switches close; this provides mains input to the pump via plug (3).
At the base of the pump, its output has a finger guard (6) to prevent access to the moving parts.
5 TECHNICAL REFERENCE
5.1 SYSTEM OVERVIEW
STANDALONE MANUAL HIGH FLOW VACUUM (TQ) 12/2020 19
At the pump’s vacuum input port, a magnetic coupling (7) is used to connect to the diverter valve
air hose.
The pump and VPEC unit are mounted onto the printer’s chassis with a mounting plate beam (2).
5.1.2 Operational Sequence
With High Flow Vacuum fitted and enabled, the print sequence is as follows:
1. Print is selected.
2. High Flow Vacuum is switched ON and remains on.
3. The product is loaded; the carrier/board moves into the print station and stops at the remote
board stop and is clamped.
4. The product is raised to vision height.
5. Camera sweep occurs to collect substrate and stencil fiducials data.
6. Align chase/stencil is performed.
7. The product is raised to print height.
8. The product is printed.
9. Separate the product from the stencil.
10. The product is lowered to vision height.
11. Camera sweep (post print alignment) is performed.
12. Table moves to transport height -unload product at transport height.
13. Carrier/board moves to outroad conveyor.
14. The sequence repeats from step 3 until the batch has printed.
15. High flow vacuum switches OFF.