03238396-01-01 High Flow Vacuum (TQ).pdf - 第42页
6 USER GUIDE 6.1 SETUP PROCEDURES 42 STANDALONE MANUAL HIGH FLOW VACUUM (TQ) 12/2020 6.1.2 Product Changeover NOTE Customer ’ s requiring tooling design or manufacture assistance should contact ASM-DEK on: tooling.uk@asm…
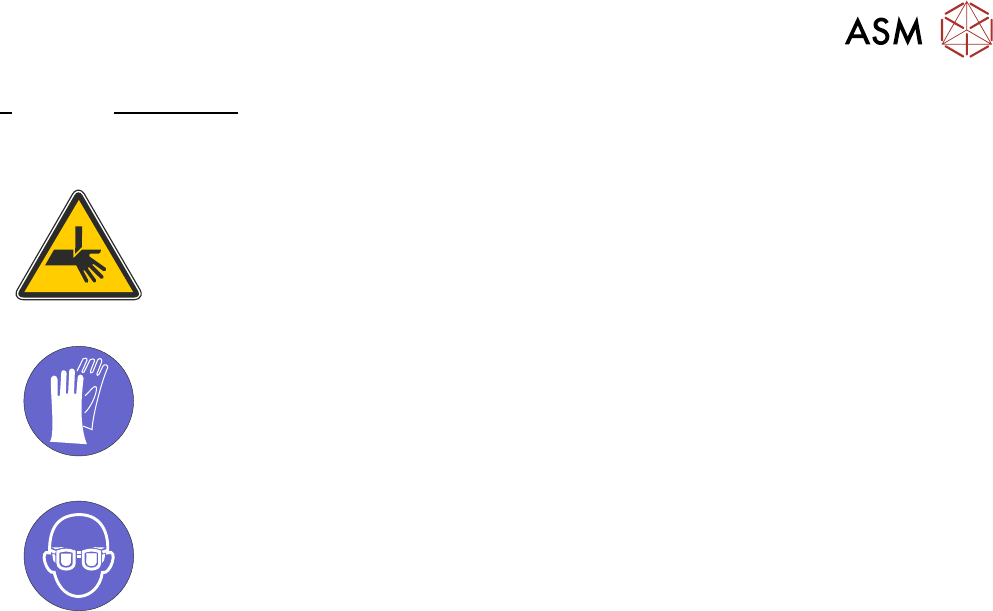
6 USER GUIDE
6.1 SETUP PROCEDURES
STANDALONE MANUAL HIGH FLOW VACUUM (TQ) 12/2020 41
6
USER GUIDE
6.1 SETUP PROCEDURES
WARNING
BOARD CLAMPS. EXTREME CARE MUST BE EXERCISED WHEN WORKING IN
THE TOOLING AREA OF THE MACHINE TO AVOID INJURY. THE FOILS ON THE
FRONT AND REAR BOARD CLAMPS ARE VERY SHARP.
MANDATORY
TOXIC SUBSTANCES MAY BE PRESENT. SAFETY GLOVES MUST BE WORN.
MANDATORY
TOXIC SUBSTANCES MAY BE PRESENT. EYE PROTECTION MUST BE WORN.
NOTE
All parameters in these procedures are example parameters , the correct set up can only be de-
termined by trial with a users' actual product.
6.1.1 Product Set Up
NOTE
Before changing product layout, load a default product file, this prevents data being overwritten in
the production product file.
To create a Default product file:
1. On the HMI select Programming from the system Menu drop-down.
2. Select a product to rename and alter, as necessary.
3. Select Copy.
4. Select Name.
5. Rename the file.
6. Select Accept.
7. Select Save And Exit.
8. Select Exit.
9. On the system Menu drop-down select Manage Printer Setup.
10. Select Check Tooling.
11. Select Under Clearance and check/set it to 14mm.
NOTE
This dimension is the maximum allowable when High Flow Vacuum tooling is fitted due to the
addition of the tooling plate.
12. Select Accept.
13. Select Switch ON High Flow Vacuum.
14. Select Exit.
6 USER GUIDE
6.1 SETUP PROCEDURES
42 STANDALONE MANUAL HIGH FLOW VACUUM (TQ) 12/2020
6.1.2 Product Changeover
NOTE
Customer’s requiring tooling design or manufacture assistance should contact ASM-DEK on:
tooling.uk@asmpt.com
1. On the HMI select Changeover from the system Menu drop-down.
2. Select the new product from the list. If the list is large, use the search function to locate the
product to load.
NOTE
Ensure that the correct product is loaded e.g. a top mounted or bottom mounted board.
3. Select Continue.
4. Select Carriage To Rear.
5. Open the cover and remove any non-reusable items (for the new product: squeegees, mater-
ial, support tooling etc.).
6. Load the new product consumables and place the tooling.
7. Select Continue.
8. Select items from the dropdown menu for each category:
– Support
– Squeegees
– Stencil
– Material
9. Close the cover.
10. Press the System button.
11. Select Manage Printer Setup.
12. Select Check Tooling.
13. Select Switch On High Flow Vacuum.
NOTE
At initialization, the presence of High Flow Vacuum is checked. However, it needs to be set for
each product.
14. Select Under Clearance. With HFV fitted the maximum allowable under clearance is 14mm.
Ensure that the setting is 14mm.
15. Select Exit.
16. Select Manage Printer Setup.
17. Select Check Alignment.
18. Select Load Stencil.
19. Open the cover.
20. Load the stencil.
21. Close the cover.
22. Press the System button.
23. Select Load Board.
24. Place a board to the input conveyor.
25. Select View Alignment.
26. Select Print Gap.
27. Set a print gap between the stencil and the board.
28. Select Accept.
29. Select Print Single Board.
30. Remove the board from the downline conveyor.
31. Select Exit.
32. Select Exit.
6 USER GUIDE
6.1 SETUP PROCEDURES
STANDALONE MANUAL HIGH FLOW VACUUM (TQ) 12/2020 43
33. Select Complete.
34. Select the Adjust tab.
35. Select Board Limit.
36. Set the board limit to 5.
37. Select Accept.
38. In the Information bar, the information posted is: Adjust Parameters Modified. Select Save.
39. Select the Status Tab. Provided the printer is ready to accept and print some test boards
(print medium/product available) the printer is ready for printing.
40. Select Print.
6.1.3 Machine Set Up
There are no user parameters in Machine Setup that relate specifically to High Flow Vacuum set
up. The vacuum can be switched ON or OFF in: Menu/Manage Printer Setup/Check Tooling.