Maintenance (Micron) workbook Iss07.pdf - 第71页
Issue 6, Nov 14 71 Objective BT3: Perform benchmark test and record results Apply small amount of paste or suitable lubr icant to stencil to lubricate squeegees. Run QC-Calc package on printer. Carry out a minimum of 100…
70 Issue 6, Nov 14
Objective BT2: Set up machine for benchmark test
Load the 265test1 product file and ensure that the following parameters are set
correctly:
• Front Print speed 25 mm/s
• Rear Print speed 25 mm/s
• Front Pressure 5kg
• Rear Pressure 5kg
• Separation Speed 1 mm/s
• Under Clearance 20mm
• No paste dispense or Screen Cleaner rate
• SPC Configuration :
¾ Data output rate = Every cycle
¾ Start Rate = 1
¾ Sample Rate = 0
¾ Start Rate Limit = 0
¾ SPC data mode = Disc
¾ SPC Format = Windows
¾ Update On Start = No
¾ Align Inspect mode = Post
Ensure that the following hardware is set-up correctly:
• 9 Tooling support pillars are used
• Squeegees fitted are of the correct length to suit board and heights calibrated
• DEK alignment test board (Part Number 137071) is used
• Screen loaded is the calibration/dry align screen
• Transport mode – No Transfer
Adjust machine parameters for benchmark test
• Transport Mode Left to Left (or Right to Right)
• Upline Protocol No FMI
• Downline Protocol No FMI
• Screen size 265
Issue 6, Nov 14
71
Objective BT3: Perform benchmark test and record results
Apply small amount of paste or suitable lubricant to stencil to lubricate squeegees.
Run QC-Calc package on printer.
Carry out a minimum of 100 full machine cycles.
On completion of the test record the following information:
• X alignment Cp/Cpk =
• Y alignment Cp/Cpk =
• Theta alignment Cp/Cpk =
• Front Pressure Cp/Cpk =
• Rear Pressure Cp/Cpk =
• Front Print Speed Cp/Cpk =
• Rear Print Speed Cp/Cpk =
• Separation Speed Cp/Cpk =
Note: The error message ‘No variation in selected data – Increase significant digits’ may
appear’ for pressure and speeds due to the lack of variation. In this instance, no values are
required.
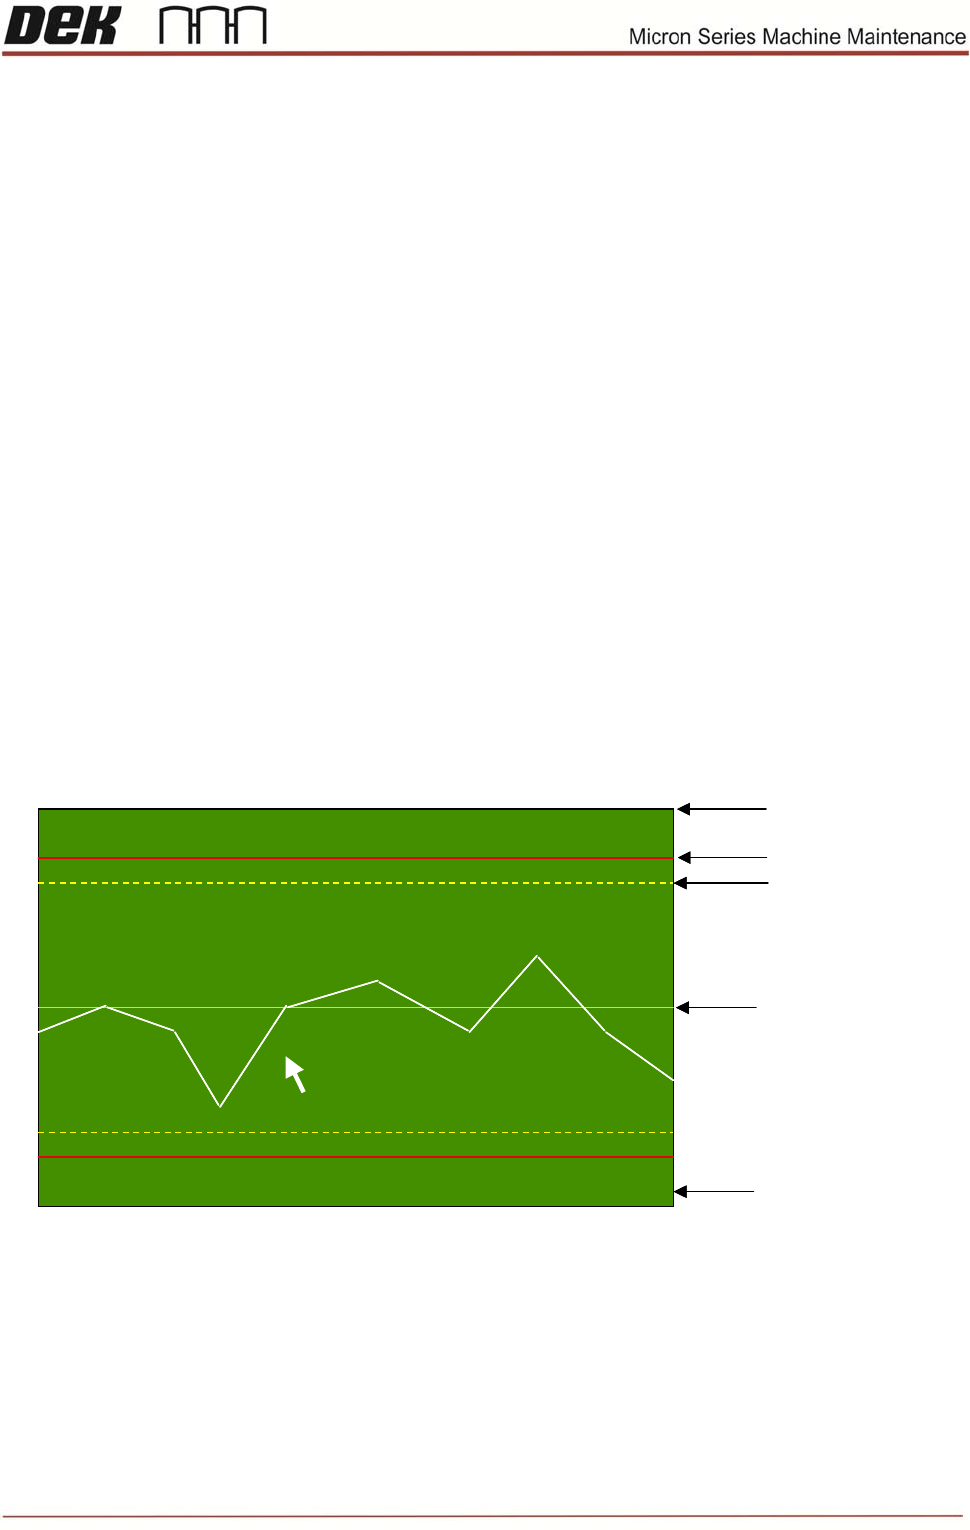
Task: Identify the arrowed items below:
NOTES:
(3) Theta Error (arcsec)
Cp = 1.11
10.0474 143
-17.0000
37.0000
10.0000
(3) Theta Error (arcsec)
Cp = 1.11
10.0474 14310.0474 143
-17.0000
37.0000
10.0000
72 Issue 6, Nov 14
Objective BT4: Identify common causes of poor performance
With the instructor, discuss the typical causes and solutions to any poor results.
NOTES:
Try video model mode
Fiducial capture
Disconnect chase clamps -no pressure
Screen move -Chase clamps
Screen move - Stretch Try new screen
Board move - belts
Remove tooling
Board move- Rail parallelism Reduce board width .5mm
Print carriage bearings
Run dry align
Calibrations
Calibrate
SUMMARY OF ADJUSTMENTS