Infinity Generic Tooling.pdf - 第23页
INFINITY MACHI NE PROG RAMMI NG STAGE 6 D - MULTIFLEX TOOLING User Manual 1.49 NOTE Ensure th at Generic T ooling is set to Enable d in Set Prefs. 6. Select Change T ooling (F6). The print carriage moves to the front of …
INFINITY
MACHINE PROGRAMMING
STAGE 6D - MULTIFLEX TOOLING
1.48 User Manual
STAGE 6D - MULTIFLEX TOOLING
WARNING
BOARD CLAMPS. EXTREME CARE MUST BE EXERCISED WHEN WORKING IN
THE TOOLING AREA OF THE MACHINE TO AVOID INJURY. THE FOILS ON THE
FRONT AND REAR BOARD CLAMPS ARE VERY SHARP.
CAUTION
BOARD CLAMPS.
Care must be taken to ensure that the board clamps are
not damaged when removing or replacing tooling.
NOTE
Setting up the MultiFlex tooling is to be performed off the machine.
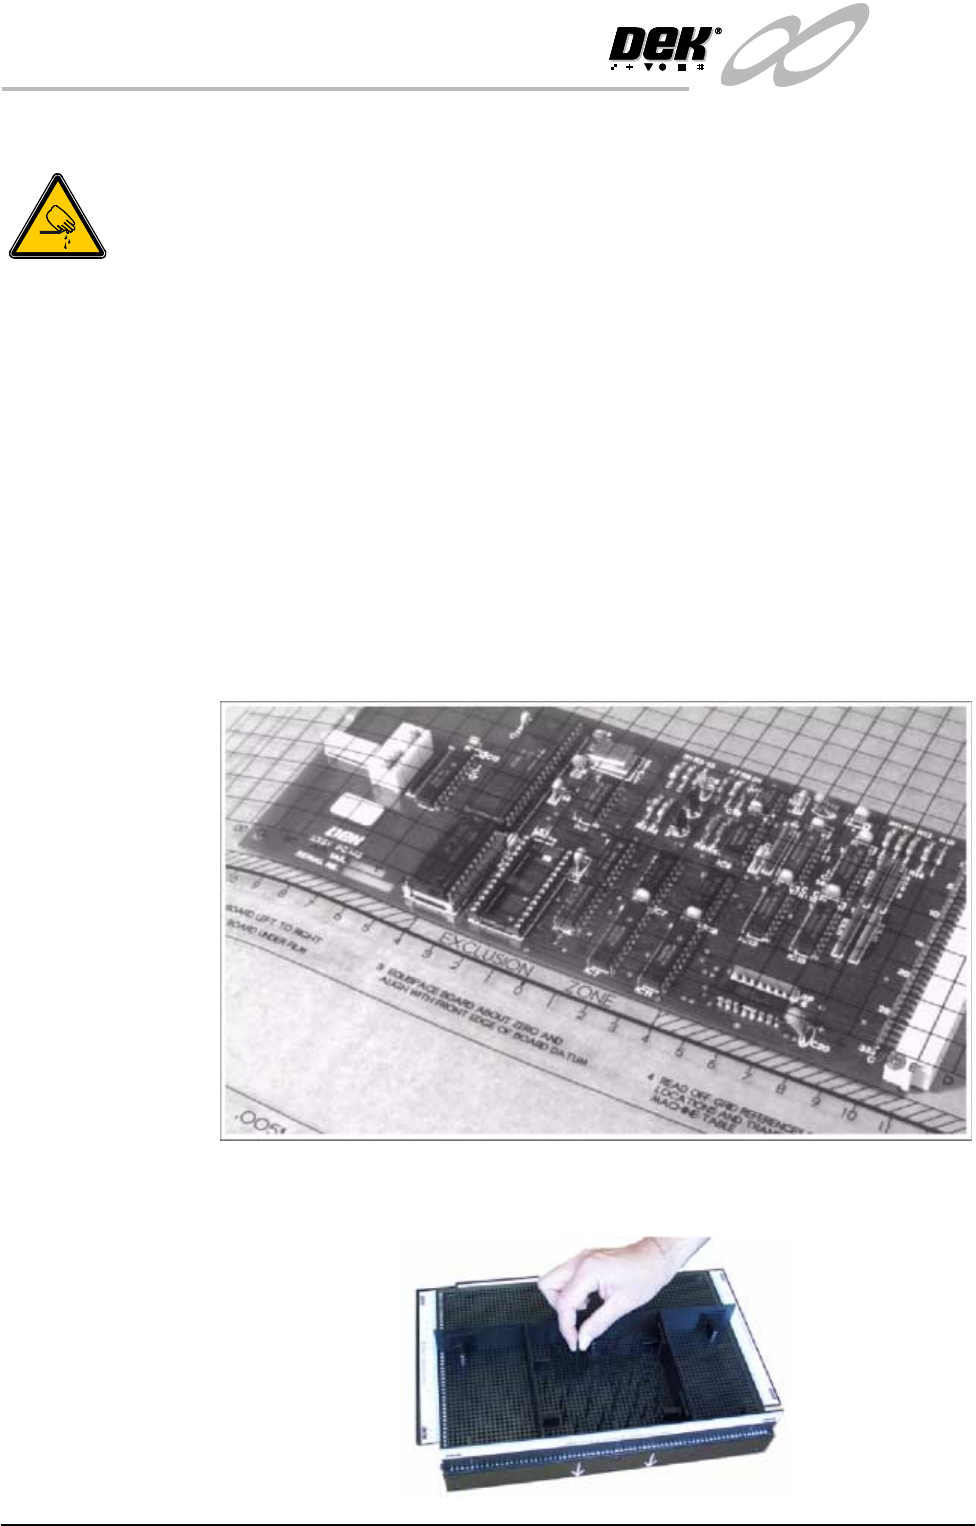
1. Create a box the same size as the board using the side plates.
2. Use the board width and board length dimensions to position the box
correctly.
3. Place the PCB on a flat surface, component side up.
4. Position the acetate template, supplied with the tooling, over the PCB such
that the front edge of the board is aligned with the arrow indicators on the
template. Ensure that the centreline of the board is aligned with the template
zero.
5. Using the grid co-ordinates marked on the template, position pins which
coincide with gaps between the underside board components.
INFINITY
MACHINE PROGRAMMING
STAGE 6D - MULTIFLEX TOOLING
User Manual 1.49
NOTE
Ensure that Generic Tooling is set to Enabled in Set Prefs.
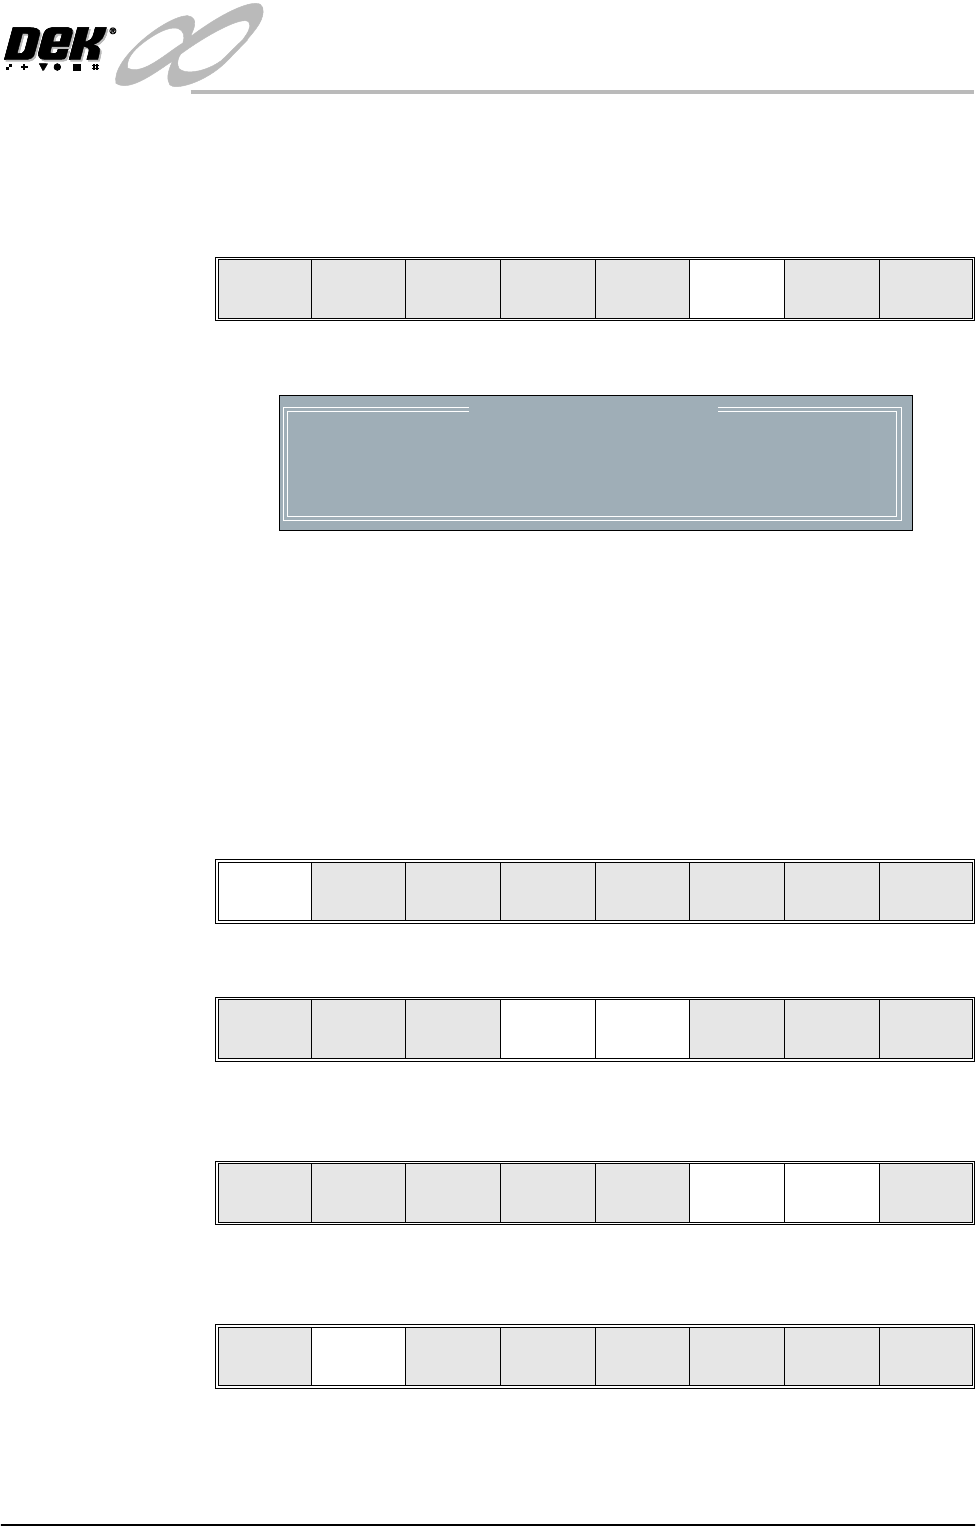
6. Select Change Tooling (F6). The print carriage moves to the front of the
printer.
The Change Tooling Parameters window is displayed:
NOTE
If the remote board stop is fitted the Board Stop X and Board Stop Y
parameters are replaced by Remote Board Stop X.
7. Setting up the board stop position is automatically done using the board
dimensions previously set in the product file. If they need adjustment to re-
position the board stop for any reason, ie any routing on the board edge or
a badly positioned image on the stencil, this can be done now. If adjustment
is necessary continue with Step 8. If adjustment is not necessary go to Step
13.
8. Select Adjust (F1).
9. Use the Next and Previous keys (F4 - F5) to highlight each parameter.
10. Use the Incr. and Decr. keys (F6 - F7), or the forward slash key (/) on the
keyboard, to change the parameter value.
11. Select Save (F2). The message ‘Saving fiducial data - Please wait Board
data file saved’ is displayed.
Mode
Load
Data
Edit
Data
Setup
Squeegee
Change
Screen
Change
Tooling
Change
Language
Exit
Change Tooling Parameters
BOARD WIDTH
BOARD STOP X
BOARD STOP Y
UNDER CLEARANCE
216.0
125.0
142.6
19.0
mm
mm
mm
mm
Adjust
Raise
Head
Remove
Cleaner
Board
Stop
Full
Width
Load
Width
Generic
Toolin g
Exit
Save Next Previous Incr. Decr. Exit
Save Next Previous Incr. Decr. Exit
Save Next Previous Incr. Decr. Exit
INFINITY
MACHINE PROGRAMMING
STAGE 6D - MULTIFLEX TOOLING
1.50 User Manual
12. Select Exit (F8).
13. Select Full Width (F5). The message ‘Checking for a board on the belts’
is displayed. Whilst the rear rail is moving the following message ‘Rail
moving...’ is displayed.
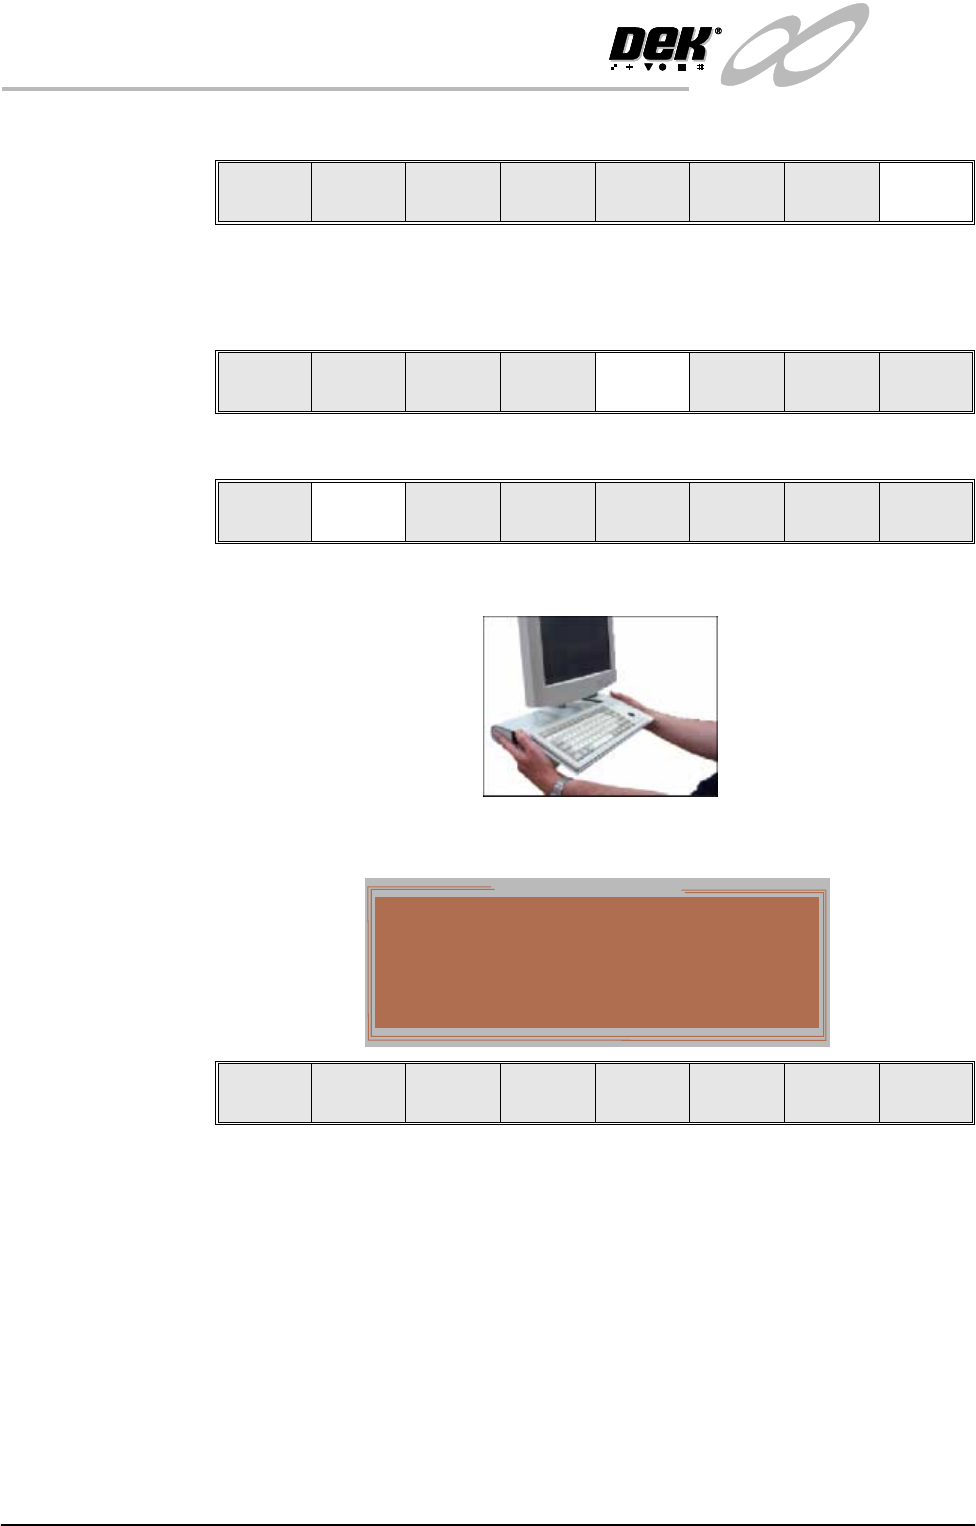
14. Select Raise Head (F2).
15. Raise the printhead using two button control.
The following window and menu bar is displayed:
Save Next Previous Incr. Decr. Exit
Adjust
Raise
Head
Remove
Cleaner
Board
Stop
Full
Width
Load
Width
Generic
Toolin g
Exit
Adjust
Raise
Head
Remove
Cleaner
Board
Stop
Board
Width
Load
Width
Generic
Toolin g
Exit
Hazardous Operation
The head must be propped while it is
raised
Insert the Head Prop.
Confirm
Lower
Head