User-Manual-of-NeoDen4-PNP-machine.pdf - 第39页
34 ⑺ ⑹ ⑸ ⑷ The size o r shap e isn’t aligned with that in “Footprint library” The size o f nozzle is ina ppropriate or insufficie nt suc tion. The nozzle is damage d o r blocked, and even has a c rack 4.7 .8 P&P prog…
33
4.7.7 First trial and testing
(1) First dry run
Usually we would suggest you to have a dry run (no components are loaded) before production test.
After it goes smoothly, you can start to produce few boards.
(2) Production test
a. Make a programming file
b. Test the file to pick and place components.
(3) Inspection
a. Inspection Items
Check if the specification, direction, polarity of components is aligned with what they should be.
Whether the components are damaged or the pins are distorted.
Whether the component is off beyond allowance.
b. Inspection Methods
The inspection methods vary from the equipment that you have.
Except visual inspection, all of amplifier, microscope, online or offline AOI equipment can be
applied if the pitch of IC is quite small to check.
c. Inspection Standard
Please follow SOP to do inspection or any other general standards (IPC Standard and SJ / T10670-
1995 SMT General Technical Requirements)
Adjust the programming file according to the placement effect after the first production test
If there is any issue of specification, direction and polarity, please follow process file to amend.
d. If the components are off, please adjust the file by following two methods
e. If the placement effects of all components are off in the same direction, it would be the fiducial
issues. Please resolve this issue by adjusting the coordinate of fiducials according to its value of
deviation.
f. If there are several components off beyond allowance, you’d better adjust their coordinates on
working file with downward-looking camera.
g. If there are couple of issues occur during test, some other points need to be considered.
h. Frequent pickup failure. Some suggestions are listed below,
The pick height is inappropriate, please revise the value after an inspection or a pick-test;
The pick offset needs an adjustment, it should be aligned with the center of component reel slot
rather than that of component.
Due to peel strength or installation issue of wasted film, the film on tape won’t be peeled
completely:
The nozzle was blocked
The nozzle is damaged or has a crack
The size issue of nozzle would cause air leakage or insufficient suction.
The air hose is blocked or has a leakage problem, and even the pump has an issue.
i. Frequently throwing components. Some suggestions are listed below,
upward-looking camera can’t take a clear picture of component due to brightness issue for example.
34
⑺
⑹
⑸
⑷
The size or shape isn’t aligned with that in “Footprint library”
The size of nozzle is inappropriate or insufficient suction.
The nozzle is damaged or blocked, and even has a crack
4.7.8 P&P programming page
This screen contains a list of available programs stored in the internal SSD, and is the screen from
which production operations are launched. The NeoDen4 is shipped with several factory test programs
installed, and these can either be kept, deleted or stored separately on an external USB drive for later
use. Available commands on this screen include:
Export to U Disk:
This command will copy the program file selected on the main screen to a USB
drive inserted into any of the four USB ports on the machine. It is recommended that files on the SSD
be backed up to a USB drive.
Import from U Disk:
This command will copy a program from an external USB drive to the
NeoDen4 and store it on the internal SSD. Programs are run from the internal SSD only.
Delete:
This command will permanently delete the selected program file from the internal SSD.
Copy: This command will copy the selected program file, allow the entry of a name for the copied
file, and store it on the internal SSD. The command is useful for creating alternative versions of
programs.
New:
Creates a new, blank program file.
Edit: This command opens the main programming interface for the machine. All parameters needed
to complete a finished board are entered in the two screens of this interface. A detailed discussion is
contained in section.
Mount: This command loads a program from the internal SSD in preparation for automatic or
stepped operation.
Continuous SMT production:
Follow the SOP to start production Notes
Do not touch the surface to board to avoid damaging the printed solder paste. 2.When the error message
occurs, please check out and solve it a.s.a.p.
Once reloading the component during production, pay attention to the model, specification, polarity
and direction of components.
5. Structure and maintenance instruction
5.1
Structure chart
⑴
⑻
⑵
⑼
⑶
⑽
⑾
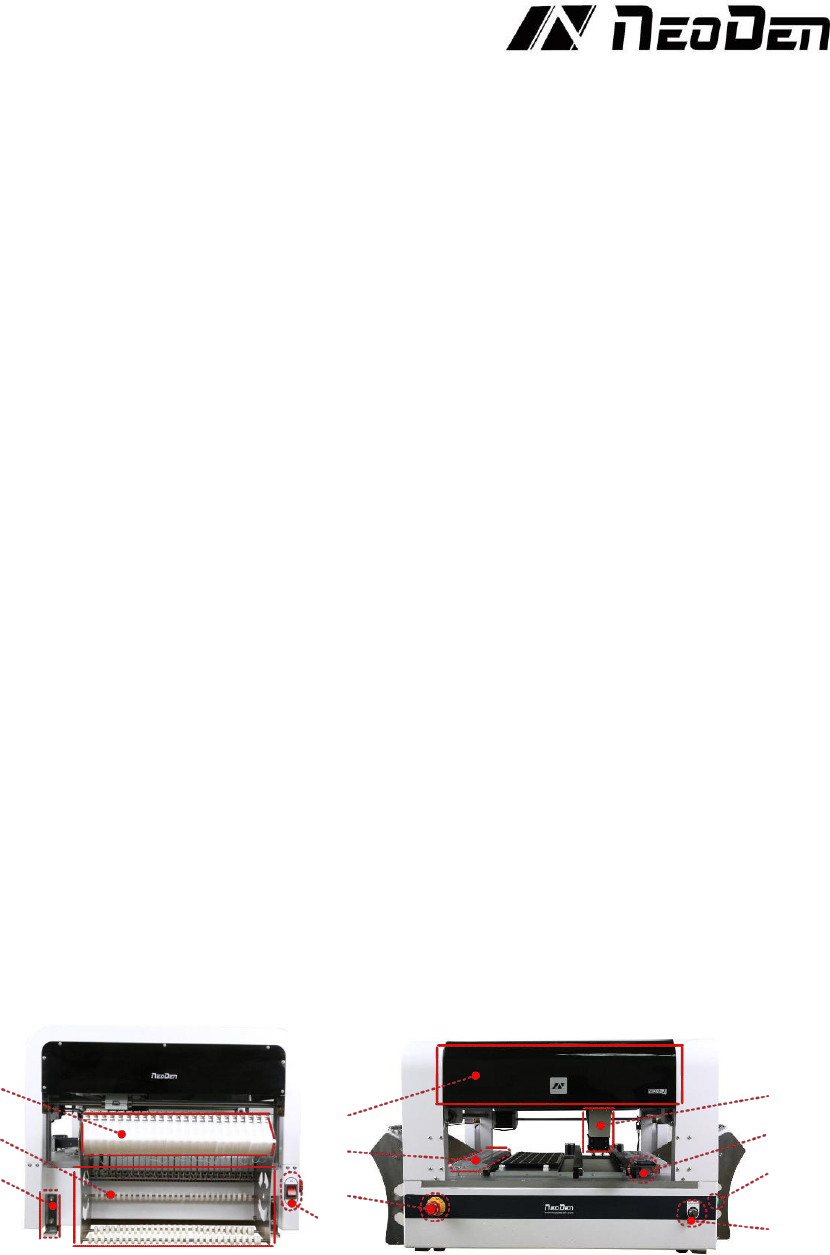
1-1 Side view 1-2 Front view
⑴Peeler
⑵Tape & Reel holder
⑶fixed support
⑷Power switch
⑸Emergency stop
⑹Feeder
⑺Cover
⑻Placement head
⑼Vibration feeder
⑽ Pause button
⑾ Conveyor port
35
⒂
⑻
⒀
⑿
⑹
⒁
⑼
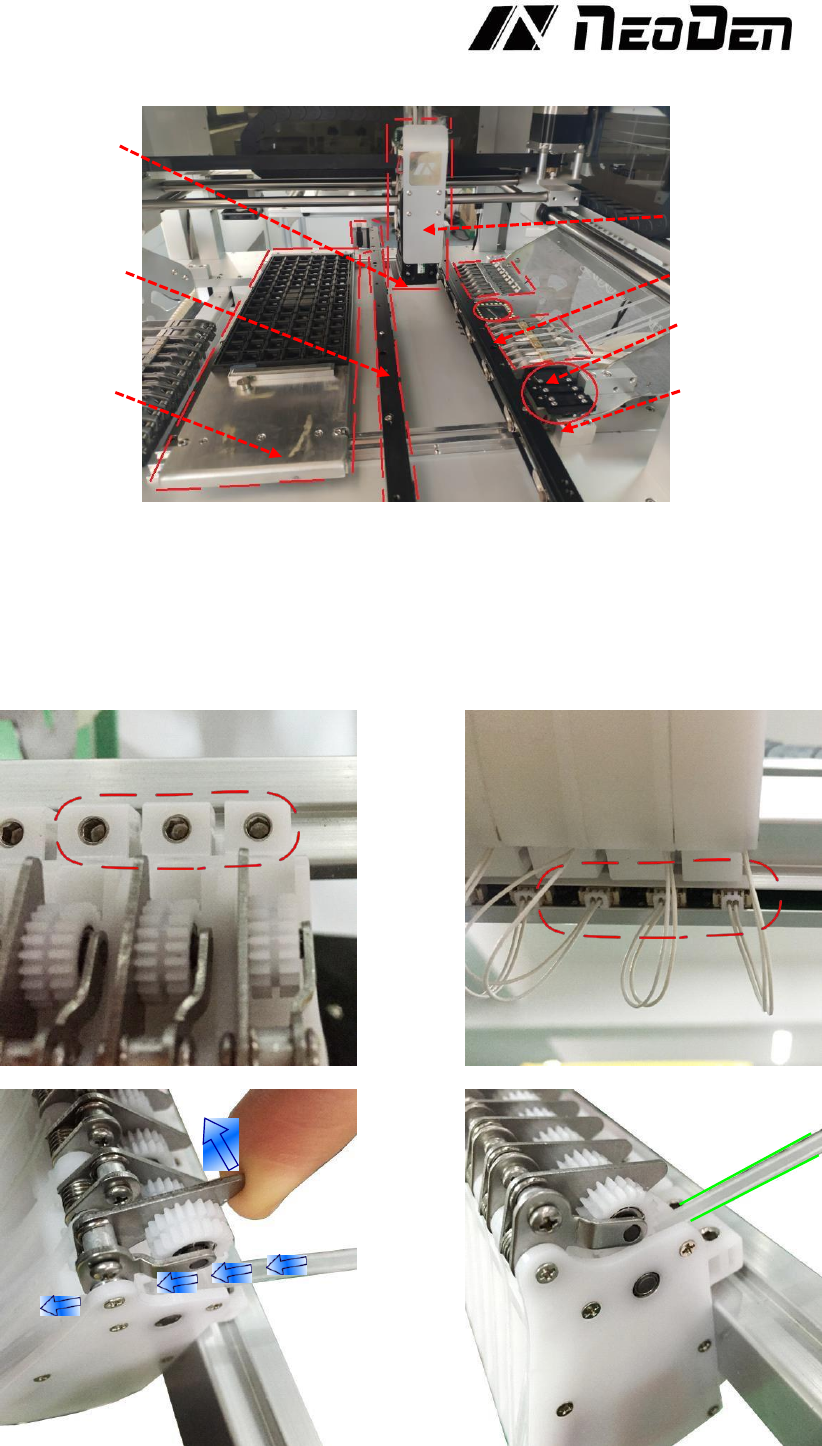
⑿ Upward-looking camera ⒀ Auto-rails ⒁ PCB support board
⒂
Nozzles
5.1.1 Peeler
Fix the peeler
Installation of peeler