User-Manual-of-NeoDen4-PNP-machine.pdf - 第47页
42 5.3 Nozzle The size o f nozzle Please ch oose no zzles acc ording to the sha pe and s ize of componen ts. Tab le 1-1 Nozzle Model CN030 CN065 CN140 CN220 CN400 CN750 Illustration Inner diameter 0.3mm 0.65mm 1.4mm 2.2m…
41
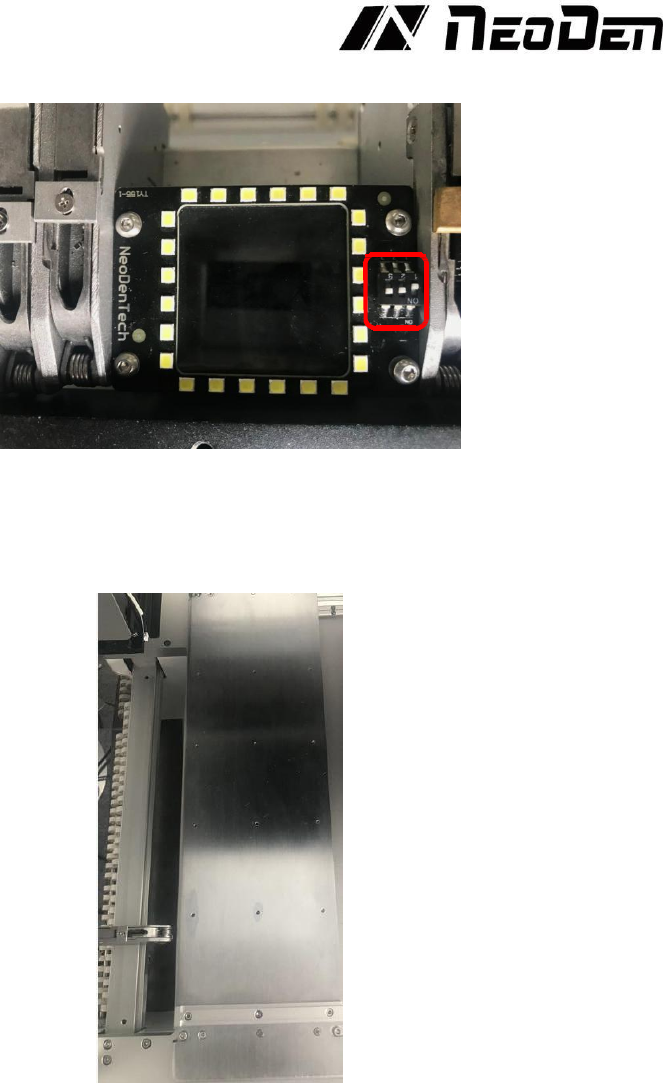
Flash board of the upward-looking Camera:
Figure 5.5
Adjust the brightness of the camera by gear switch, to work with different components. See the
Figure 5.5.
High magnetic positioning plate
Figure 5.6
Use high magnetic positioning plate to fix PCB and IC tray. See the Figure 5.6.
42
5.3
Nozzle
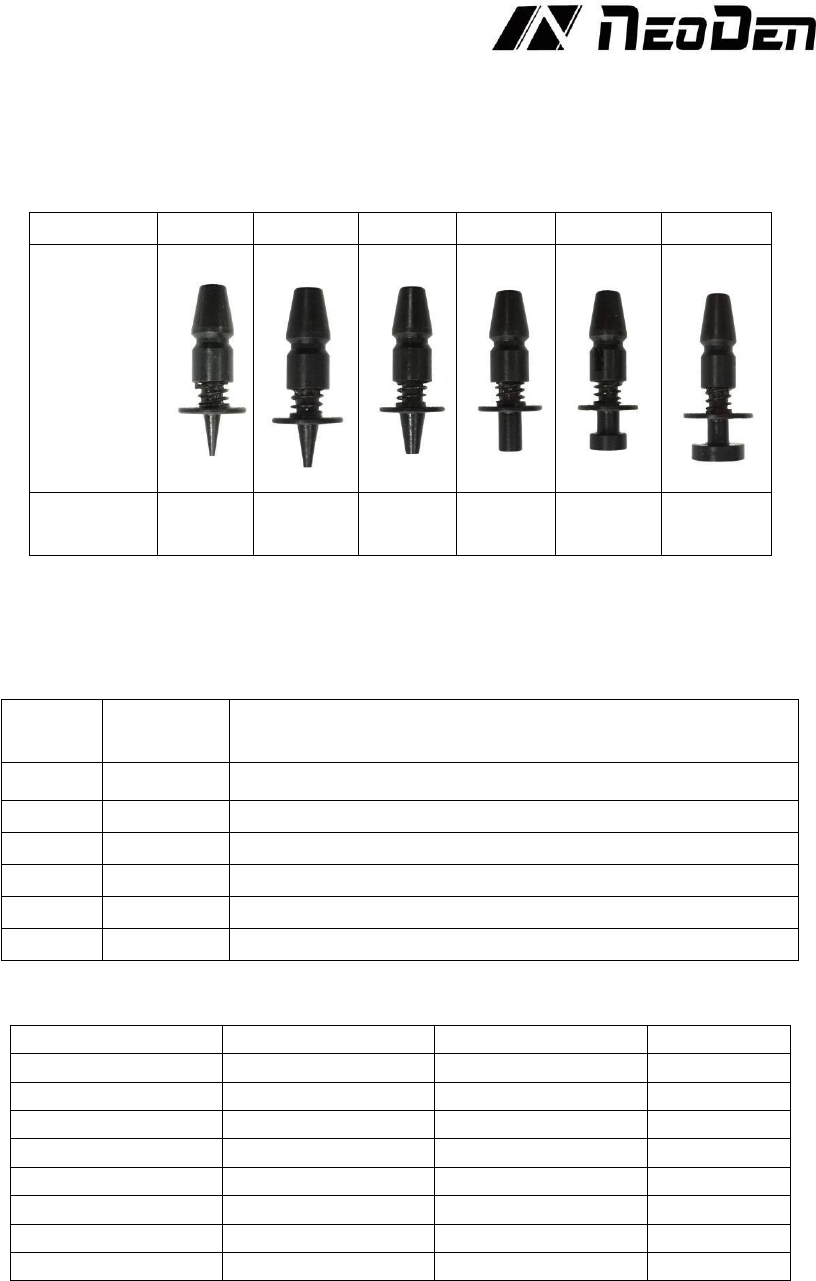
The size of nozzle
Please choose nozzles according to the shape and size of components.
Table 1-1 Nozzle
Model
CN030
CN065
CN140
CN220
CN400
CN750
Illustration
Inner
diameter
0.3mm
0.65mm
1.4mm
2.2mm
4mm
7.5mm
Reference of nozzle selection
In order to assure placement accuracy, please select nozzles according to the shape and size of
components.
Table 1-2 Size comparison of nozzles
Size
Minimum
diameter
Recommendation
CN030
0.2mm
0201,0402
CN065
0.5mm
0402,0603,0805, diode
CN140
1.2mm
1206,1210,1812,2010, SOT23,5050
CN220
2.0mm
SOP series ICs, SOT89, SOT223, SOT252
CN400
4.0mm
ICs from 5 to 12mm
CN750
7.5mm
ICs bigger than 12mm
size
size
0201
0.6*0.3
0402
1.0*0.5
0603
1.6*0.8
0805
2.0*1.2
1206
3.2*1.6
1210
3.2*2.5
1812
4.5*3.2
2010
5.0*2.5
SMA
4.0*2.5
SMB
4.0*3.3
SMC
6.6*5.6
SOT23
3*1.4
SOT89
4.5*2.5
SOT223
6.4*3.7
TO252
6.5*6.3
43
5.4
Maintenance
5.4.1 Take effective measures to reduce/ avoid malfunction
(1)
Reinforce daily maintenance
(2)
P&P machine is that high-accuracy device which requires a clean working environment with
constant temperature and humidity, so it’s necessary to have a routine maintenance.
(3)
Requirements for operator
(4)
Operator should get a basic operator training, which should cover fully all the skills and
knowledge needed to safely operate the type of pick and place machine.
(5)
Operating strictly against equipment’s instruction. DON’T use machine with problems. Stop the
machine once malfunction appears and contact with the after-sales service staff, restart to work after
problem solved.
(6)
Operator should be concentrated.
(7)
Observation-- to see whether there is abnormal situation, such as peel-box doesn’t work, plastic
tape is broken etc.
(8)
Listening-- whether have strange sound, such as noise from placement head, sound of loss
component, strange noise of conveyor etc.
(9)
Handwork--solve some small problems in time, such as install feeder, correction placement
position etc. If the main machine body or circuit problem, please consult after-sales staff.
Formulate measures to reduce/ avoid big problem.
(10)
The most easily appeared problem during work are placement wrong components and
placement misaligned. Supply below measures for ref.
(11)
It needs to check whether the components’ package is matched with related feeder. If not,
please correct them.
(12)
As to tape reel feeder, when ran out of one reel, operator must check whether newly changed
tape reel is correct or not.
(13)
After import the SMD file or edit chip list manually, please recheck each component’s No.,
nozzle rotation angle and placement position to make sure correct.
(14)
Operator must check the first finished PCB of each file. If any problem, please find solutions
such as revise program to solve it.
(15)
To check the placement position misaligned or not, component loss problem in regular work.
Find reason in time and solve it.
(16)
In sum, P&P machine’s running speed and placement accuracy still has limit. People’s work is
important to run machine on its proper role. So, it’s necessary to comply with effective measures to
keep machine normal work, its placement quality and efficiency.