APC - 224650 Issue 1.pdf - 第102页
APC SOFTWARE SETUP AND REC OMMENDED SETTINGS SOFTWARE SETUP PARAMETERS 2.6 All Purpose Clamping (APC) Manual Chapter Issue 1 Nov 16 OTS V acuum Mode If vaccum tooling is fitted, the vacuum can be set to engage before or …
APC SOFTWARE SETUP AND RECOMMENDED SETTINGS
SOFTWARE SETUP PARAMETERS
Chapter Issue 1 Nov 16 All Purpose Clamping (APC) Manual 2.5
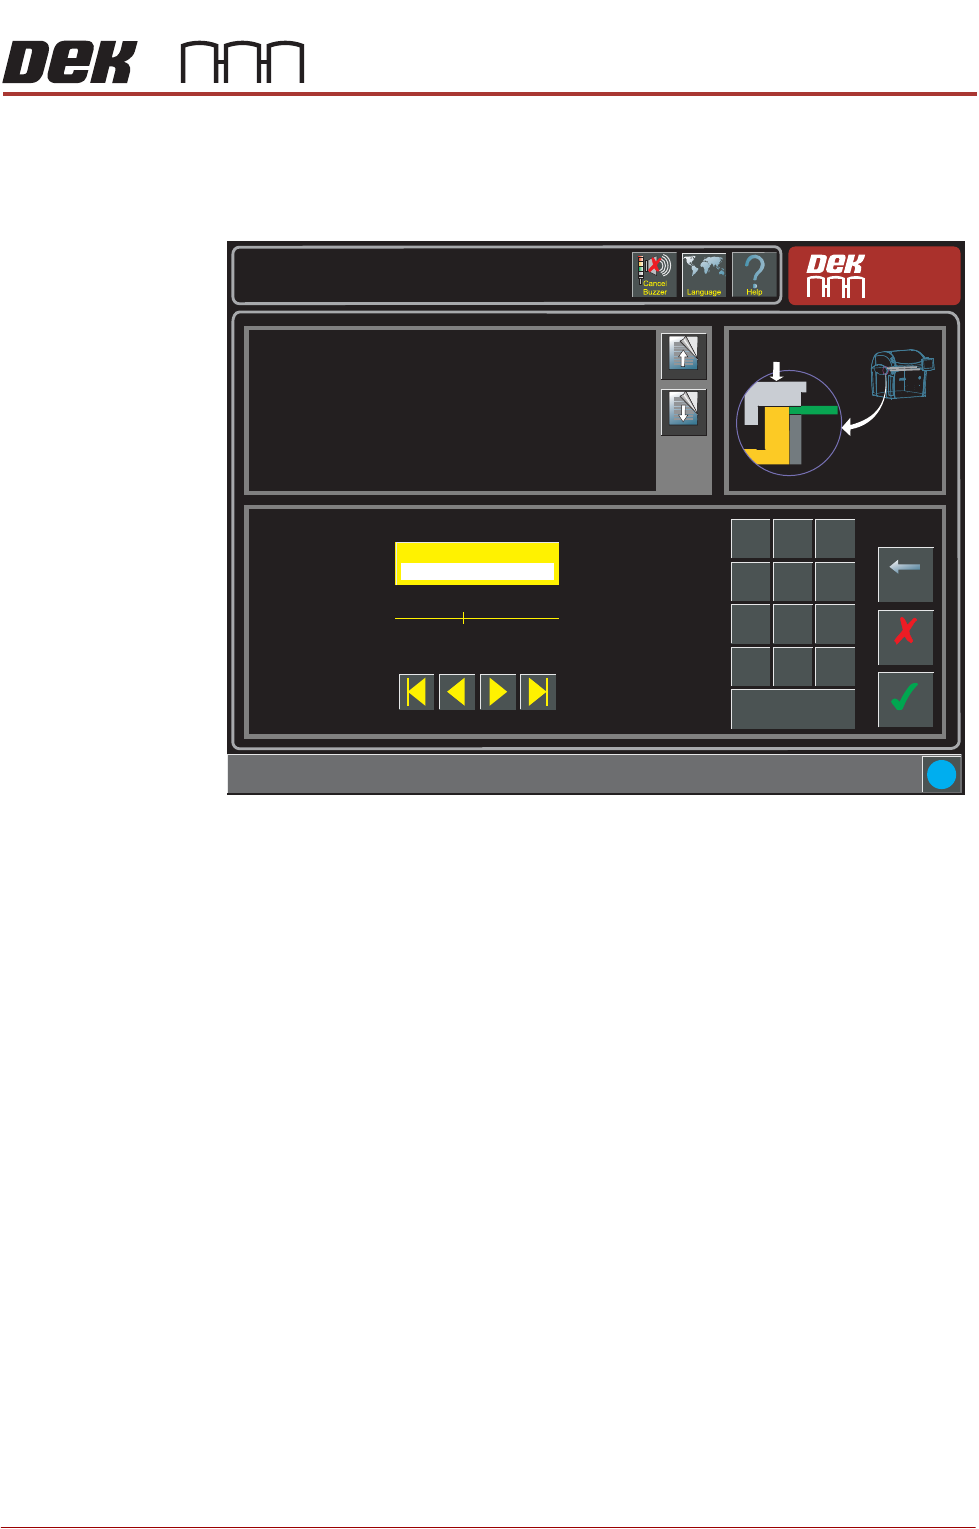
Clamp Pressure The over the top clamp is placed over the board and pressure is applied so that
when the board is fed into the machine and the snugger operates, the top of the
board is held level with the snugger. A minimum of 1.5 and maximum of 5 bar
can be set, 1.5 bar of pressure is required to overcome the balance valve.
Setup \ Tooling
Page Up
Page
Down
This parameter represents the pressure applied to flatten the board before
snugging.
Accept
Cancel
Clamp Pressure ( bar )
3.0
Backspace
Min
1.5
Max
5.0
7
8 9
4
5
6
1 2
3
0
.
+/-
Apply
i
APC SOFTWARE SETUP AND RECOMMENDED SETTINGS
SOFTWARE SETUP PARAMETERS
2.6 All Purpose Clamping (APC) Manual Chapter Issue 1 Nov 16
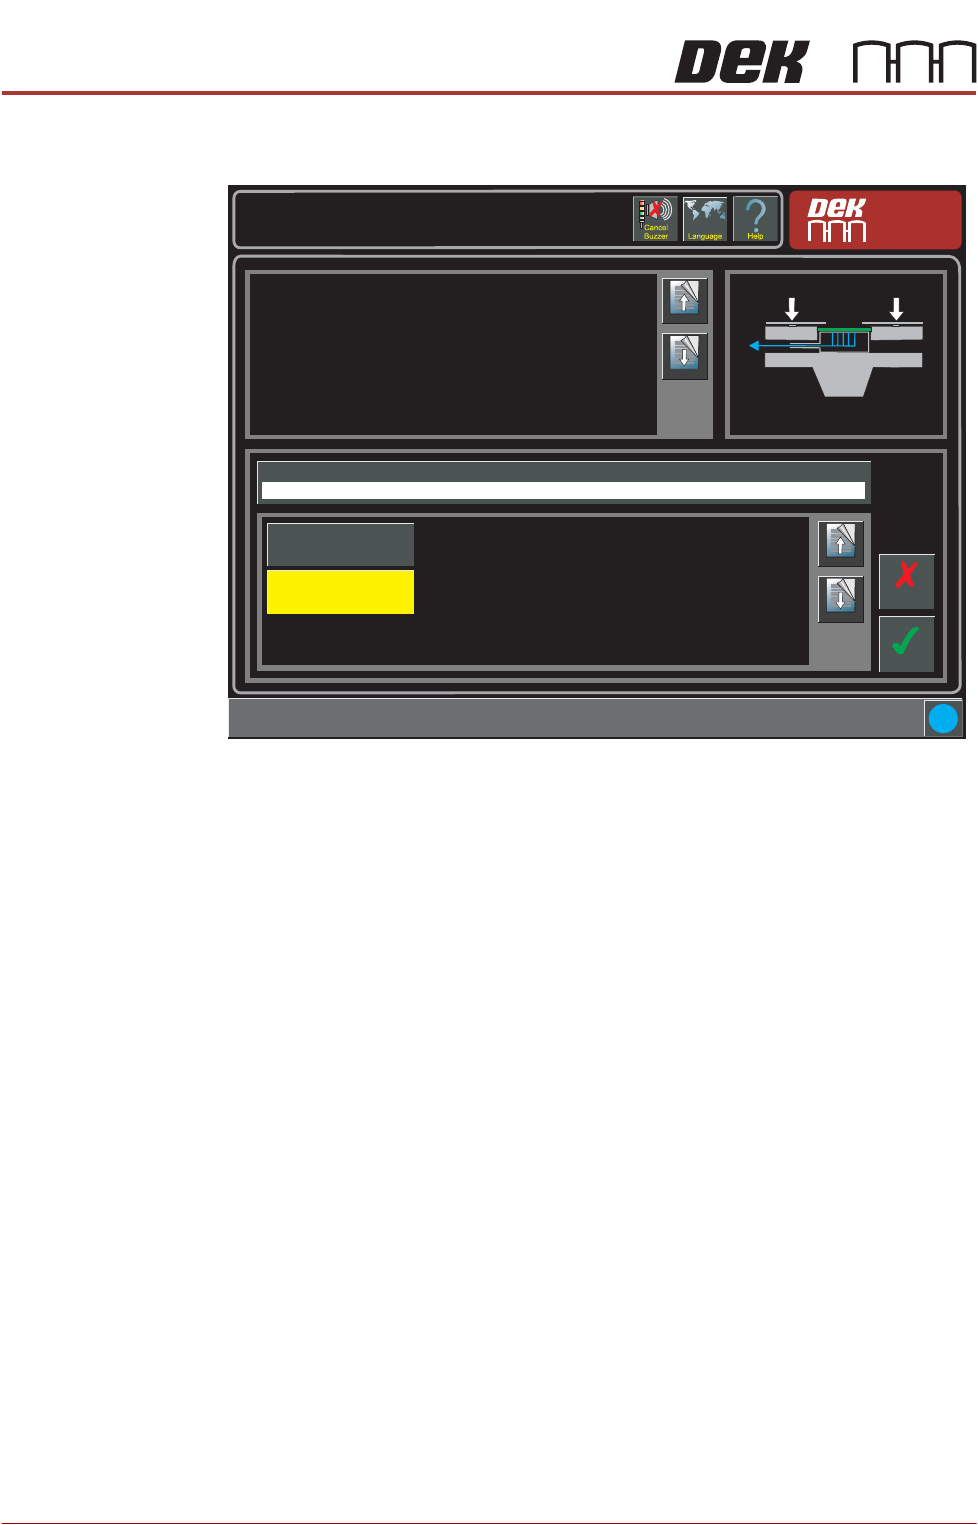
OTS Vacuum Mode If vaccum tooling is fitted, the vacuum can be set to engage before or after the
board is clamped/snugged.
Setup \ Tooling
Page Up
Page
Down
This parameter sets determines if the vacuum is to be applied before or
after snugging and clamping the board.
If the board snuggers are applied and the board becomes dislodged it
cannot be clamped. To prevent any movement, the vacuum is applied
beforehand.
The options are:
Before
The product is held by the vacuum prior to snugging and clamping taking
place.
After
The board edges are flattened by the clamps before the vacuum is applied.
Accept
Cancel
i
OTS Vacuum Mode
Before
Page Up
Page
Down
After
Before
APC SOFTWARE SETUP AND RECOMMENDED SETTINGS
CALIBRATION
Chapter Issue 1 Nov 16 All Purpose Clamping (APC) Manual 2.7
CALIBRATION
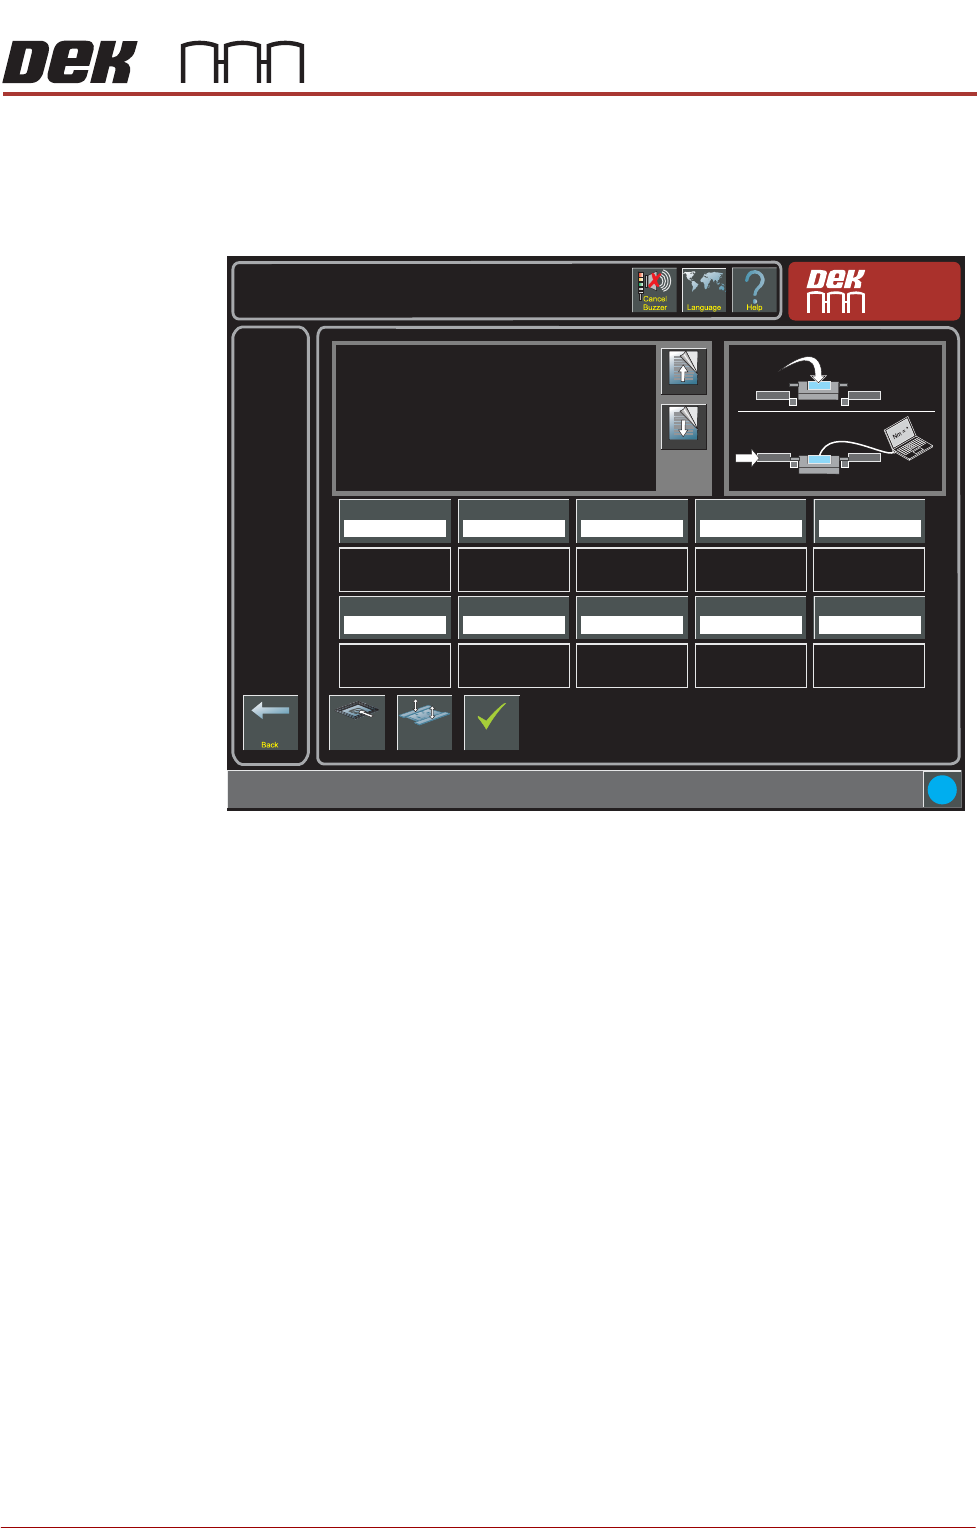
The APC Calibration is a part-software / part-hardware procedure for calibrating
the torque force used when clamping. The calibration page can be found at
Maintenance -> Machine Setup -> Basics -> APC Calibration page.
Using a calibration jig and a laptop with specialist software installed, the torque
force requested by the machine software and the actual force applied on the
machine can be measured, compared and adjusted to ensure accurate forces
are being applied.
NOTE
See Snug Force Calibration in the All Purpose Clamping chapter of this manual
for details of the calibration procedure.
Torque Value 1
27.0%
i
Maintenance \ Machine Setup \ Basics \ APC Calibration
Page Up
Page
Down
On selecting this parameter, the rising table moves to
transport height, the transport rails are checked for boards,
and the rear rail is moved into position to allow the user to
place the test jig between the front and rear rails.
The ten read only Torque Value parameters represent the
percentage of the torque delivered. The torque applied to
the jig is measured by the sensor at its centre. Selecting
Torque On/Off applies torque to the jig, selecting Torque
On/Off again releases it.
Values are input into the ten Calibration Value parameters
Load Screen
Board
Clamps
Accept
Torque Value 2
28.0%
Torque Value 3
29.0%
Torque Value 4
30.0%
Torque Value 5
31.0%
Calibration Value 1
20.0 Newtons
Calibration Value 2
25.0 Newtons
Calibration Value 3
30.0 Newtons
Calibration Value 4
35.0 Newtons
Calibration Value 5
40.0 Newtons
Torque Value 6
32.0%
Torque Value 7
33.0%
Torque Value 8
34.0%
Torque Value 9
35.0%
Torque Value 10
36.0%
Calibration Value 6
45.0 Newtons
Calibration Value 7
50.0 Newtons
Calibration Value 8
55.0 Newtons
Calibration Value 9
60.0 Newtons
Calibration Value 10
65.0 Newtons
Nm