APC - 224650 Issue 1.pdf - 第38页
ALL PURPOSE CLAMPING (APC) ADJUSTMENTS AND SETTINGS 1.26 All Purpose Clamping (APC) Manual Chapter Issue 1 Nov 16 25. Using a 3mm Allen key slacken the four ret aining screws, passing through the upper bearing carriage a…
ALL PURPOSE CLAMPING (APC)
ADJUSTMENTS AND SETTINGS
Chapter Issue 1 Nov 16 All Purpose Clamping (APC) Manual 1.25
13. Ensure that Home Rail Width is highlighted.
14. Select Run Diagnost.
15. Select Exit.
16. Use Next or Previous to highlight Rising Table.
17. Select Run Diagnost.
18. Use Next or Previous to highlight Rising Table to Transport Height.
19. Select Run Diagnost.
20. Open the front printhead cover.
21. Remove any tooling from the manual tooling plate.
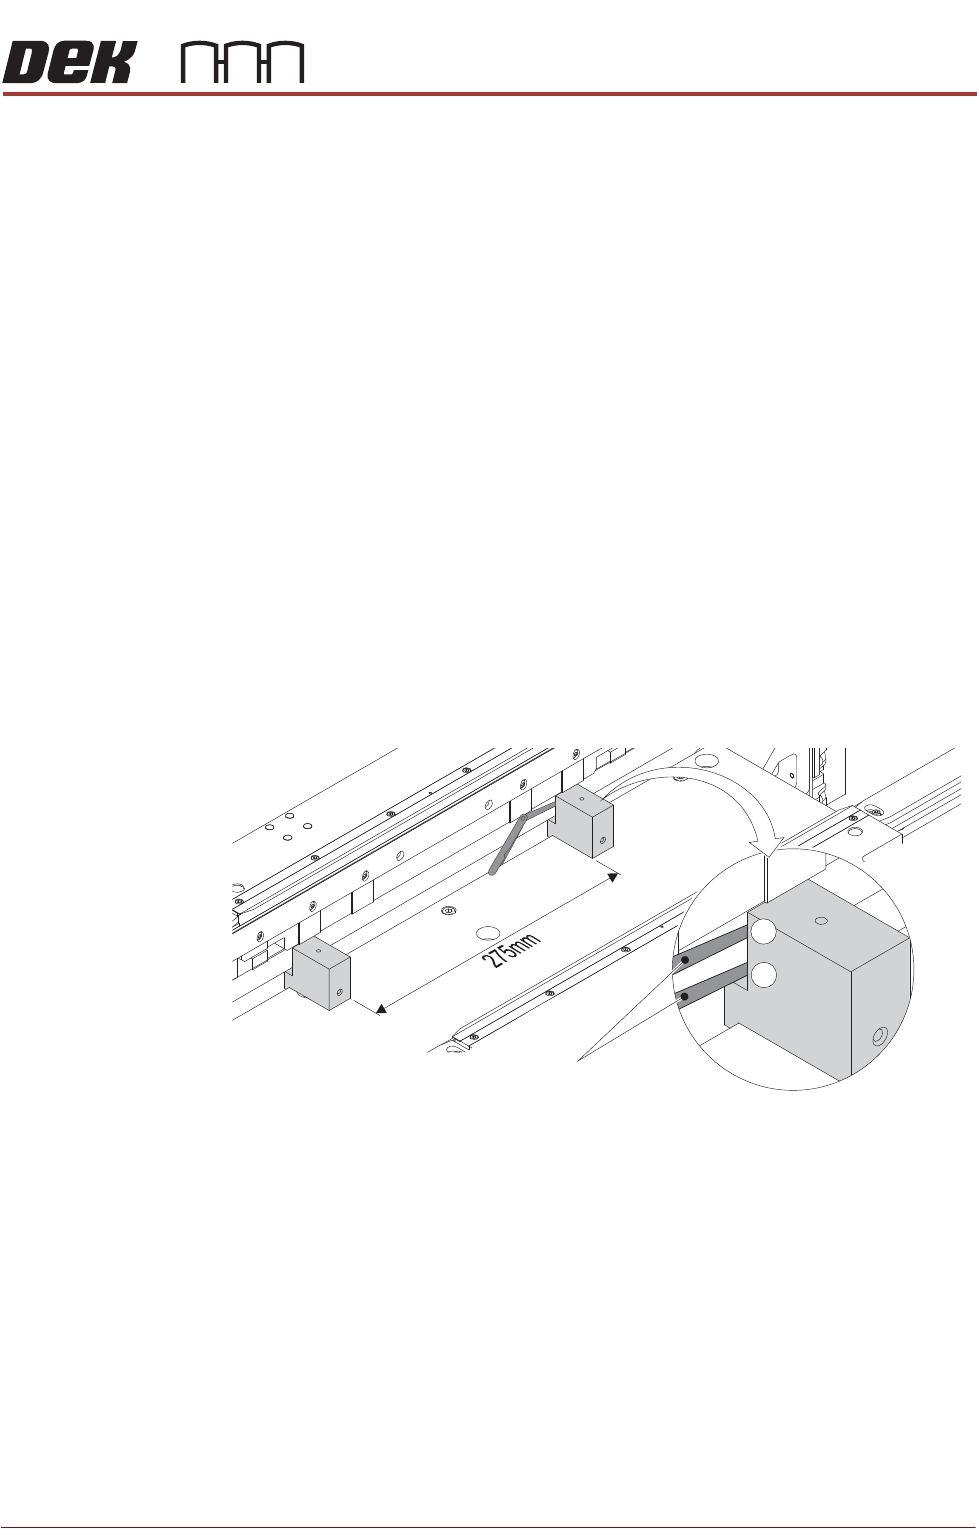
22. Place the rail setting jigs (Part No 205816) on the manual tooling plate,
spaced approximately 275mm apart about the centre, ensuring that they are
against the front of the table.
23. Using the jog buttons, carefully lift the table until the rails are clear of the
clatter bars.
24. Using a 0.05mm feeler gauge as a no-go gauge, check positions 1 and 2
(shown in graphic) on both rail setting jigs.
If a gap >0.05mm is present, adjustment is needed. Continue at Step 25.
If adjustment is not necessary continue at Step 31.
View on Rear of Front Rail
0.05mm Feeler Gauge
1
2
ALL PURPOSE CLAMPING (APC)
ADJUSTMENTS AND SETTINGS
1.26 All Purpose Clamping (APC) Manual Chapter Issue 1 Nov 16
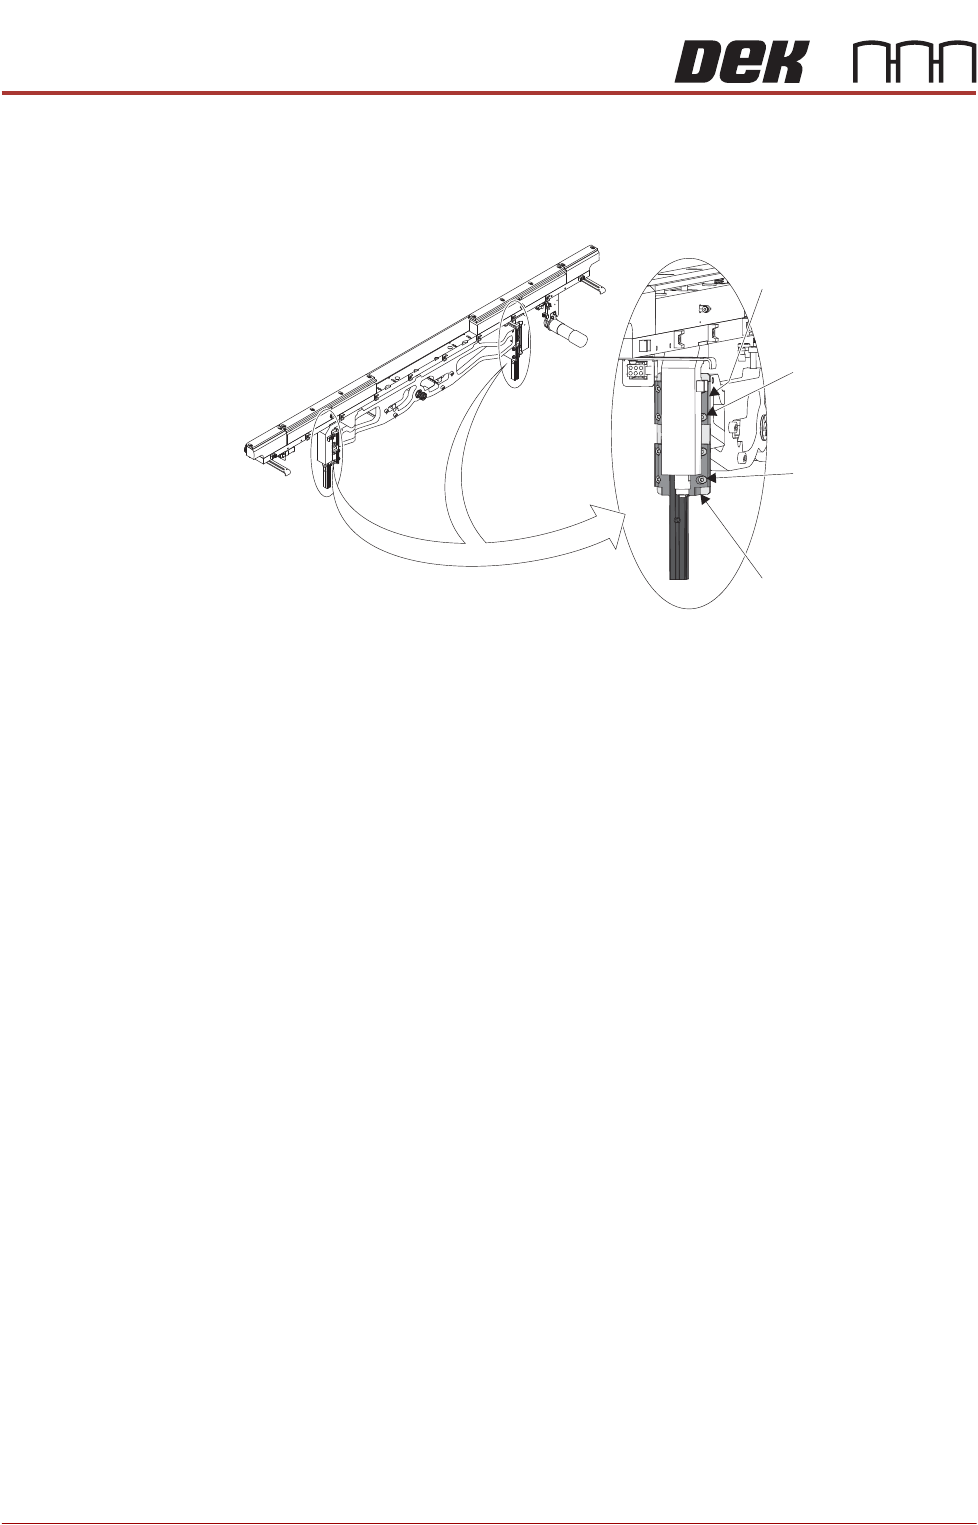
25. Using a 3mm Allen key slacken the four retaining screws, passing through
the upper bearing carriage and connecting mount, and attaching the left
hand transport leg to the rail support arm. Repeat for the lower bearing
carriage.
26. Repeat Step 25 for the right hand transport leg.
27. Move the transport rail until it sits snugly in both rail setting jigs. The correct
setting is shown in Step 24.
28. Tighten the retaining screws on both the left and right hand upper bearing
carriages.
29. Recheck the parrallelism as detailed in Step 24.
30. Tighten the retaining screws on both the left and right hand lower bearing
carriages.
31. Remove the rail setting jigs from the rising table.
32. Close the front printhead cover.
33. Press the System button.
34. Select Exit.
35. Select Exit.
36. Select Back.
Rear Rail
Parallelism
NOTE
Ensure Front Rail Parallelism has been carried out prior to commencing this
procedure. It is recommended that the rear rail parallelism procedure is carried
out by two persons.
1. Select Shut Down.
2. Select Continue.
3. Switch the mains isolator to OFF.
4. Remove the left and right hand side panels (if necessary, disconnect the air
and electrical supplies and remove the printer from the production line).
Upper Bearing Carriage
Upper Rail Support
Arm Screws (4 off)
Lower Bearing Carriage
Lower Rail Support
Arm Screws (4 off)
ALL PURPOSE CLAMPING (APC)
ADJUSTMENTS AND SETTINGS
Chapter Issue 1 Nov 16 All Purpose Clamping (APC) Manual 1.27
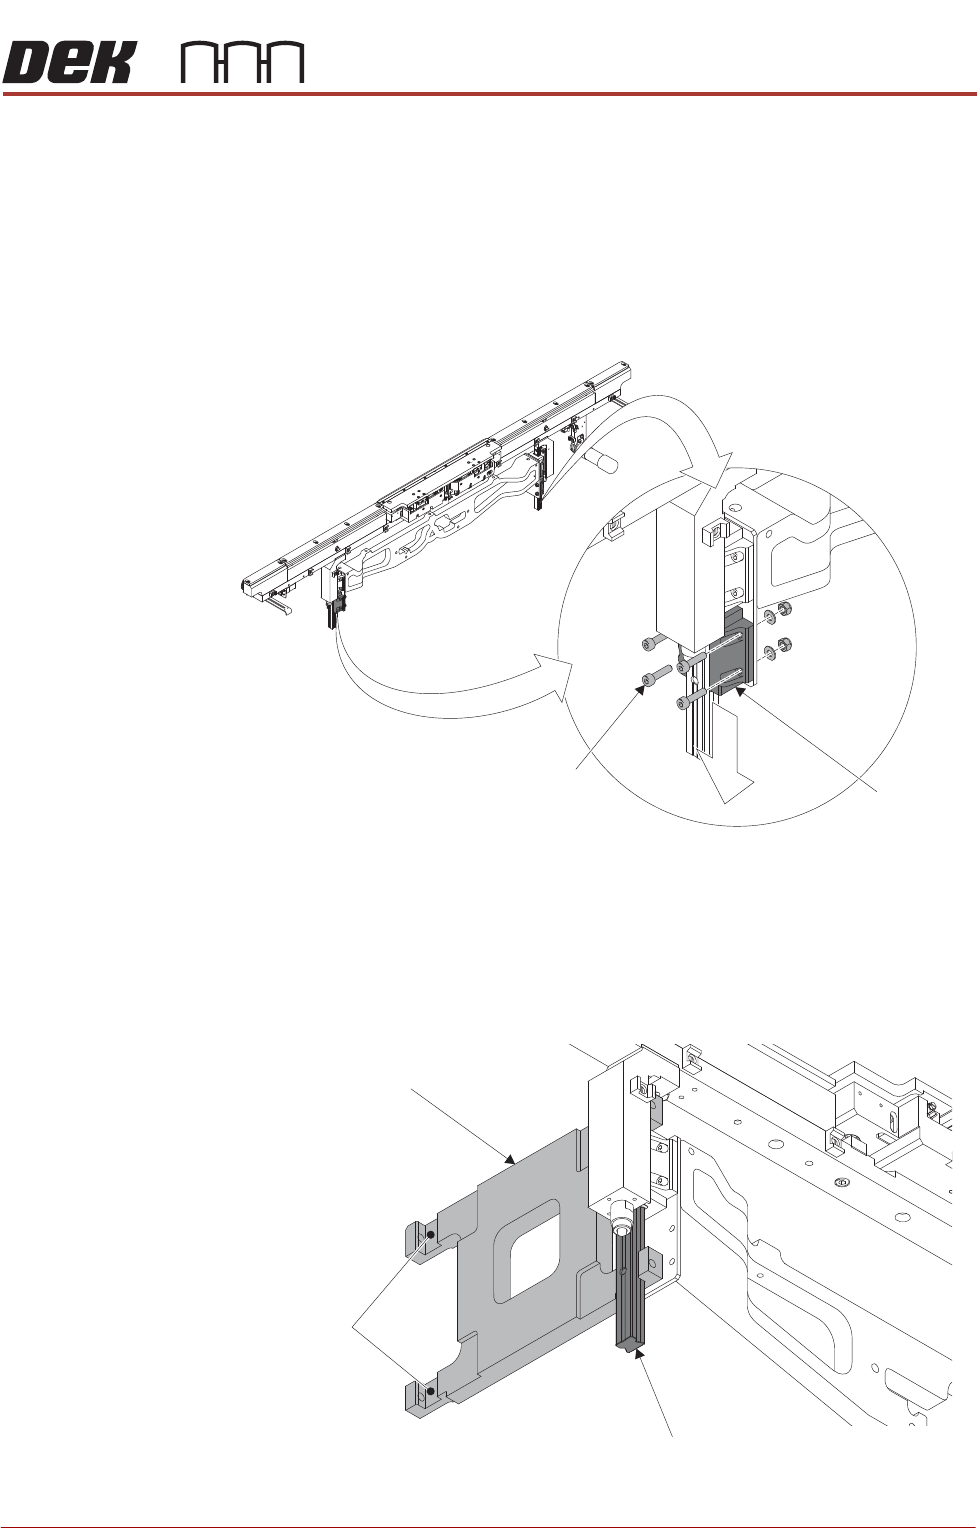
5. Locate the lower bearing carriages on the front transport rail left and right
leg linear guides. Remove the four retaining screws from each lower car
-
riage, and then remove the carriage by sliding off the bottom of the linear
guide.
NOTE
The upper and lower bearing carriages on each leg are matched sets, to
enable correct position and orientation on re-assembly they should be
marked/identified in some way.
6. Repeat Step 5 for the rear transport rail left and right leg lower bearing
carriages.
7. Using a pair of rail parallelism H jigs (Part No 158109) fit the jigs to the front
transport rail left and right leg linear guides. Ensure the linear guides fit
snugly in the jig slots.
Front Rail
Lower
Bearing
Carriage
Retaining Screw
(4 positions)
H Jig
Front Left Linear Guide
Rear Linear
Guide Slot