APC - 224650 Issue 1.pdf - 第43页
ALL PURPOSE CLAMPING (APC) ADJUSTMENTS AND SETTINGS Chapter Issue 1 Nov 16 All Purpose Clamping (APC) Manual 1.31 28. Open the front printhead cover . 29. Check that the jig can be moved lef t to right along the conveyor…
ALL PURPOSE CLAMPING (APC)
ADJUSTMENTS AND SETTINGS
1.30 All Purpose Clamping (APC) Manual Chapter Issue 1 Nov 16
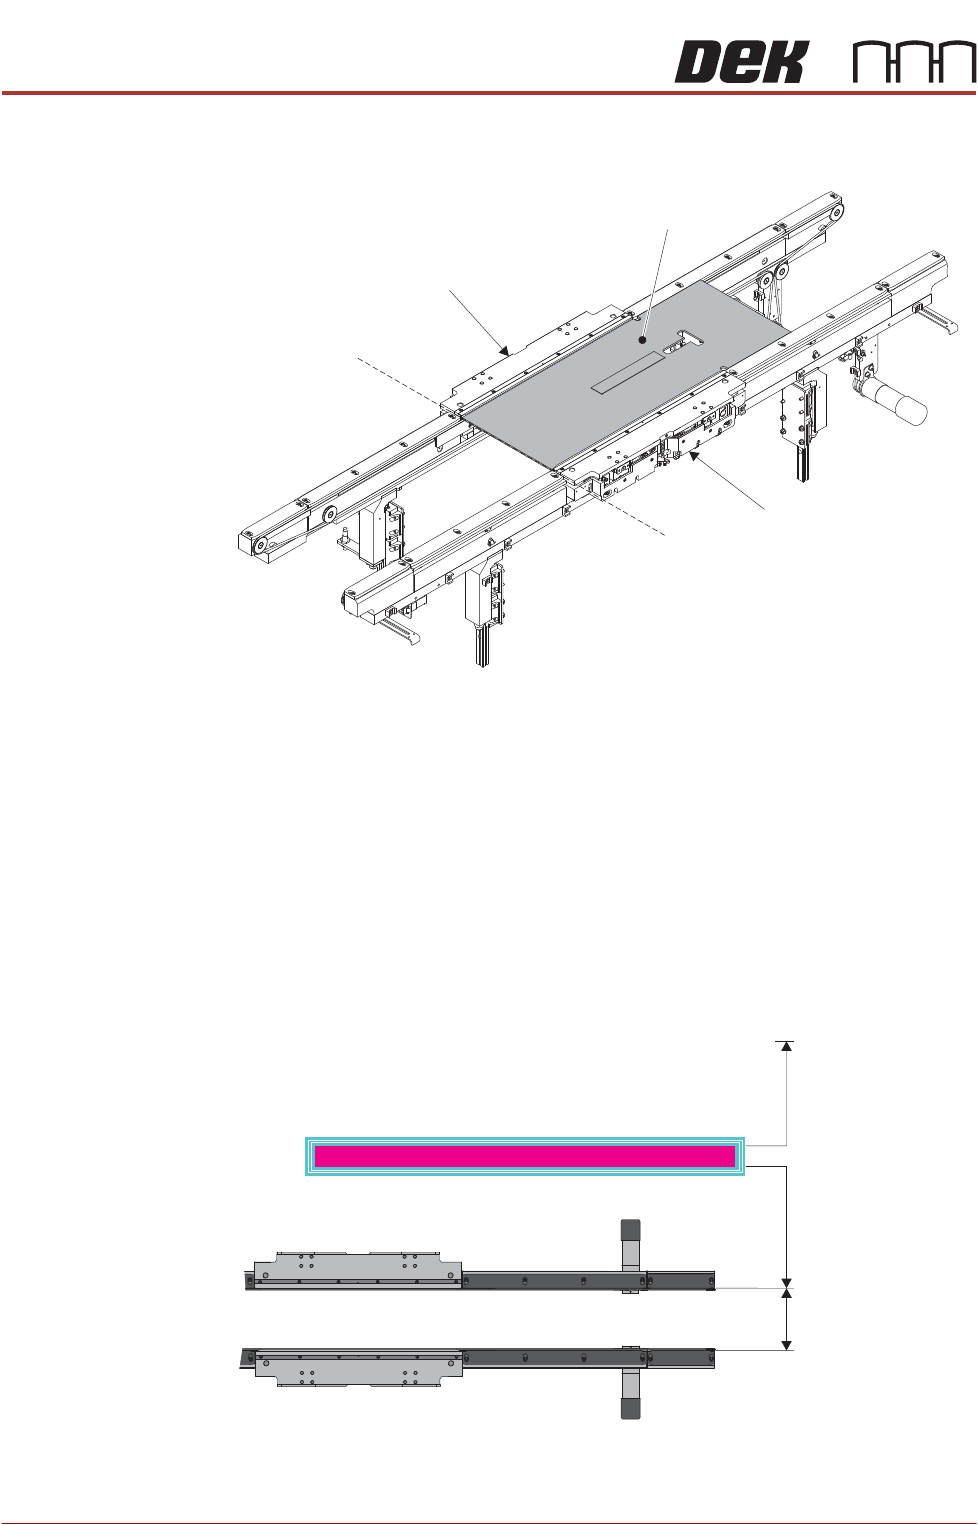
21. Load the APC Conveyor Setting Jig (Pt No. 225240) into the print area. Align
the left-hand edge of the jig with the left-hand end of the APC modules.
22. Close the front printhead cover.
23. Press the System button.
24. Use Next or Previous to highlight Set Rail Board Width Calibration.
25. Select Run Diagnost to open the Rail Width Offset window.
26. Use Incr. or Decr. to set the offset required to hold the jig.
NOTE
Increasing the offset increases the dimension between the rear rail and the
home position, therefore decreasing the width between the front and rear
rails.
27. Select Move.
APC Conveyor Setting Jig
APC Rear Module
APC Front Module
Alignment
Rear of Machine
Rail Width
RAIL WIDTH OFFSET 0.00 mm
ALL PURPOSE CLAMPING (APC)
ADJUSTMENTS AND SETTINGS
Chapter Issue 1 Nov 16 All Purpose Clamping (APC) Manual 1.31
28. Open the front printhead cover.
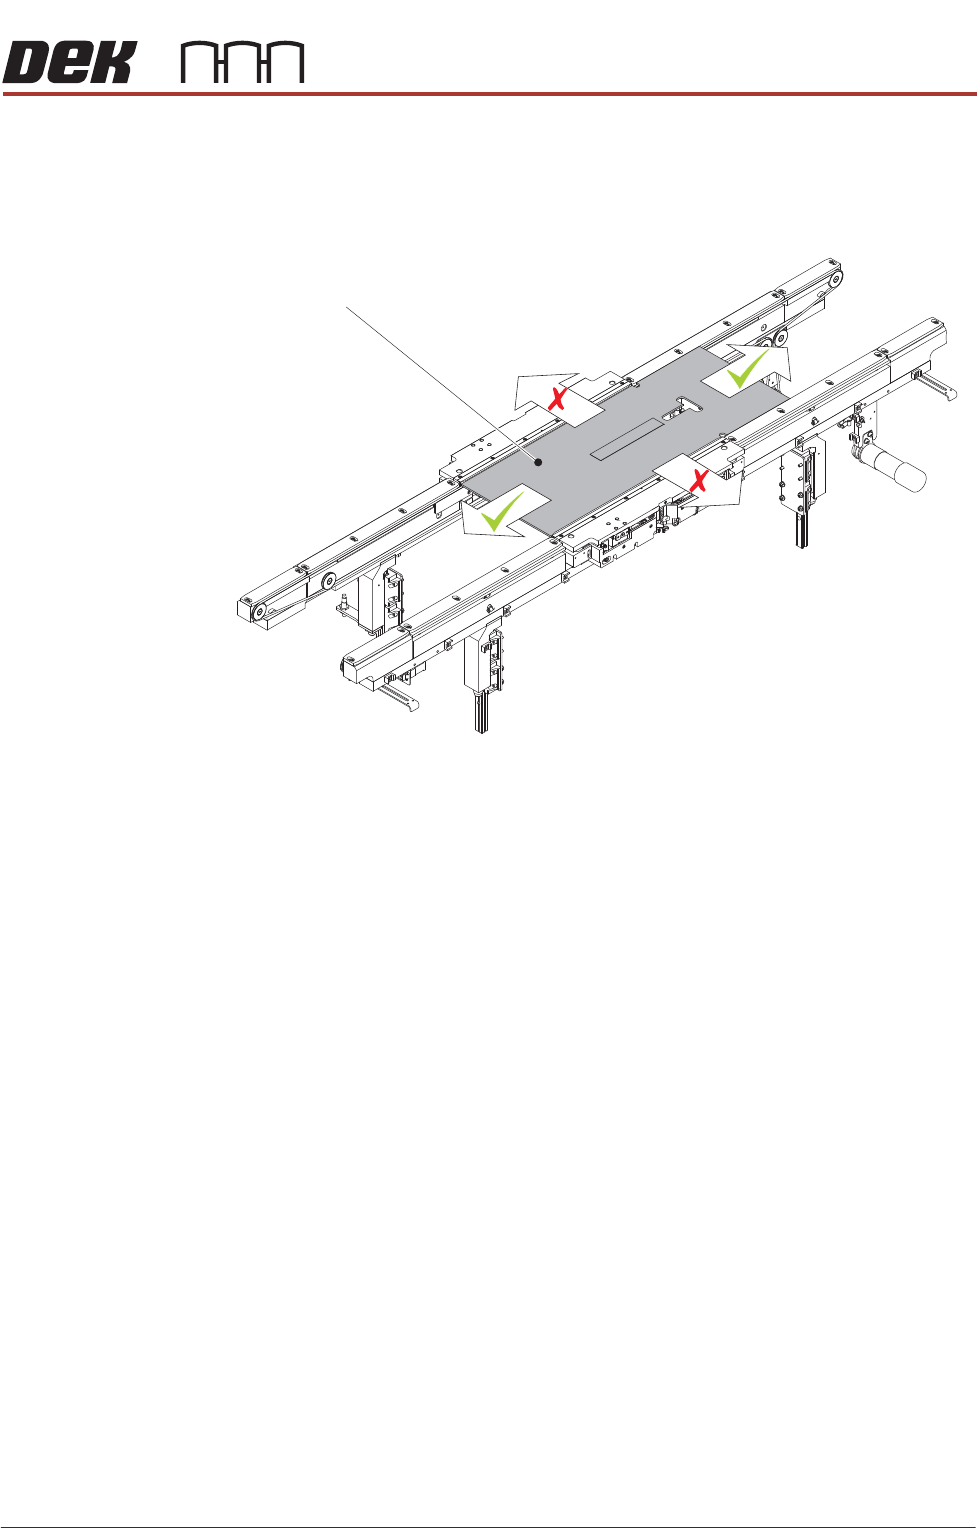
29. Check that the jig can be moved left to right along the conveyor belts but not
back and forth in the Y axis. Any movement in the Y axis indicates too much
clearance and the offset requires further adjustment.
30. If the rail width requires further adjustment, close the front printhead cover,
press the System button and repeat Steps 26 to 29.
31. If the rail width is correct, close the front printhead cover, press the System
button and select Set.
32. Select Yes to save the information.
33. Open the front printhead cover.
34. Push the front and rear mid rail board guides (output end) up against the jig.
Tighten the eight M3 retaining screws (four per guide).
35. Slide the jig to the right, until level with the end rail board guides.
36. Push the front and rear end rail board guides (output end) up against the jig.
Tighten the four M3 retaining screws (two per guide).
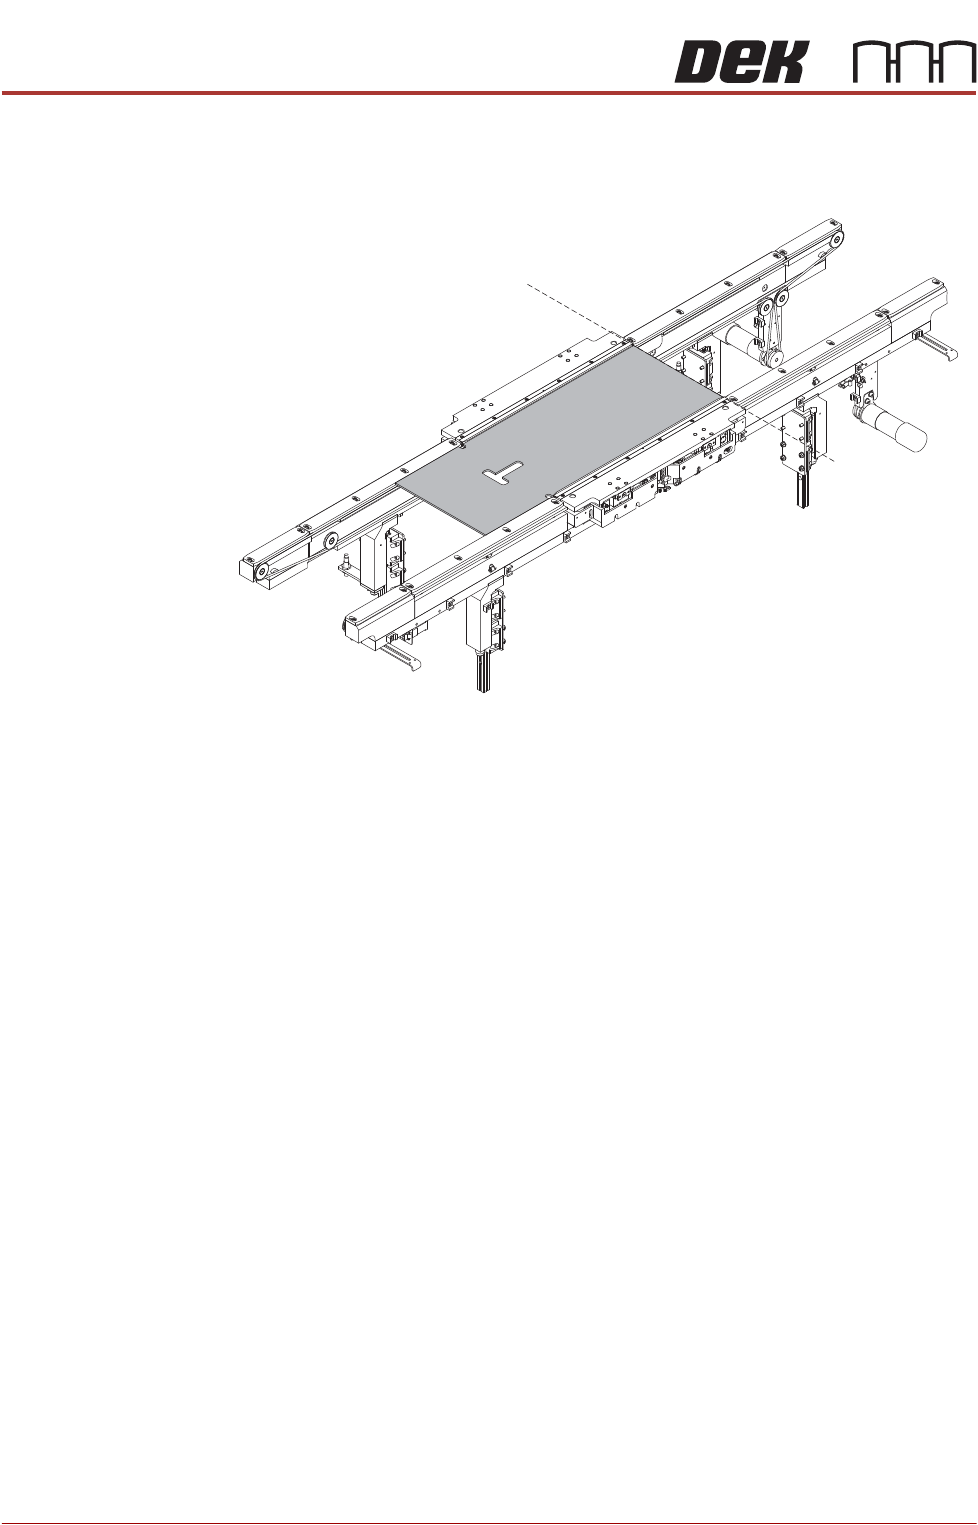
APC Conveyor Setting Jig
ALL PURPOSE CLAMPING (APC)
ADJUSTMENTS AND SETTINGS
1.32 All Purpose Clamping (APC) Manual Chapter Issue 1 Nov 16
37. Remove the setting jig from the machine. Flip over and replace in the print
area. Align the right-hand edge of the jig with the right-hand end of the APC
modules.
38. Repeat Steps 34 to 36 for the input end rail board guides.
39. Remove the setting jig from the machine.
40. Close the front printhead cover, press the System button.
41. Use Next or Previous to highlight Home Rail Width is highlighted.
42. Select Run Diagnost.
43. Select Adjust and set the board width to 250mm.
44. Select Exit.
45. Use Next or Previous to highlight Drive Rail to Board Width.
46. Select Run Diagnost.
47. Open the front printhead cover.
48. Place the calibration board on the input transport rail belts.
Alignment