FUJI NXT Programming Manual QD004-18.pdf - 第196页
6. Editing Jobs on the Machine (MEdit) QD004-18 186 NXT Programming Manual Checking and editing the pickup height for a tray. 22. The [Measu re Pickup Height] st ep is displaye d. Specify the cavity position on which to …
QD004-18 6. Editing Jobs on the Machine (MEdit)
NXT Programming Manual 185
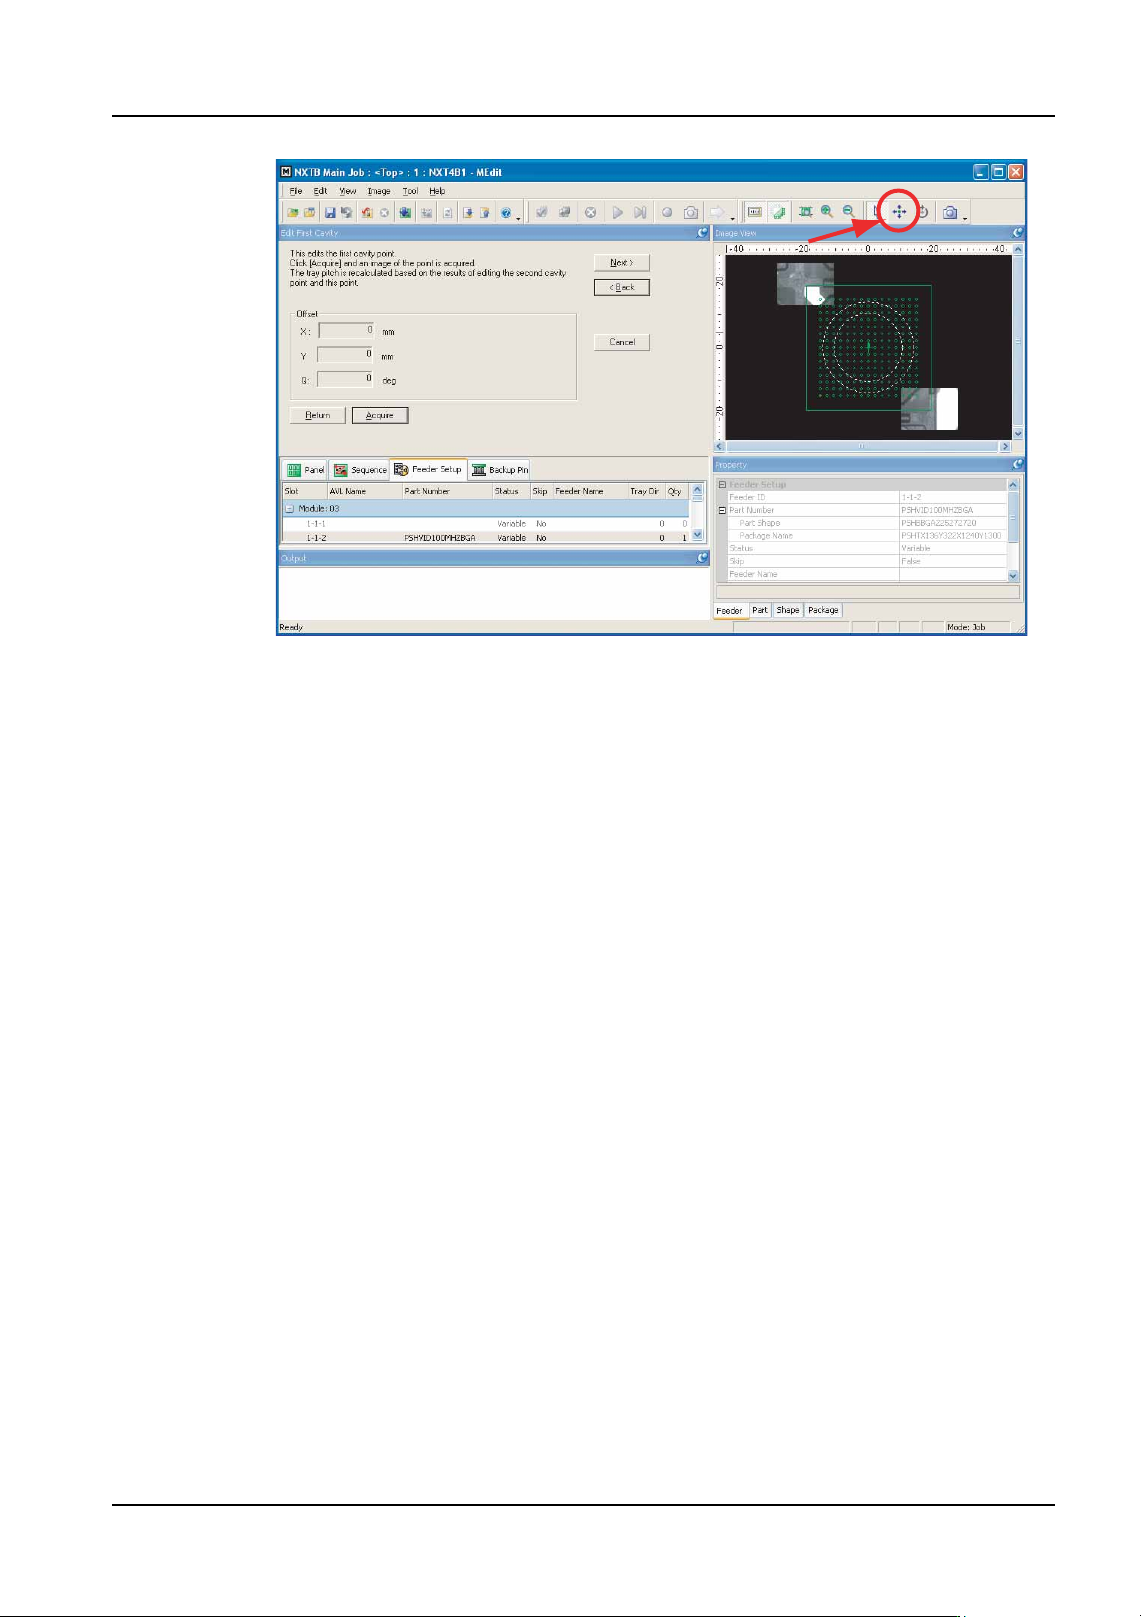
14.Check the pickup position in the X- and Y-direction using the displayed image. If the
pickup position needs to be moved, click the positioning button (the button with the four
arrows) and then click in the image of the graphic at which the pickup should be
performed (the [Offset] values are automatically changed).
15.When the pickup position for the part is correct, click [Next].
16.The step for the second specified cavity is displayed. Click [Acquire] to take a picture of
the part in the second specified cavity in the tray. A picture of the part is taken and
displayed.
17.Check the second pickup position in the X- and Y-direction using the displayed image.
If the pickup position needs to be moved, click the positioning button (the button with the
four arrows) and then click in the image of the graphic at which the pickup should be
performed (the [Offset] values are automatically changed).
18.When the pickup position for the part is correct, click [Next]. If the first pickup position
data is not being edited and pickup height is being measured, then go to step 22. If none
of these are being measured, then go to step 27.
Checking and editing the pickup position for a tray.
19.The step for editing the pickup position is displayed. Click [Acquire] to take a picture of
the part in the specified slot in the tray. A picture of the part is taken and displayed.
20.Check the pickup position in the X- and Y-direction using the displayed image. If the
pickup position needs to be moved, click the positioning button (the button with the four
arrows) and then click in the image of the graphic at which the pickup should be
performed (the [Offset] values are automatically changed).
21.When the pickup position for the part is correct, click [Next]. If the pickup height test is
not being performed, go to step 27.
NXTEJM022Eb
6. Editing Jobs on the Machine (MEdit) QD004-18
186 NXT Programming Manual
Checking and editing the pickup height for a tray.
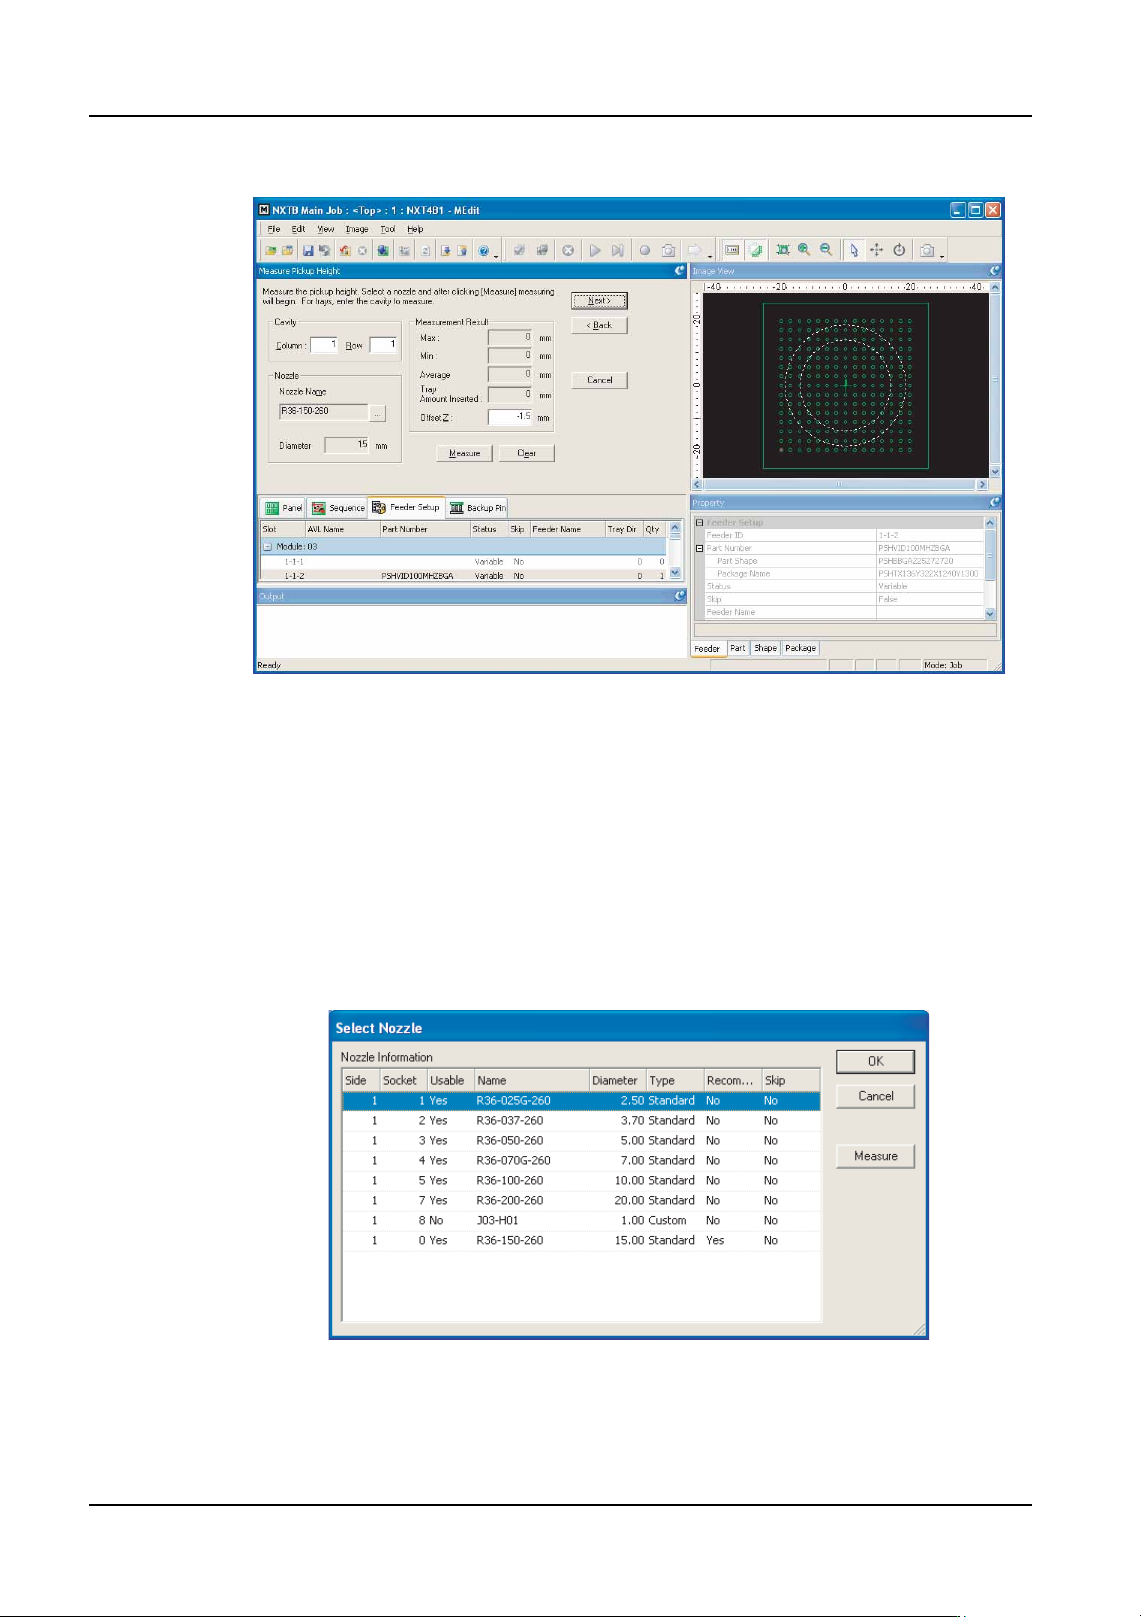
22.The [Measure Pickup Height] step is displayed. Specify the cavity position on which to
perform the pickup test (a part must be present in the cavity) in the [Cavity] group.
Note: Trays have a certain amount of warp. Therefore, the measurement should be performed
at multiple cavities to determine the optimum pickup height. (Fuji recommends measuring
the center cavity and the 4 corner cavities.)
23.If it is necessary to specify a particular nozzle (the nozzle that is to be used in the job is
automatically selected), then follow the sub-steps below.
a. Click [...] to specify which nozzle or claw (OF head only) to use for the test.
Note: The machine knows which nozzles and claws are present in the module (if a check has
been performed by the machine). In cases where the job-specified nozzle and claws can
be used for the height measurement, that nozzle and claws are automatically selected.
b. Select the nozzle or claws (OF head only) to be used for the measurement in the
dialog box that is displayed and then click [OK].
Note: If the module has not yet performed calibration and does not know what nozzles and claws
are present in the nozzle station, click [Measure] to have the module check which nozzles
NXTEJM023b
NXTEJM017Ea
QD004-18 6. Editing Jobs on the Machine (MEdit)
NXT Programming Manual 187
and claws are present.
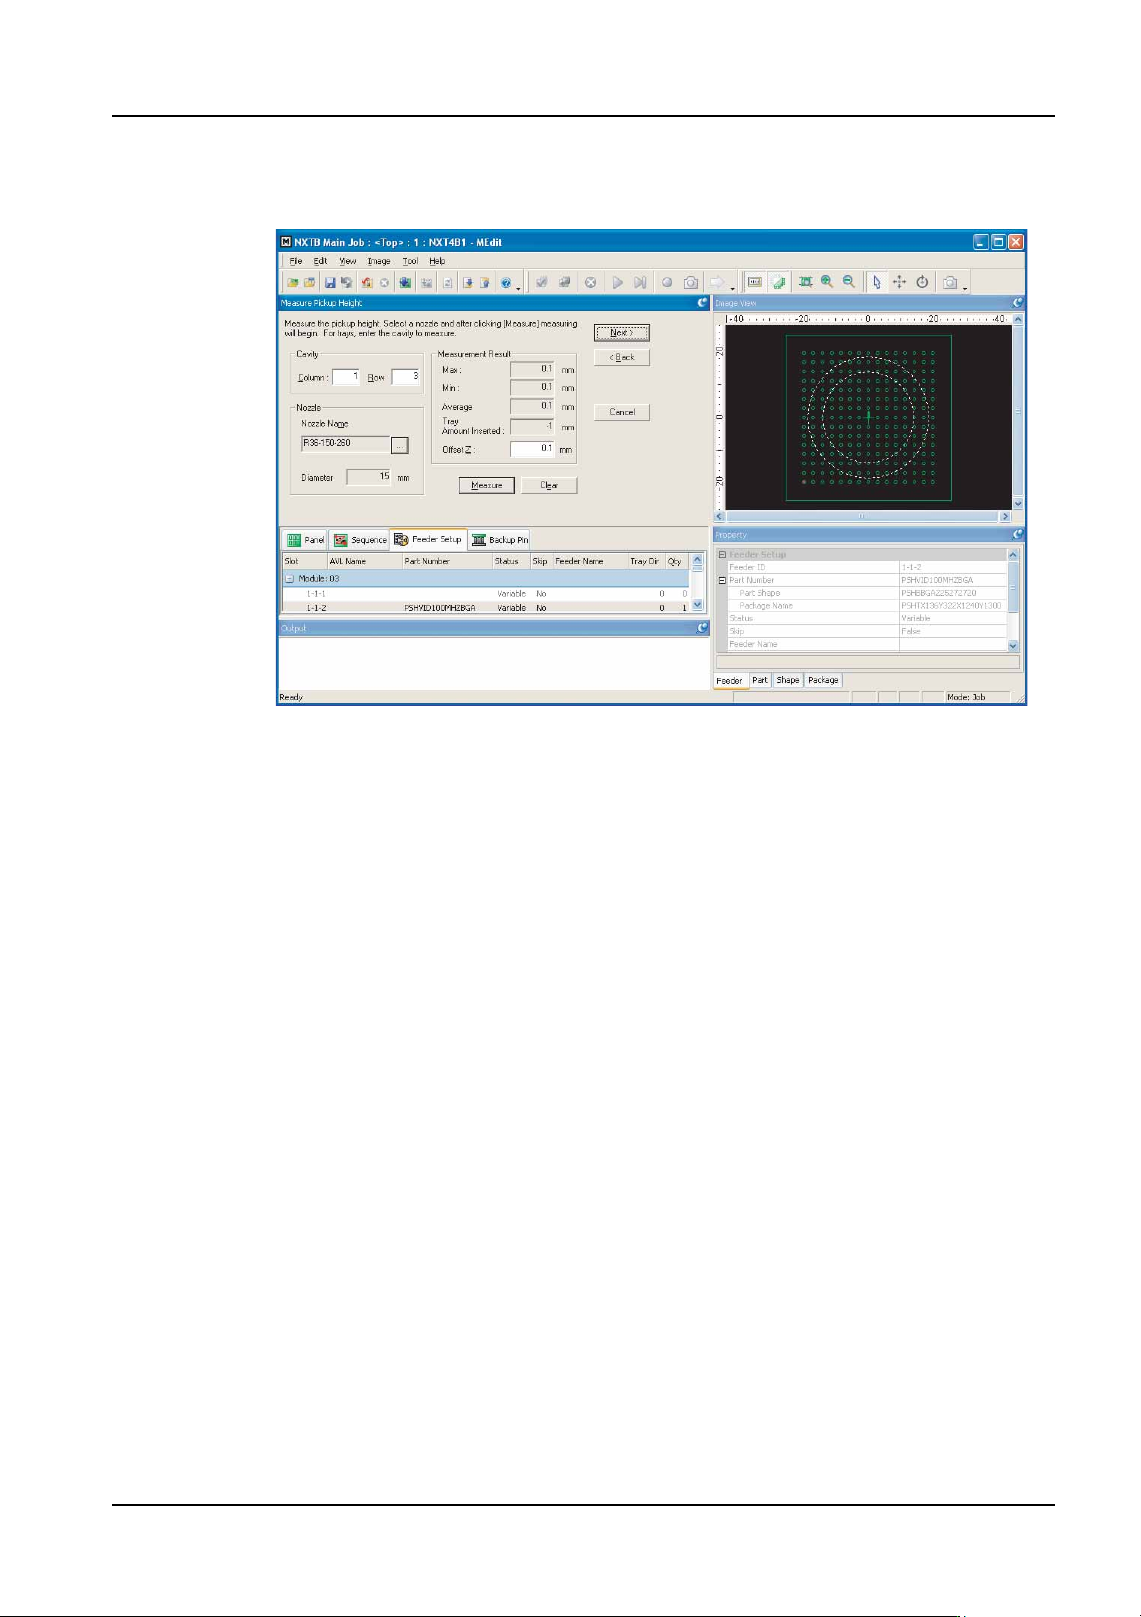
24.Click [Measure] to begin the pickup height test.
25.The results of the test are displayed and the Z offset is automatically determined. It is
possible to manually edit this value.
Note: A dialog box is displayed when a stroke error occurs. Click [Yes] in this dialog box to try
moving the head back down and measure again. The same error occurs if there is no part
in the pickup position. If unsure if a part is present or not, check the part status in the tray.
Caution: If measurement is performed for an OF head, even if the nozzle (claw) does not contact a
part when lowered, the lowest position of the Z-axis is displayed as the result of
measurement. Then, if measurement is performed again, the nozzle (claw) lowers to a
position that is -1.5 mm lower than the result for the previous measurement, so the
measurement value will change greatly. The position at which the result obtained is
approximately the same as the previous result is the position at which the part has actually
been contacted. Due to this, the measurement should be repeated until the result is
approximately the same.
26.Once the Z offset has been determined and the results are acceptable, click [Next].
NXTEJM024Ea