FUJI NXT Programming Manual QD004-18.pdf - 第53页
QD004-18 3. Job Builder NXT Programming Manual 43 3.4.4 Using the M6S and single conveyor S (from NXT V4.30) Make the following settings in t he job before using a single conveyor S at an M6S module. Fuji Flexa V3.4.0 or…
3. Job Builder QD004-18
42 NXT Programming Manual
01PRG-0035
(4)(3)(2)(1)
HH
QD004-18 3. Job Builder
NXT Programming Manual 43
3.4.4 Using the M6S and single conveyor S (from NXT V4.30)
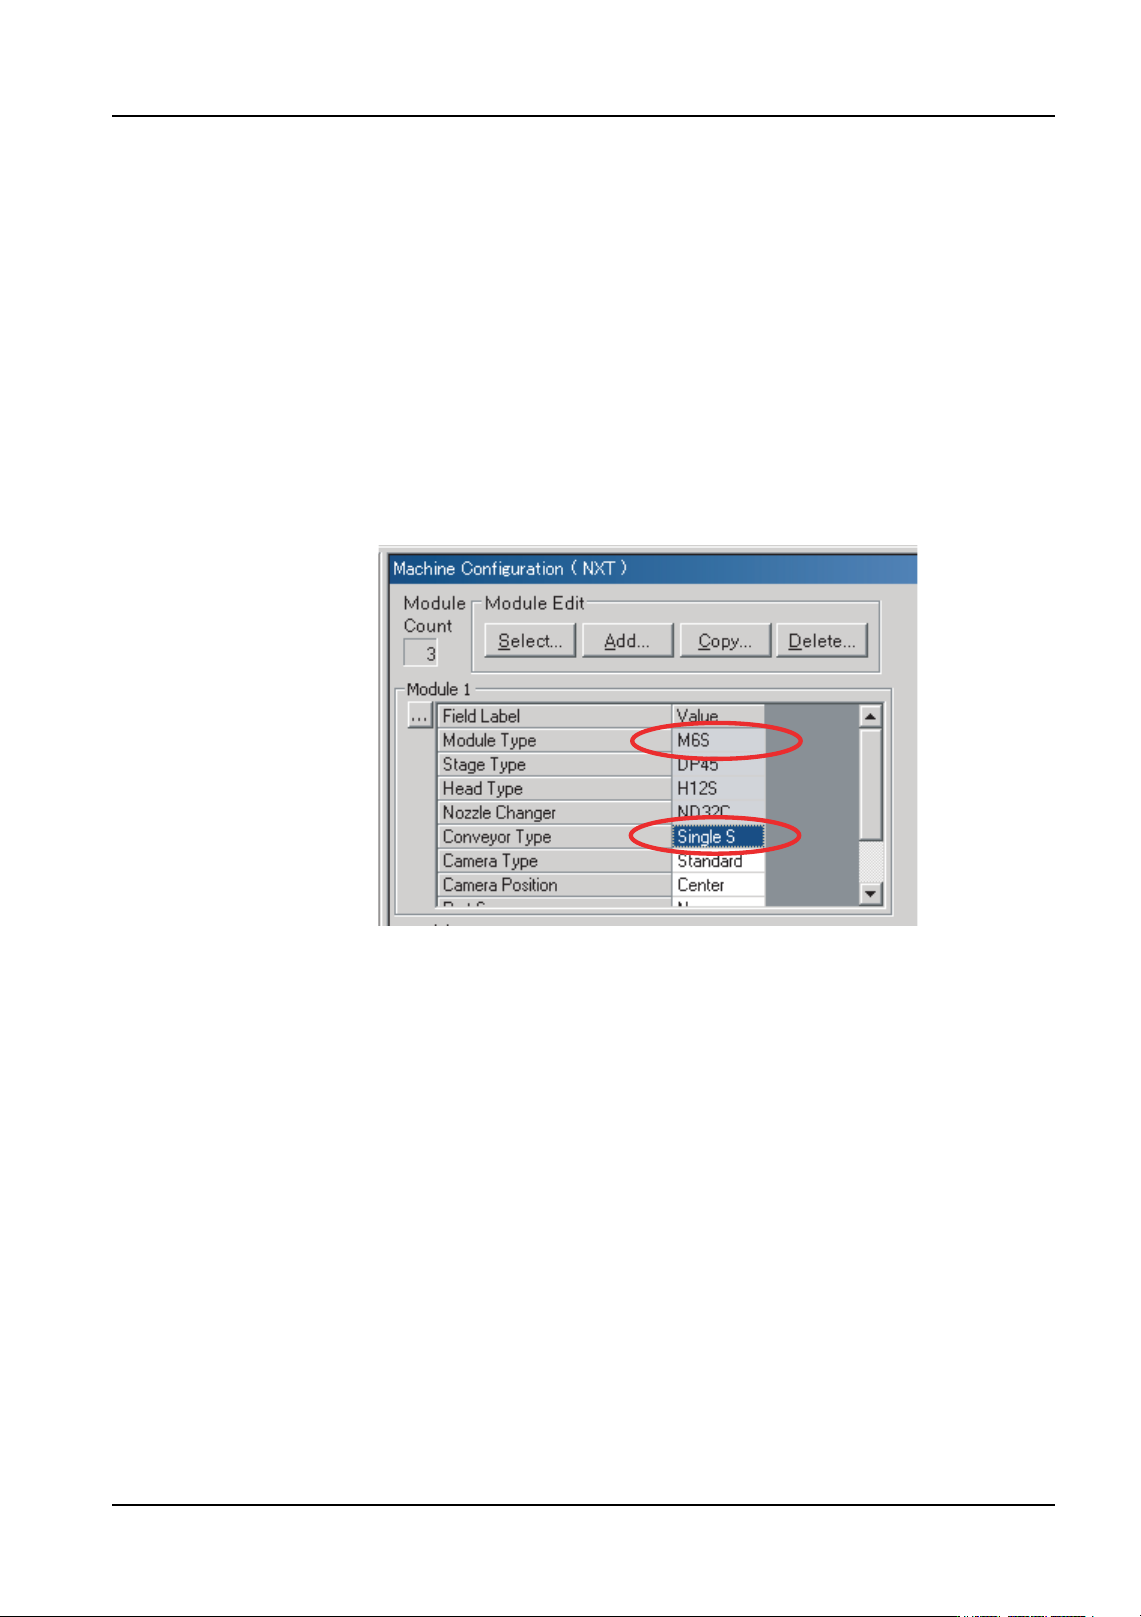
Make the following settings in the job before using a single conveyor S at an M6S module.
Fuji Flexa V3.4.0 or later is required.
Settings
Display the [Machine Configuration] pane of the job in Fuji Flexa (See 3.3.3 "Configuring an
NXT machine" for more details.)
Module configuration
1. Click the [Modules] tab at the bottom of the Machine Configuration pane.
2. Select “M6S” for [Module Type].
3. Select “Single S” for [Conveyor Type].
01PRG-0050E
3. Job Builder QD004-18
44 NXT Programming Manual
Panel conveyance
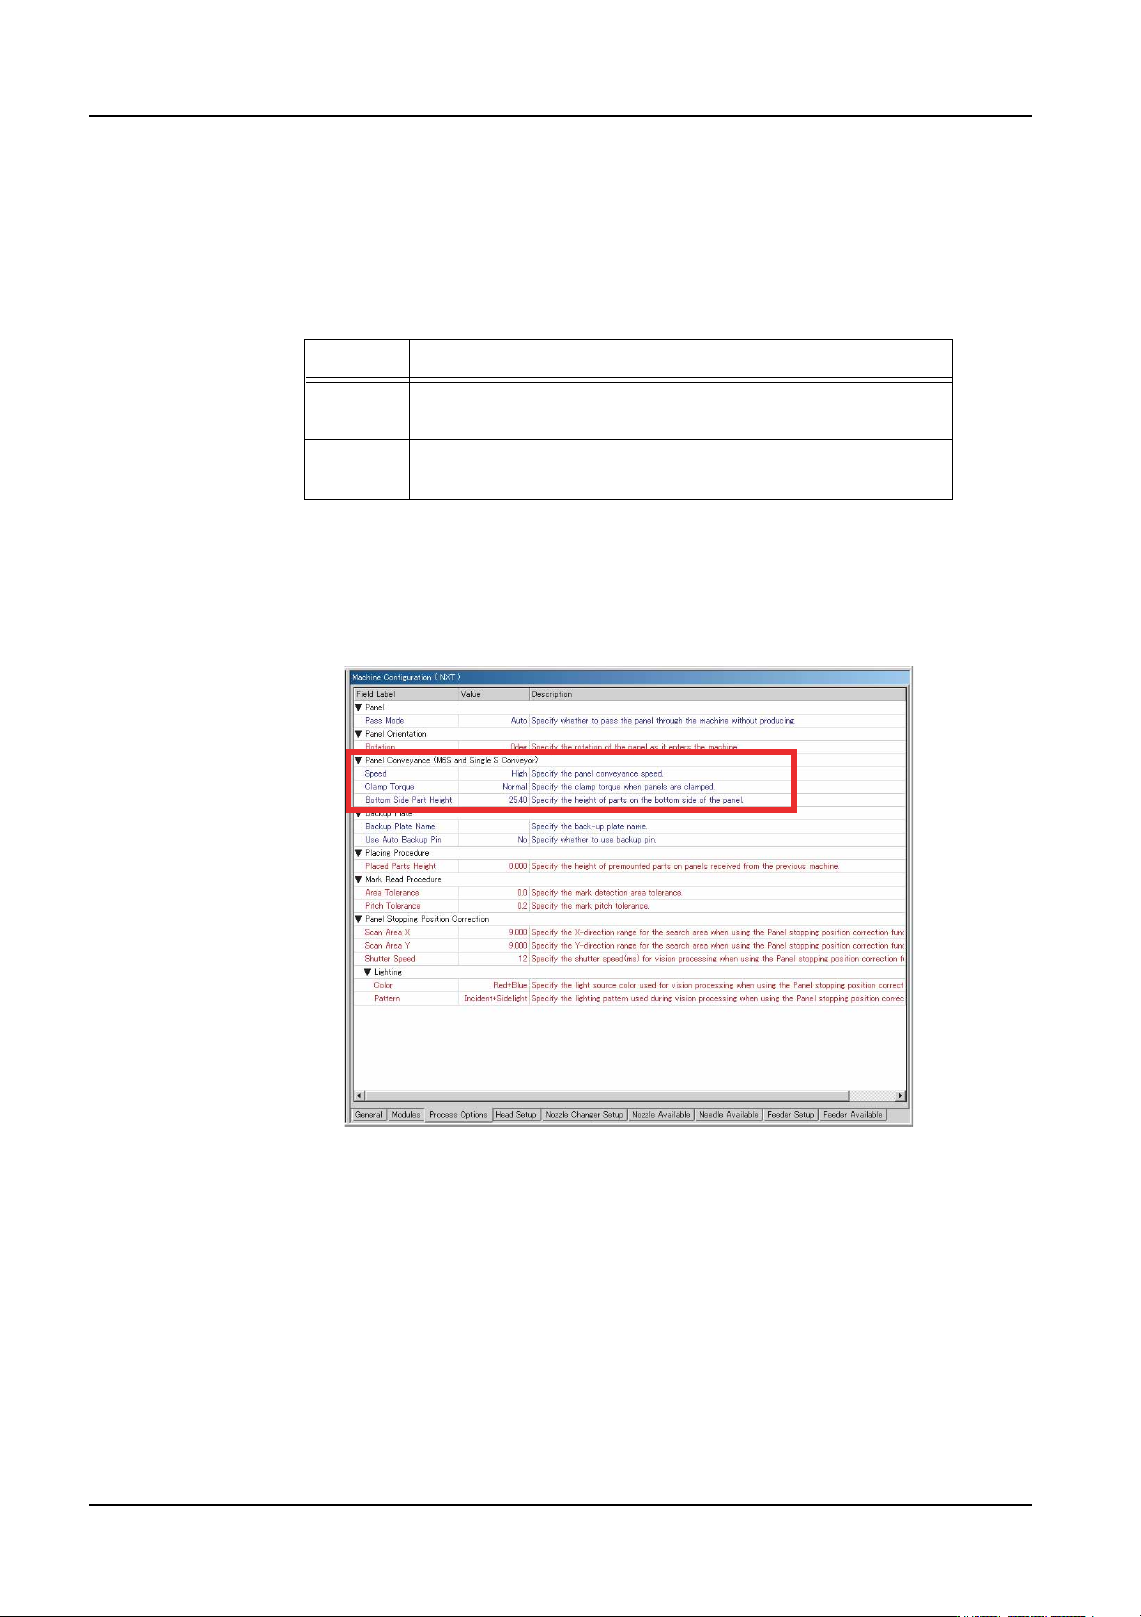
1. Click the [Process Options] tab at the bottom of the Machine Configuration pane.
2. In the [Panel Conveyance (M6S and Single S Conveyor)] section, specify the following
two settings. (The [Speed] setting is not currently used.)
a. [Clamp Torque]
b. [Bottom Side Part Height]
• Enter a value from 0 to 25.4 mm.
Note: If the part height setting is incorrect, back up pins may contact parts on the bottom side of
the panel and damage the panel.
Value Details
Normal This is the default clamp torque setting. Use this setting
when using the insertion pressure control function.
Soft Use this setting when clamping fragile panels, such as
ceramic panels.
01PRG-0051E