FUJI NXT Programming Manual QD004-18.pdf - 第52页
3. Job Builder QD004-18 42 NXT Programming Manual 01PRG-0035 (4) (3) (2) (1) HH
QD004-18 3. Job Builder
NXT Programming Manual 41
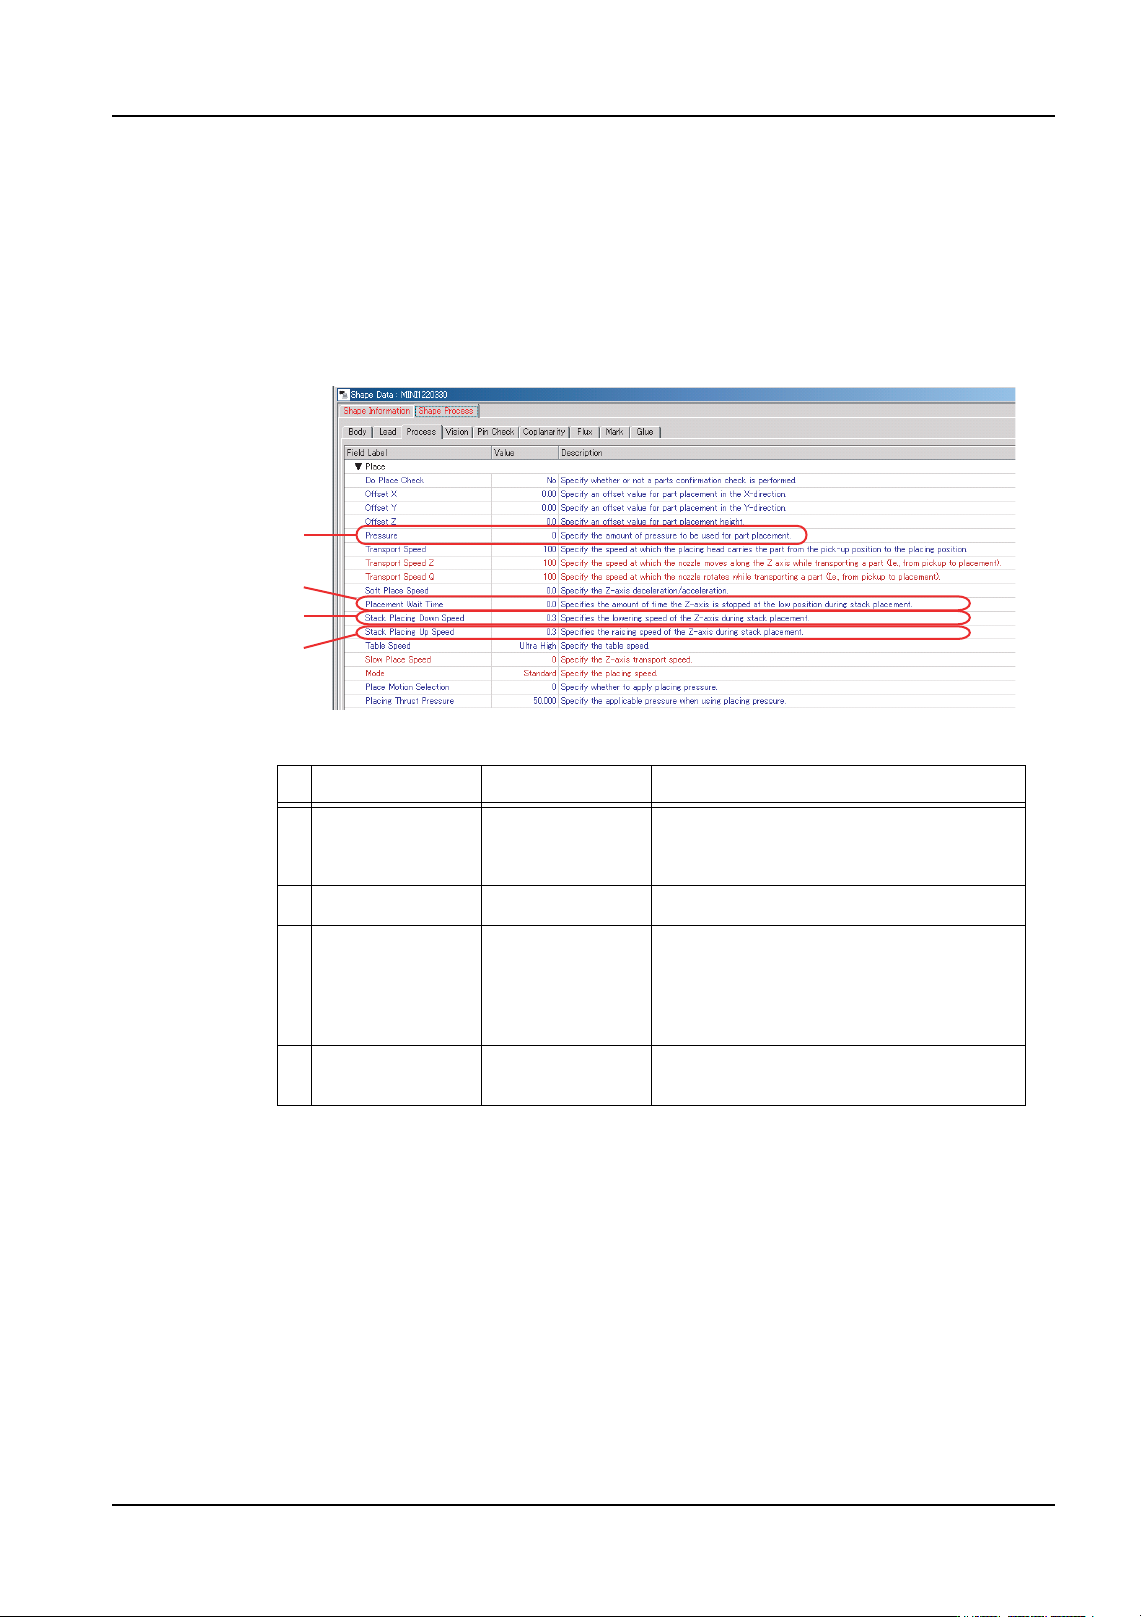
Shape data settings
1. Select the [Shape Data] tab from the job information bar.
2. Double-click the name of the shape data for the part. The shape data settings are
displayed.
3. Select the [Shape Process] tab and then select the [Process] tab.
4. Specify settings for the settings listed below.
*1: If a value greater than “0.3” is specified for [Stack Placing Down Speed], the amount of
pressure exerted on the part when the nozzle is in the lowered position (placing the part)
may exceed the value specified for [Pressure].
*2: In Fuji Flexa, a value from “0” to “5000” can be specified. However, placing is performed
using 220 gf if a value less than 220 gf is specified. Likewise, placing is performed using
1020 gf if a value greater than 1020 gf is specified.
Setting name Setting range Details
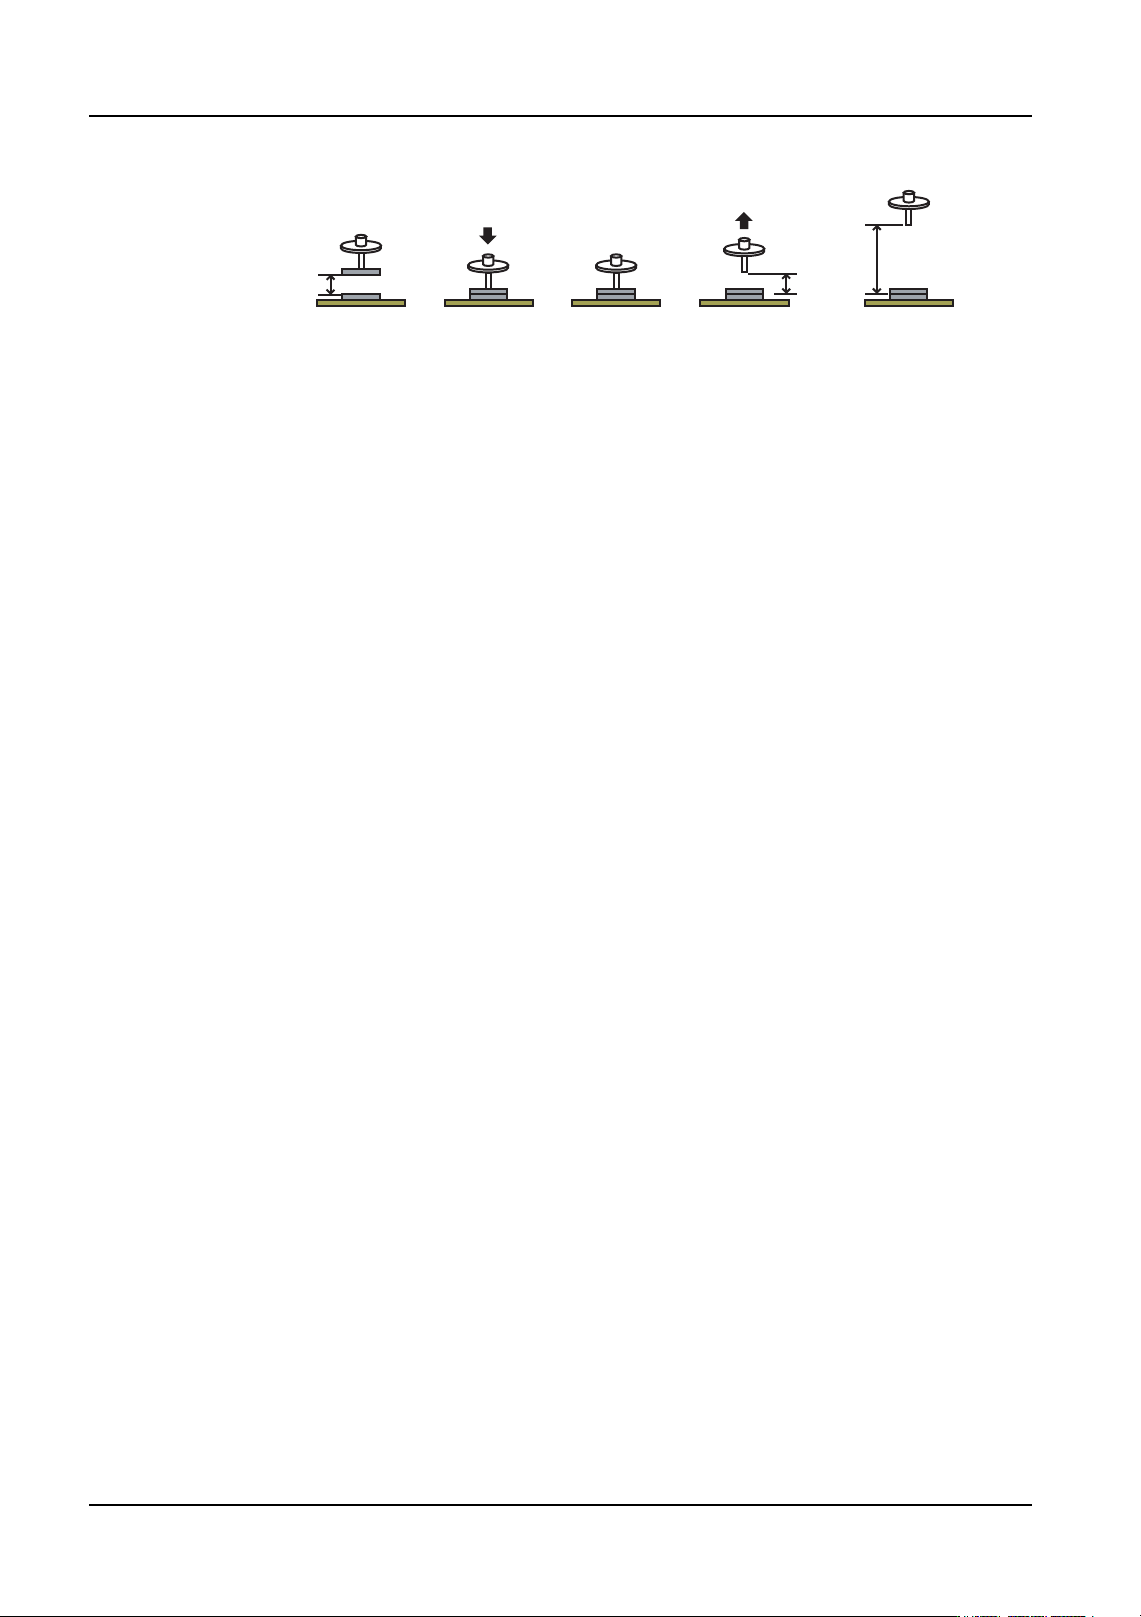
1 Stack Placing
Down Speed
(*1)
0.1 to 10.0 (%) Speed at which the nozzle (Z-axis) is
lowered.
2 Pressure (*2) 220 to 1020 (gf) Pressure used when stacking parts.
3 Placement Wait
Time
0.000 to 20.000
(msec)
Amount of time the machine pauses
with the nozzle lowered (pushing on the
part on top of the stack). If “0” is
specified, the default value for the head
is used.
4 Stack Placing
Up Speed
0.1 to 10.0 (%) Speed at which the nozzle (Z-axis) is
raised.
01PRG-0036E
1
2
3
4
3. Job Builder QD004-18
42 NXT Programming Manual
01PRG-0035
(4)(3)(2)(1)
HH
QD004-18 3. Job Builder
NXT Programming Manual 43
3.4.4 Using the M6S and single conveyor S (from NXT V4.30)
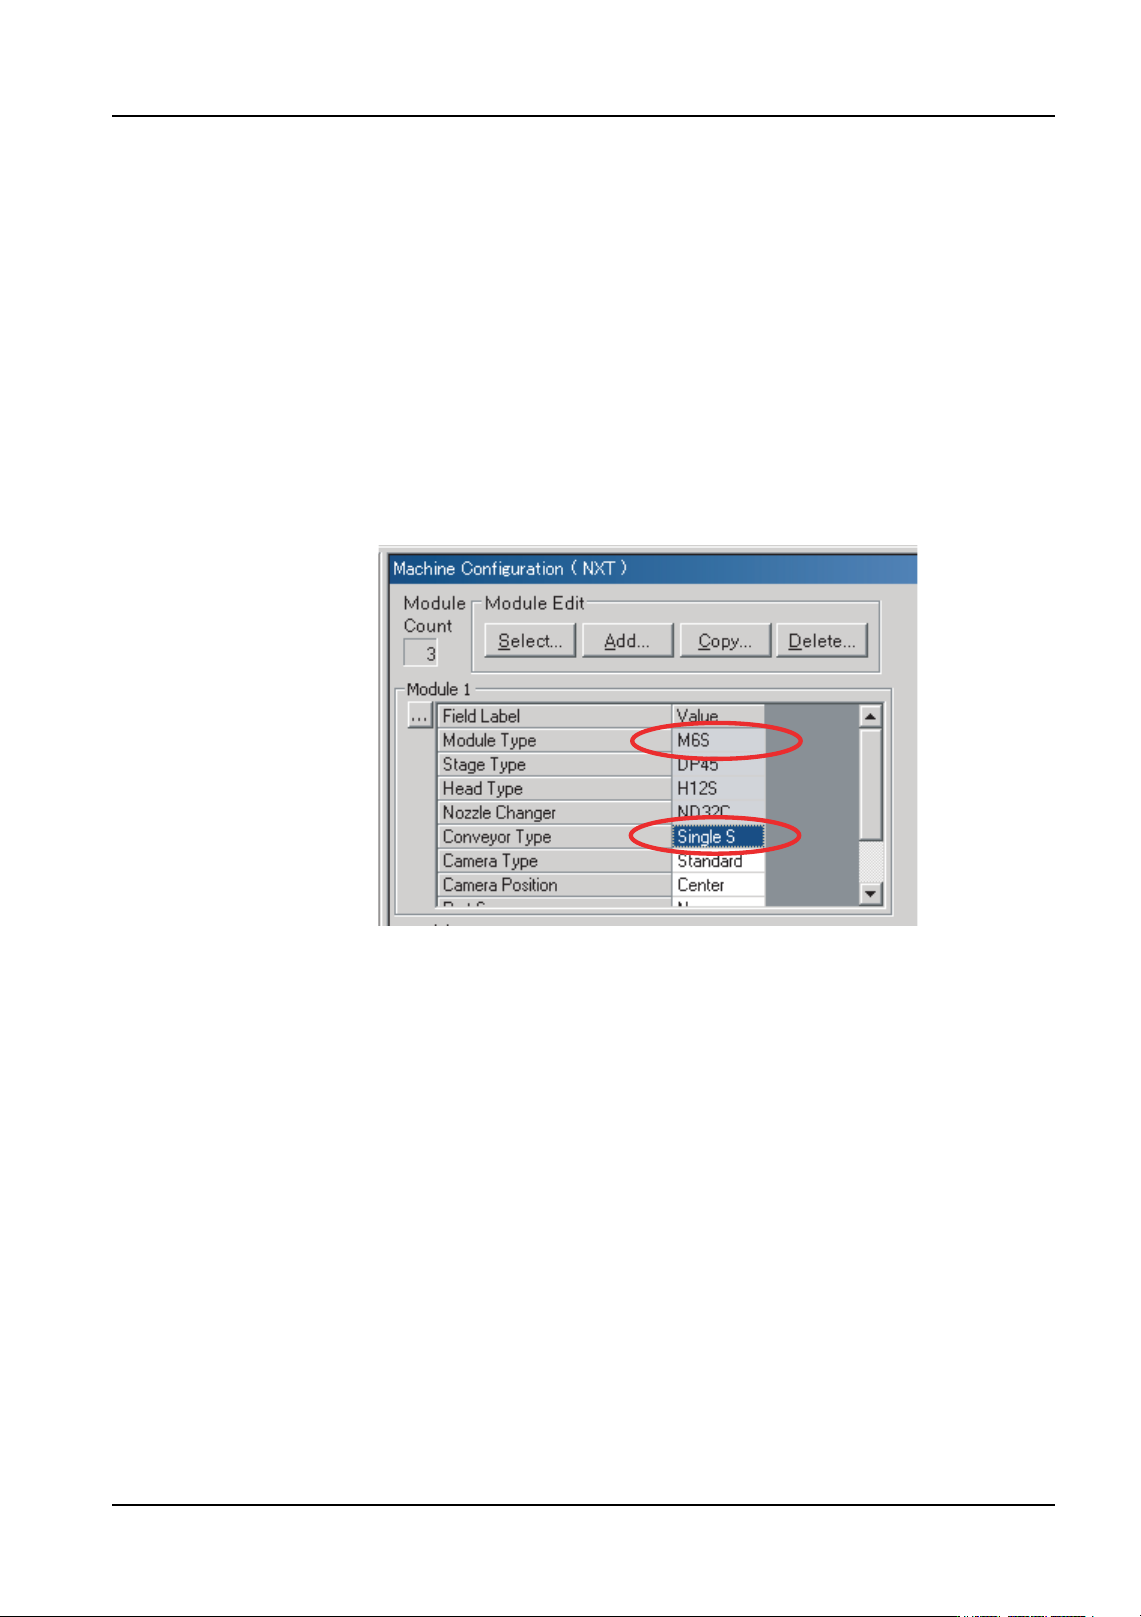
Make the following settings in the job before using a single conveyor S at an M6S module.
Fuji Flexa V3.4.0 or later is required.
Settings
Display the [Machine Configuration] pane of the job in Fuji Flexa (See 3.3.3 "Configuring an
NXT machine" for more details.)
Module configuration
1. Click the [Modules] tab at the bottom of the Machine Configuration pane.
2. Select “M6S” for [Module Type].
3. Select “Single S” for [Conveyor Type].
01PRG-0050E