FUJI NXT Programming Manual QD004-18.pdf - 第200页
6. Editing Jobs on the Machine (MEdit) QD004-18 190 NXT Programming Manual Indexing the tape Check the chart and push the index button the numbe r of times required to index the part forward. Returning the tape Check the…
QD004-18 6. Editing Jobs on the Machine (MEdit)
NXT Programming Manual 189
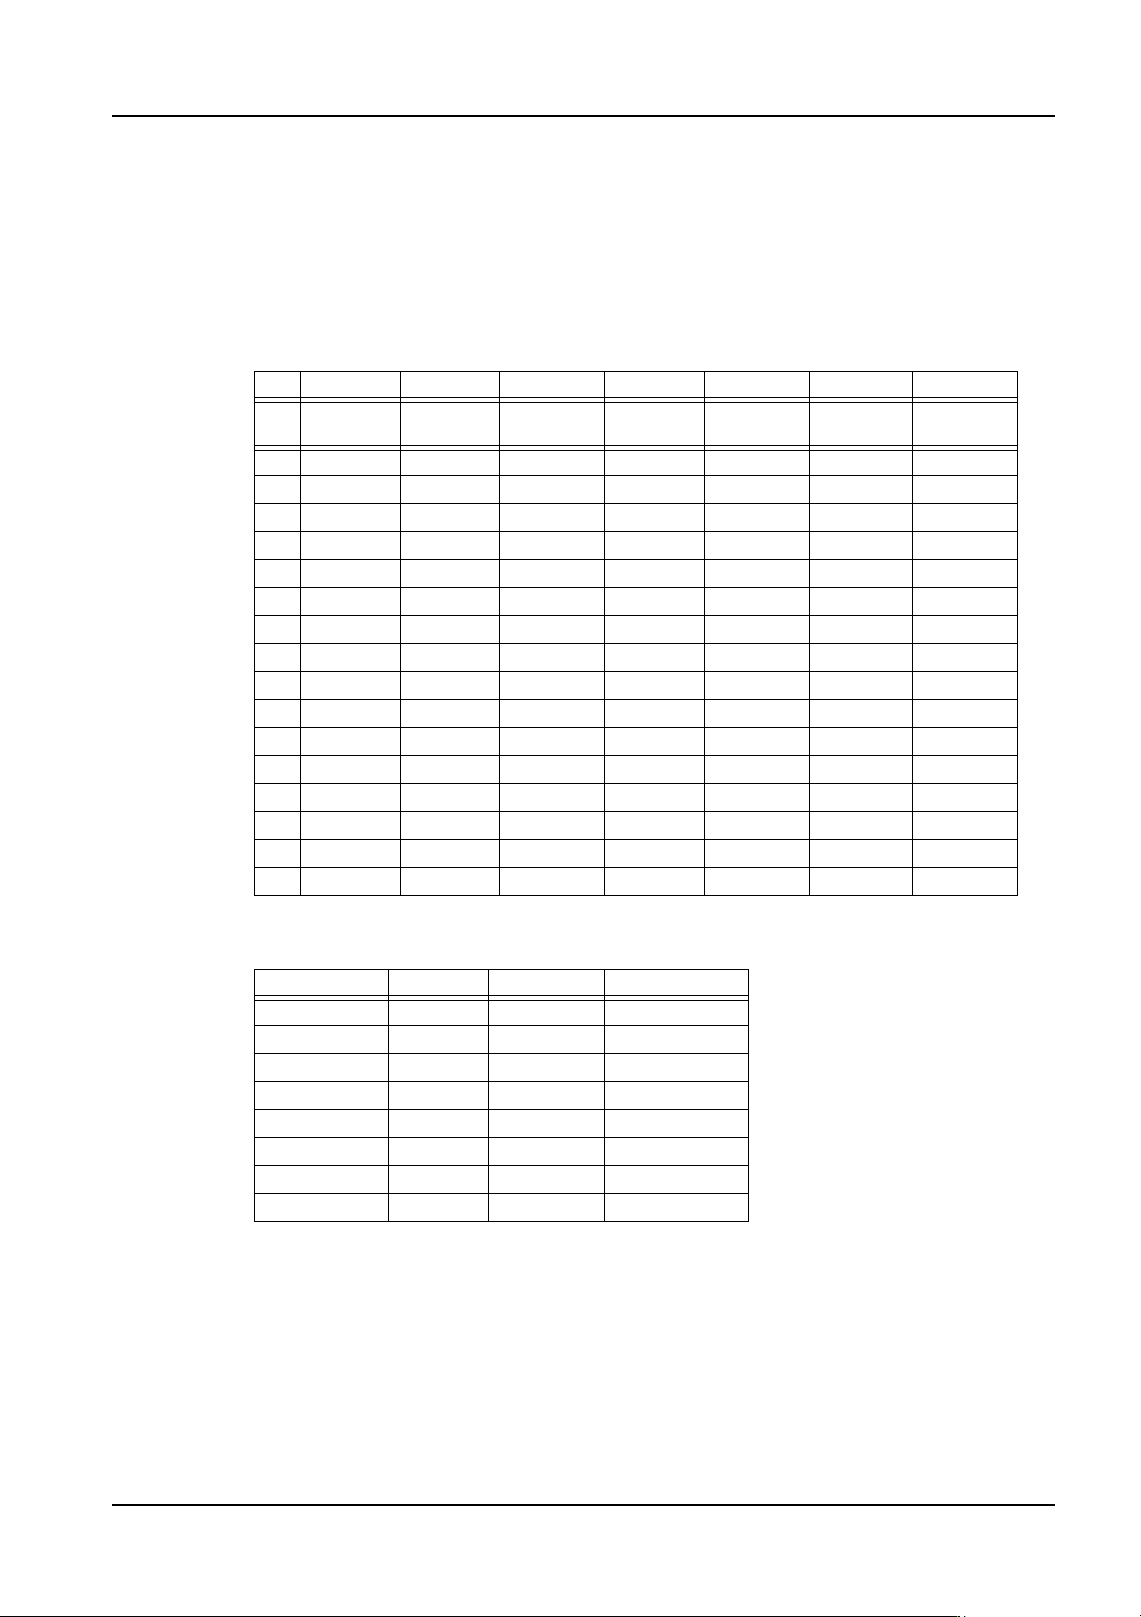
6.8.4 Feeder index count and tape return method for pickup tests
When performing a pickup test, it is necessary to index the parts because the test does not
automatically index them and there are certain cases in which indexing must be performed
a certain number of times, depending on the feeder. The feed count list is shown below.
Index count based upon feeder type and pitch table
Tape Feeders
Stick Feeders
Note: Items in the () indicate that it might be possible to use that amount to index the part for the
pickup test. However, there are times when a Y-axis movement tolerance error occurs and
the pickup test cannot be performed because the pickup position will change based on
calibration compensation or any pickup offset values (part size or smaller) and therefore the
pickup position will be outside the valid movement range.
W08 W12 W16 W24 W32 W44 W56
Pitc
h
Index
amount
Index
amount
Index
amount
Index
amount
Index
amount
Index
amount
Index
amount
11 X X X X X X
21 X X X X X X
4 1 3 (1) 3 (1) 4 4 4 4
8 2 (1) 2 (1) 3 3 3 3
12 2 (1) 2 (1) 2 (1) 2 (1) 2 (1) 2 (1)
16 2 (1) 2 (1) 2 (1) 2 (1)
20 2 (1) 2 (1) 2 (1) 2 (1)
24 2 (1) 2 (1) 2 (1) 2 (1)
28 (1) (1) (1)
32 (1) (1) (1)
36 (1) (1)
40 (1) (1)
44 (1)
48 (1)
52 (1)
56 (1)
Feeder Width Type Chute Type Index Amount
24 mm 1S Top (1)
24 mm 1S Bottom X
24 mm 1L Top X
24 mm 1L Bottom X
48 mm 2S Top (1)
48 mm 2S Bottom X
48 mm 2L Top X
48 mm 2L Bottom X
6. Editing Jobs on the Machine (MEdit) QD004-18
190 NXT Programming Manual
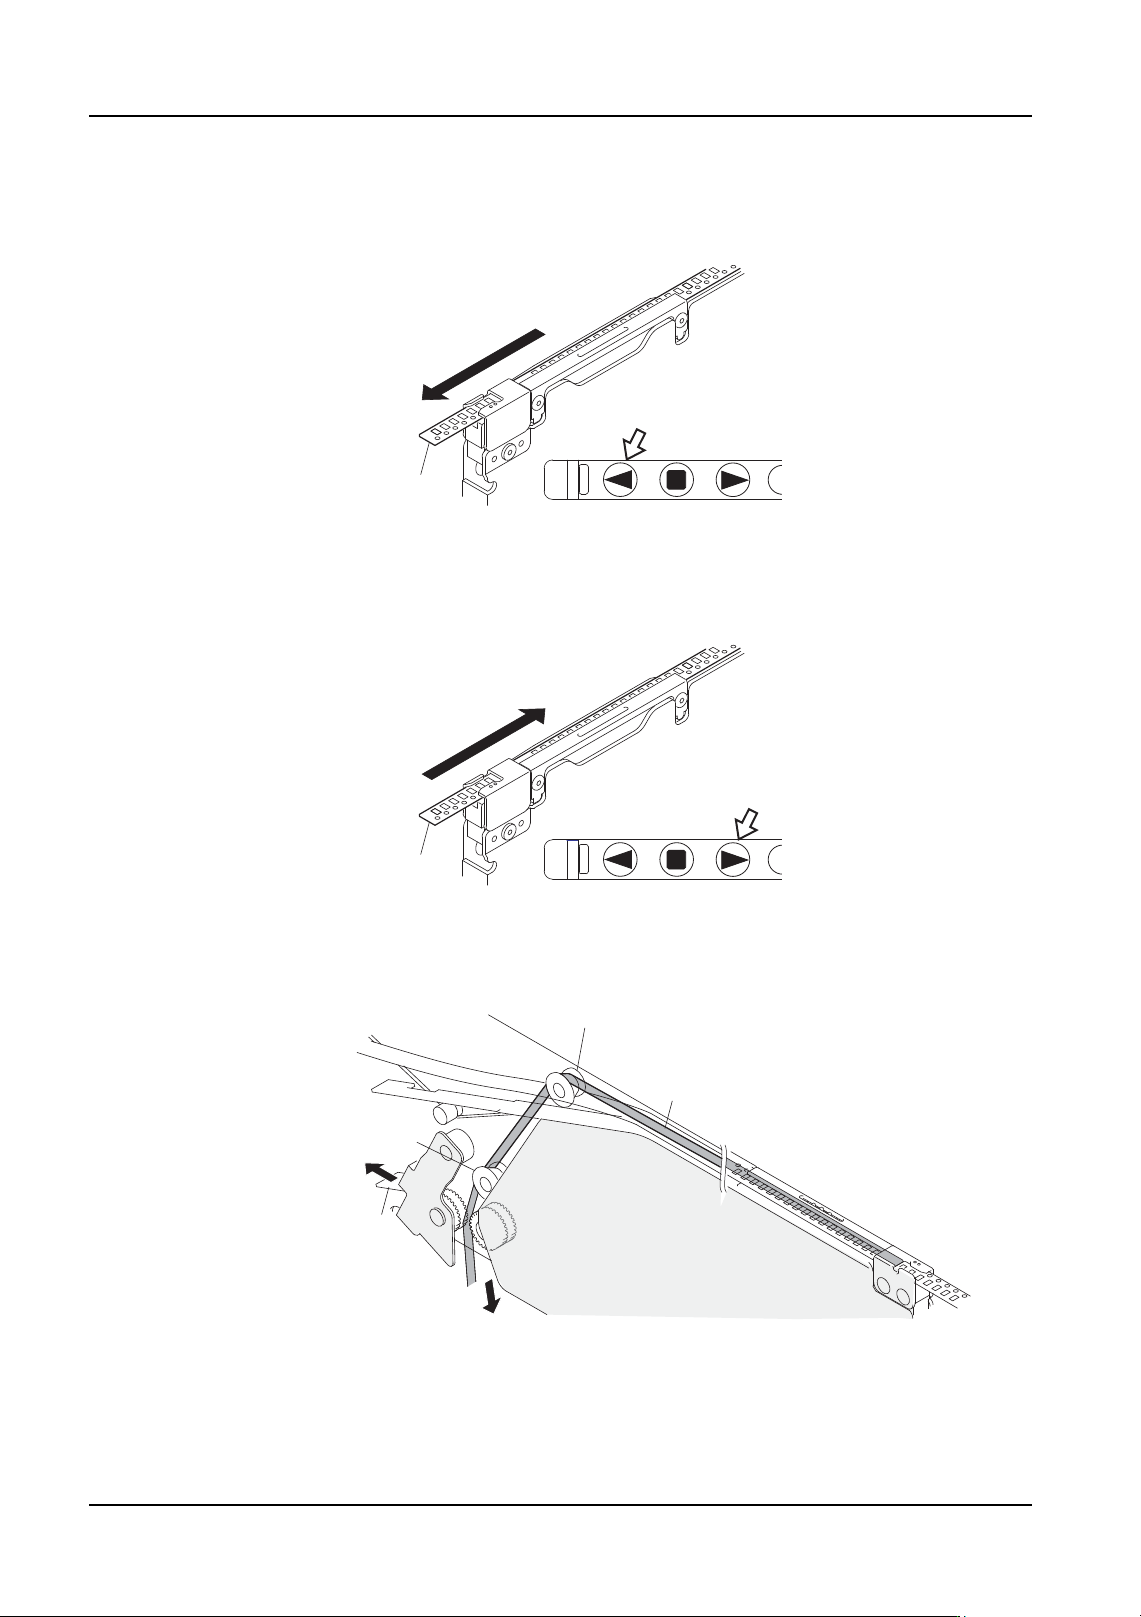
Indexing the tape
Check the chart and push the index button the number of times required to index the part
forward.
Returning the tape
Check the part and index the part back the number of times it was indexed forward by
pushing the back button the same number of times.
Note: The take-up lever is designed to prevent looseness in the top film when rotated correctly
(i.e., the tape is indexed forward). When rotated in the opposite direction, looseness in the
top film develops. Eliminate this looseness manually by opening the take-up lever and
gently pulling on the top film and then returning the take-up lever.
Carrier tape
ERR
PWR
1
2
4
NXTFDR006
Carrier tape
ERR
PWR
1
2
4
NXTFDR181
Top film
Take-up lever
Roller (upper side)
Roller (lower side)
NXTFDR008
QD004-18 6. Editing Jobs on the Machine (MEdit)
NXT Programming Manual 191
6.9 Testing Vision Processing (from NXT V4.10: H01
head and OF head)
The vision processing test function is used to perform the following procedures.
• Adjust the vision processing height at the machine (for the side light camera).
• Check vision processing results.
• Check and edit the job.
Caution: Perform a pickup test to determine the correct pickup position before performing a vision
processing test.
Restrictions
• Only original slots can be selected for a vision processing test.
• It is possible to begin a vision processing test even if all of the nozzles that are
specified in the job are not set in the nozzle station. Nozzles that are not
specified in the job are used. As a result, the nozzles used when performing
automatic operation and the nozzles used when performing the vision
processing test may differ.
• The parts used when testing vision processing are not included in the used parts
count. As a result, there will be a discrepancy in the remaining parts count in
Fujitrax Verifier.
• When the claw is being used, even if the pickup position XY is incorrect, an
offset may be used when the part is picked up. In such a case, if the part that
was picked up is returned to the tray, the part may not fit properly into the tray
cavity. For this reason, the pickup test should be performed and pickup XY
position adjusted before performing a vision processing test.