FUJI NXT Programming Manual QD004-18.pdf - 第32页
3. Job Builder QD004-18 22 NXT Programming Manual Specifying NXT machin e processing options Data about the processing of the job for the NXT machine must be entered. When a machine with a certain name is a dded for the …
QD004-18 3. Job Builder
NXT Programming Manual 21
12.Repeat the previous steps, while selecting the next module in the machine until all of the
modules in the machine have the correct configuration.
13.If any pairs of M3 modules are to perform paired production, display the modules and
change the setting [Perform Paired Module Production] to “Yes” for both modules.
Specify any required stopping position offset. Repeat until all M3 modules that are to
perform paired module production have the correct setting.
Note: Paired module production is when two M3 modules clamp a single panel across the
conveyors for the modules and place parts on the same panel. Paired production can only
be performed between set pairs of M3 modules.
14.If the created module configuration is the standard setup for the selected NXT machine,
right-click the grey area outside of the setting area in the [Modules] tab and select [Save
as the Default Machine Configuration] to save the current module configuration as the
standard configuration. When the same machine is brought into a job from this point,
the module configuration will be the same as that just specified.
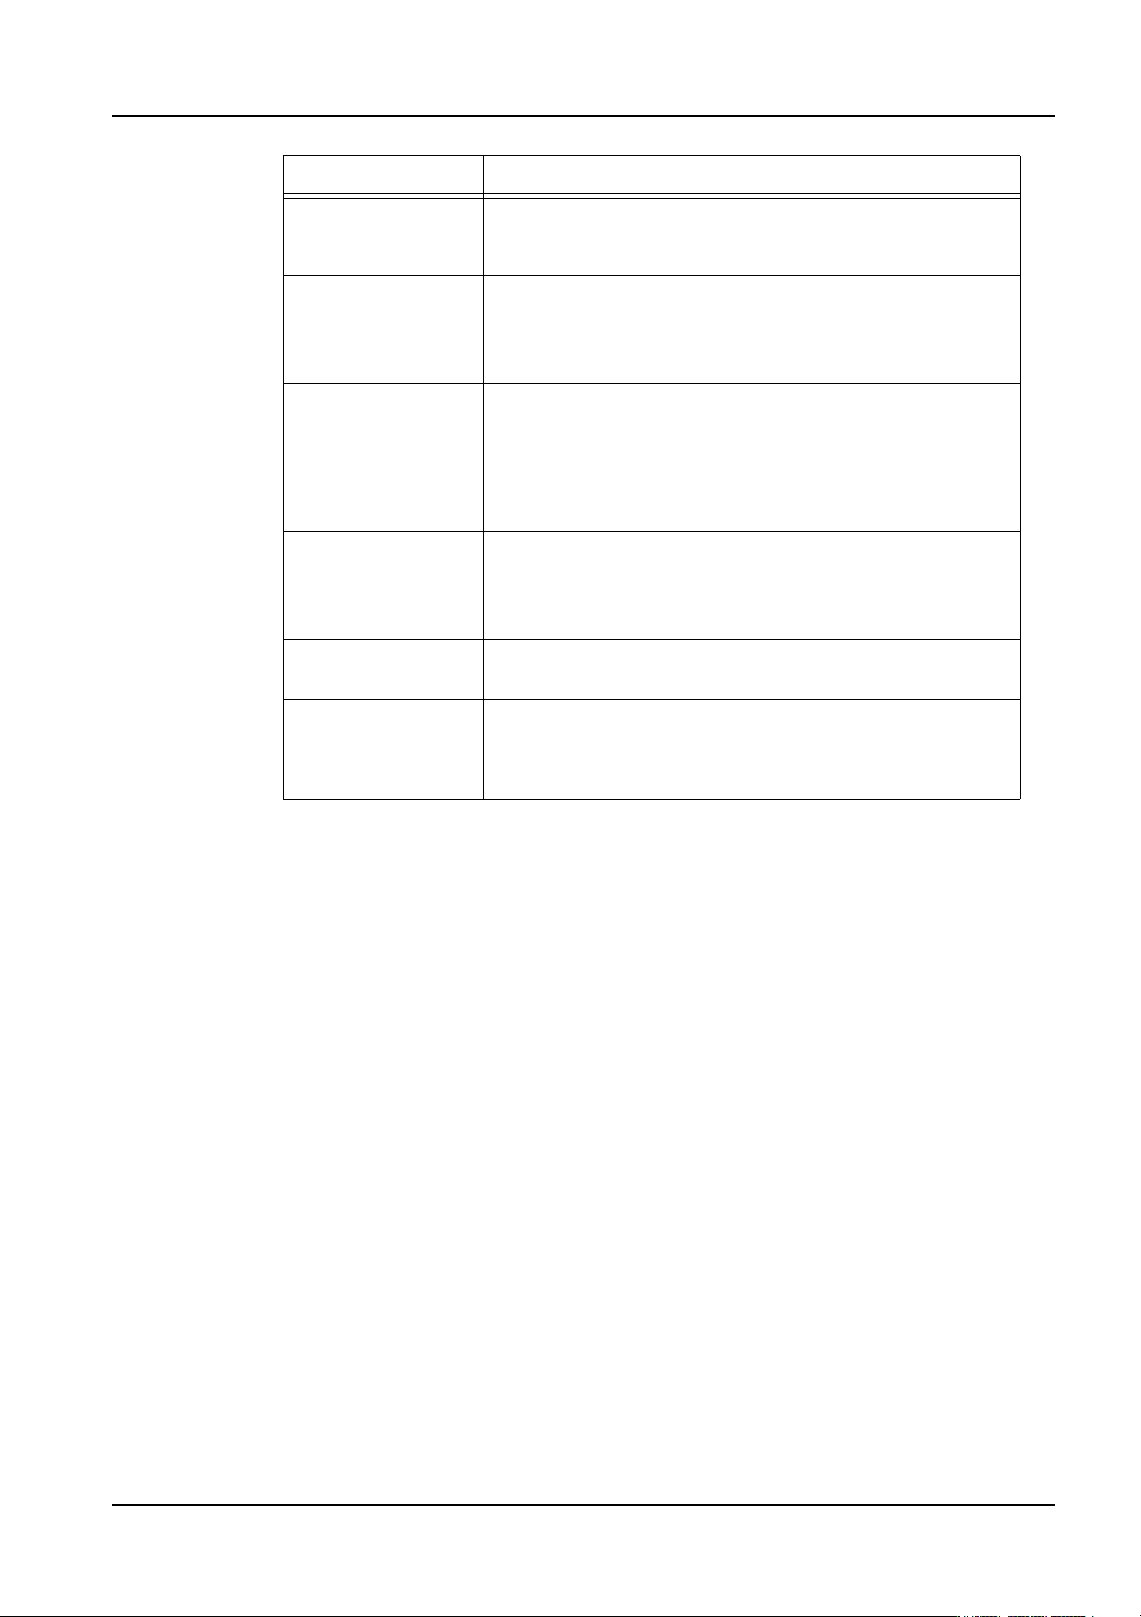
Camera Position This setting only displays when for M6 modules and is
used to specify the position of the camera. Only if a M6 has
a feeder pallet is this setting valid.
Part Sensor Specify whether a part presence check sensor is installed.
No: There is no parts sensor
Yes: A parts sensor is present
Part Sensor Type Specify the type of sensor to check for the presence of
parts.
-Sensor: A sensor is used to check.
-IPS: IPS is used to check for the presence of parts as
well as the part height.
Calibration Unit Specify whether a unit to check the nozzle load is installed.
No: There is no calibration unit
Yes: A calibration unit is present
Coplanarity This specifies whether or not the module is equipped with
coplanarity measuring unit. This is a NXT option.
Actual Cycle Time
Difference
Make a setting here when a difference between the
projected cycle time and actual production cycle time
exists for the module. Specify the difference between
these two cycle times.
Setting Description
3. Job Builder QD004-18
22 NXT Programming Manual
Specifying NXT machine processing options
Data about the processing of the job for the NXT machine must be entered. When a
machine with a certain name is added for the first time, the default process options are
used. This data must be checked and edited if it is not the correct processing options for
that machine.
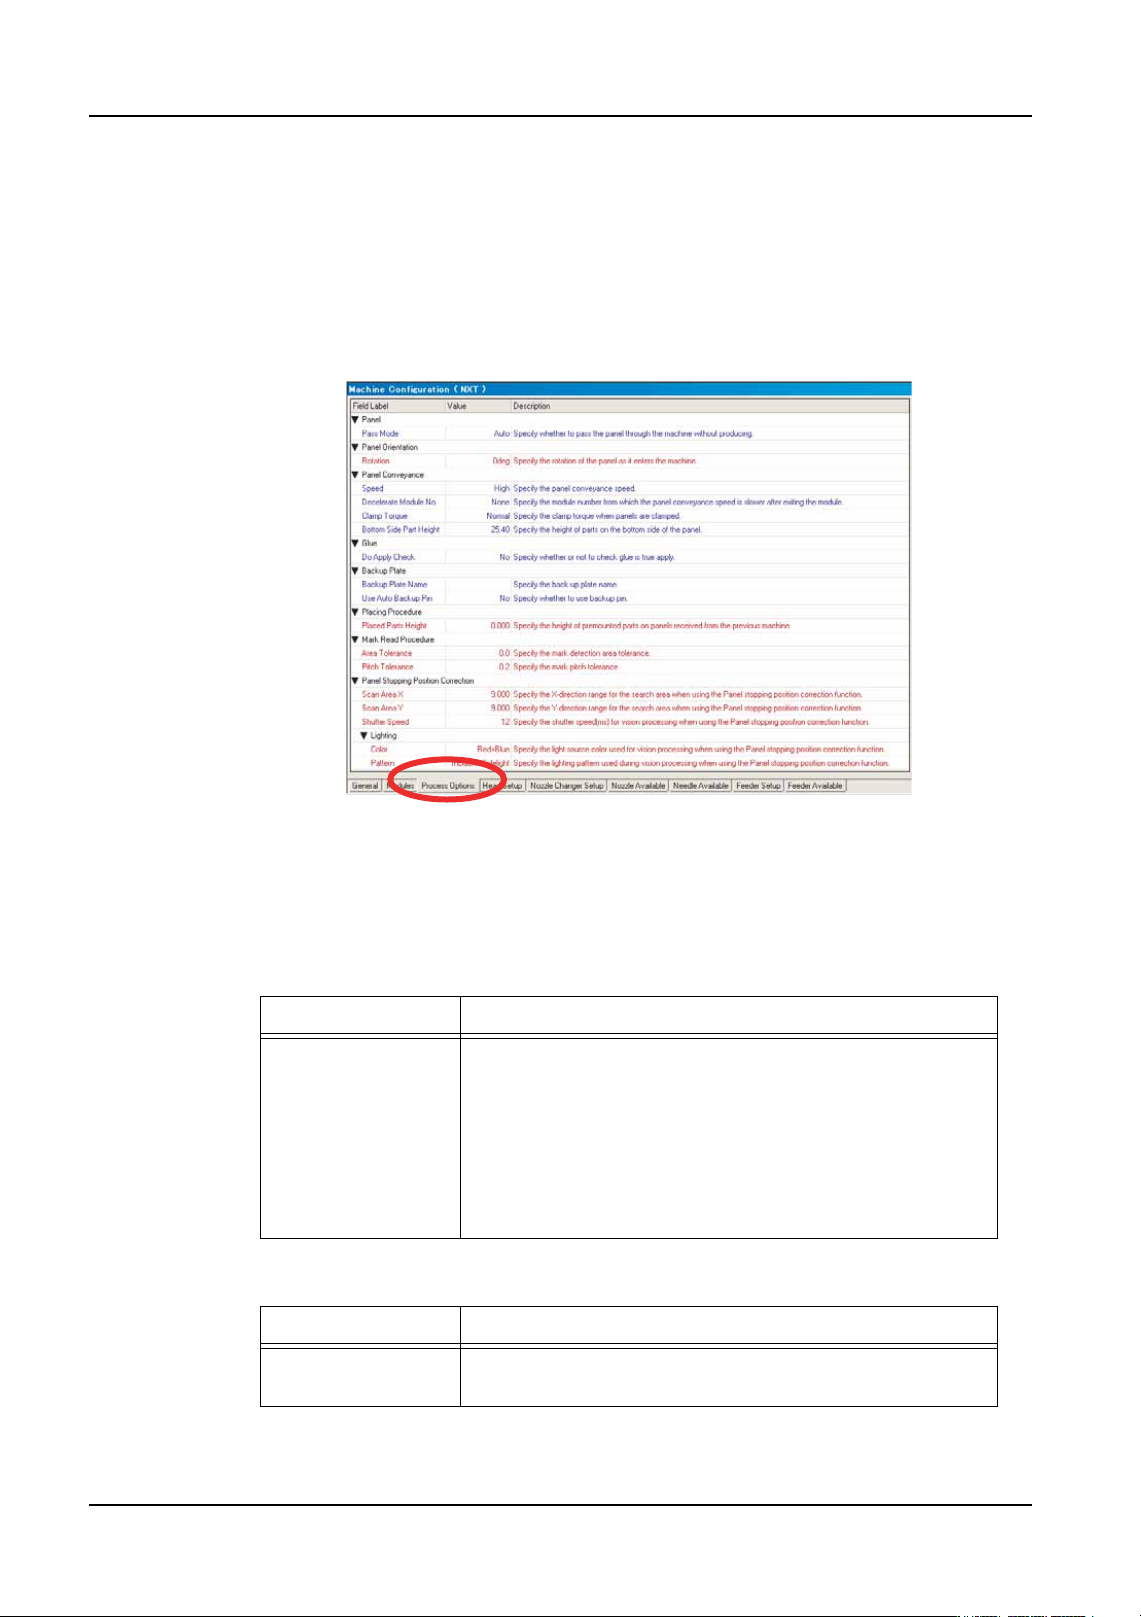
1. There are several tabs at the bottom of the [Machine Configuration] pane. Select the
[Process Options] tab to display the available process options for the machine
2. Enter the appropriate process settings for the machine. There are multiple groupings of
data. Refer to the tables below for information on the settings. More information on
special settings that relate to options can be found in the appropriate “Job Settings for
Advanced Functions” section.
Panel
Panel Orientation
Setting Description
Pass Mode Specify whether the machine should operate in pass
mode. When operating in pass mode the machine does
not produce any boards, and acts instead as a conveyor.
On: Operate using pass mode
Off: Normal production is performed.
Auto: The pass mode decision is made automatically
based on part allocation.
Setting Description
Rotation Specify the orientation of the panel as it enters the
machine.
01PRG-0055Ea
QD004-18 3. Job Builder
NXT Programming Manual 23
Panel Conveyance
Glue
Backup Plate
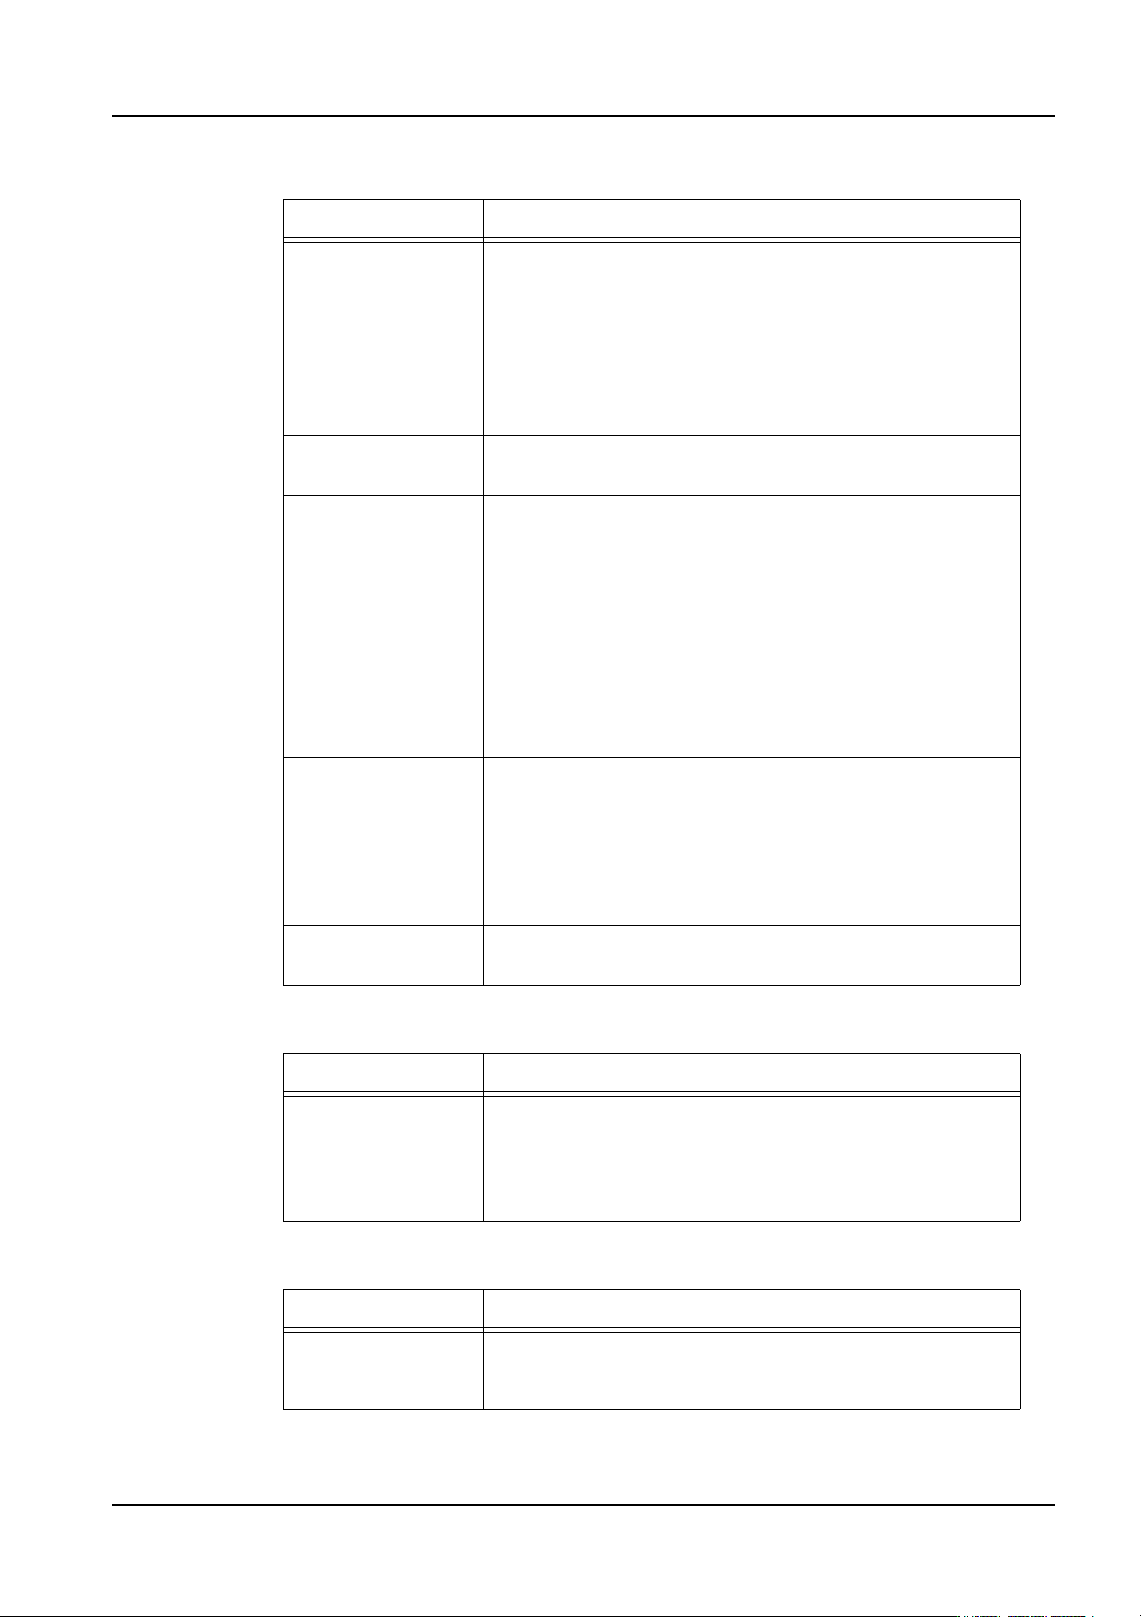
Setting Description
Speed Specify the panel conveyance speed.
High: This speed can convey panels with standard parts in
a stable manner.
Middle: This conveys panels at 70% of the high speed.
Low: This conveys panels at 50% of the high speed.
ULow: This conveys panels at 30% of the high speed.
Decelerate Module
No.
Specify the module number from which the panel
conveyance speed is slower after exiting the module.
Speed After
Decelerate
Specify the panel conveyance speed for panels after they
exit the module from which the slower conveyance was
specified. This must be a slower setting than that specified
in [Speed].
Middle: This conveys panels at the same speed as the
Middle setting for Speed.
Low: This conveys panels at the same speed as the Low
setting for Speed.
ULow: This conveys panels at the same speed as the
ULow setting for Speed.
Clamp Torque Specify the clamp torque when panels are clamped. This
is only applicable for conveyors that use motors to clamp
the panel, such as the single conveyor S.
Normal: Normal torque
Soft: Light torque (Used when placing parts on fragile
panels.)
Bottom Side Part
Height
Specify the height of parts on the bottom side of the panel.
The transport speed can be increased for shorter parts.
Setting Description
Do Apply Check Specify whether or not to glue check sequences are
applied to check the glue condition.
Yes: Place glue check sequences and check
No: Do not check
Setting Description
Backup Plate Name Specify the back-up plate name. This is optional and is
used to indicate a specific backup plate when performing
changeover.