00195982-03_SM_SWS_EN.pdf - 第378页
15 Calibration 15.3 Calibration die handling - flip unit 378 Service Manual SIPLACE Wafer System (SWS) 11/2018 Fig.544: ● The Z axis is moved up until the the time-out when the bearing touches a segment. ● This value is…
15 Calibration
15.3 Calibration die handling - flip unit
Service Manual SIPLACE Wafer System (SWS) 11/2018 377
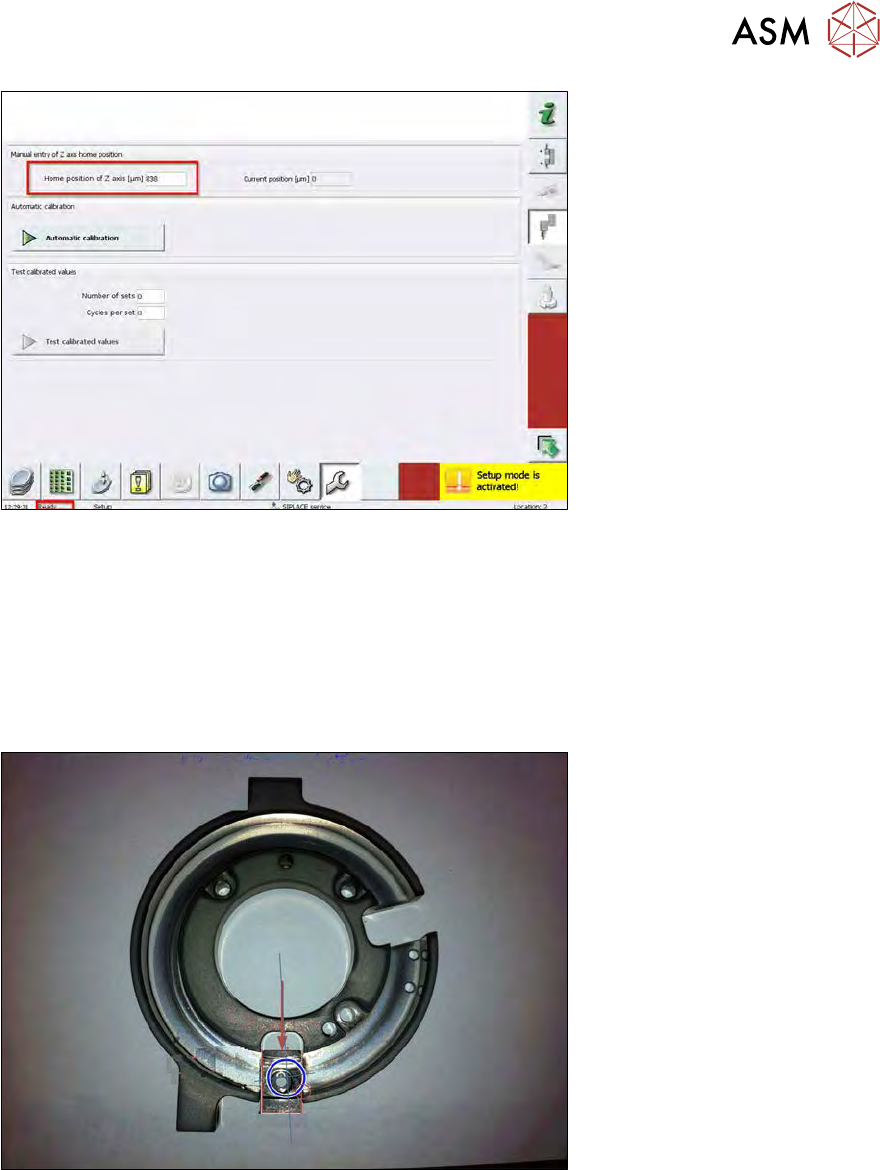
Fig.542:
► After successful automatic calibration of the Z axis, the status changes to Ready.
► The calibrated Z axis zero point correction value is shown at Home position of Z axis (µm).
How Automatic calibration for the flip head Z axis works
●
The Z axis holding cylinder is used as the start home position for the Z axis.
●
The flip rotation axis is moved to the home position.
●
The flip head rotation axis is rotated to the right by a defined value.
Fig.543:
●
The Z axis is moved down until the the time-out when the bearing touches a segment.
●
This Z value is saved.
15 Calibration
15.3 Calibration die handling - flip unit
378 Service Manual SIPLACE Wafer System (SWS) 11/2018
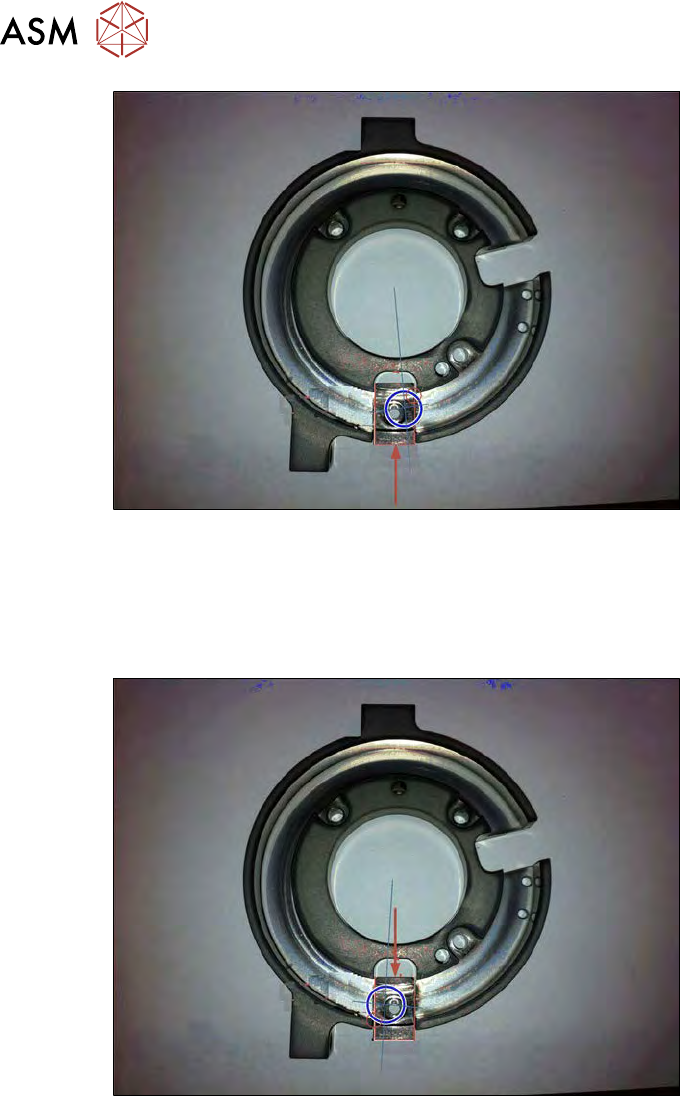
Fig.544:
●
The Z axis is moved up until the the time-out when the bearing touches a segment.
●
This value is saved.
●
From these two values, the home position for the Z axis is calculated (average value).
●
The flip head rotation axis is rotated to the left by a defined value.
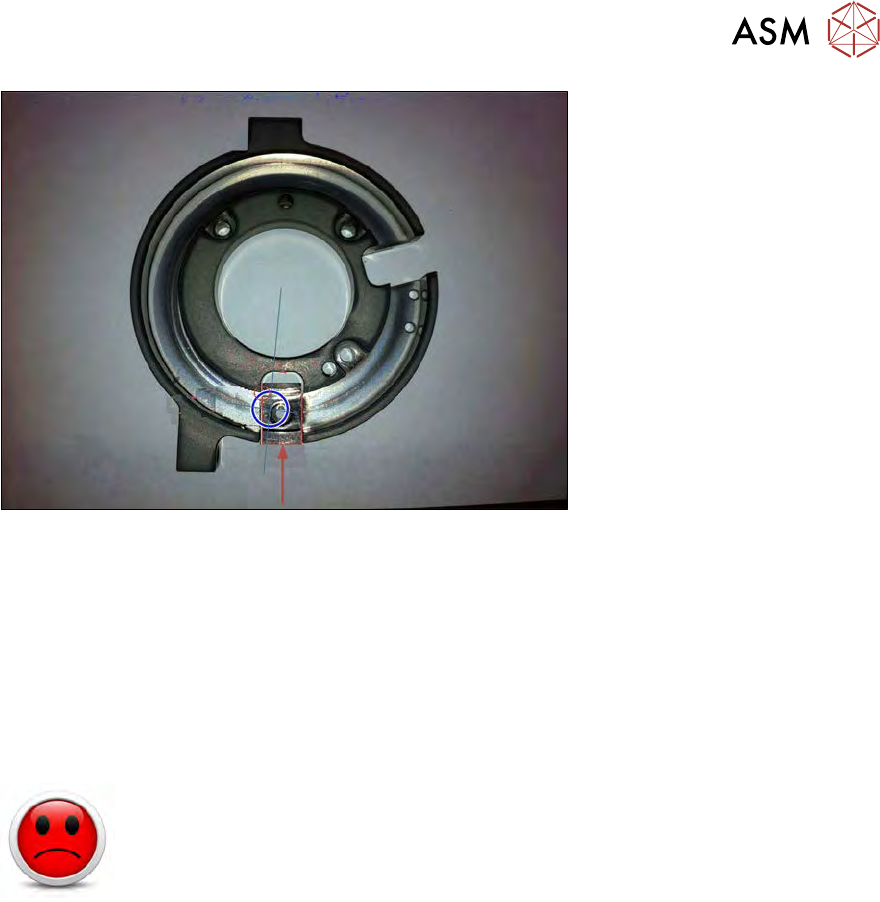
Fig.545:
●
The Z axis is moved down until the the time-out when the bearing touches a segment.
●
This Z value is saved.
15 Calibration
15.3 Calibration die handling - flip unit
Service Manual SIPLACE Wafer System (SWS) 11/2018 379
Fig.546:
●
The Z axis is moved up until the the time-out when the bearing touches a segment.
●
This value is saved.
●
From these two values, the home position for the Z axis is calculated (average value).
●
Based on this four detected values, the exact mean value for Z axis zero point correction can
be calculated.
●
The Z axis zero point is now exactly in the center of the raceway!
15.3.2.4 Calibration – segment offset calibration in X direction
HIGH RISK OF SERIOUS INJURIES
► Setup mode must be activated!
Tools required
●
Teflon tape (local source → plumbing workers / hardware store) → no ASM part number
●
Nozzle 906 or equal nozzles with a sharp tip (2x nozzles required for each segment)
Procedure
This calibration detects and compensates for the offset between segment 1 and segment 2 in X dir-
ection.
Ejector needle, camera center (red cross in vision view) and both segment centers should be in
one point!
With the following calibration procedure, only the software correction in X direction (rotation of the
flip head) can be done!
Should your segments also show a significant offset in Y direction, a mechanical adjustment might
be necessary. Sometimes it helps to turn the nozzle on the related segment by 180° (some nozzles
can have tolerances in X or Y up to 70µm). If the offset in Y direction cannot be improved in that
way, please contact your local service partner for further assistance.
► Manually place the nozzles on the segments (nozzle type 906 in the example).