semi合集-English.pdf - 第6290页
SEMI G58-94 © SEMI 1994 5 8.1.3.3 Ext ernal Lead Plating (if appl i c able) 8.1.3.3.1 Thicknes s — Shall be measure d b y X-ray fluorescence. 8.1.3.3.2 Solderability — Shall be tested p er MIL- STD-883, Meth od 2003. 8.2…
SEMI G58-94 © SEMI 1994 4
7.3.3 Voids — 0.005" (0.127 mm) maximum
allowable dimension with no more than four allowed
and a minimum separation of 0.030" (0.762 mm)
between sites.
7.4 Leadframe
7.4.1 Lead Bond Areas — the minimum lead bond
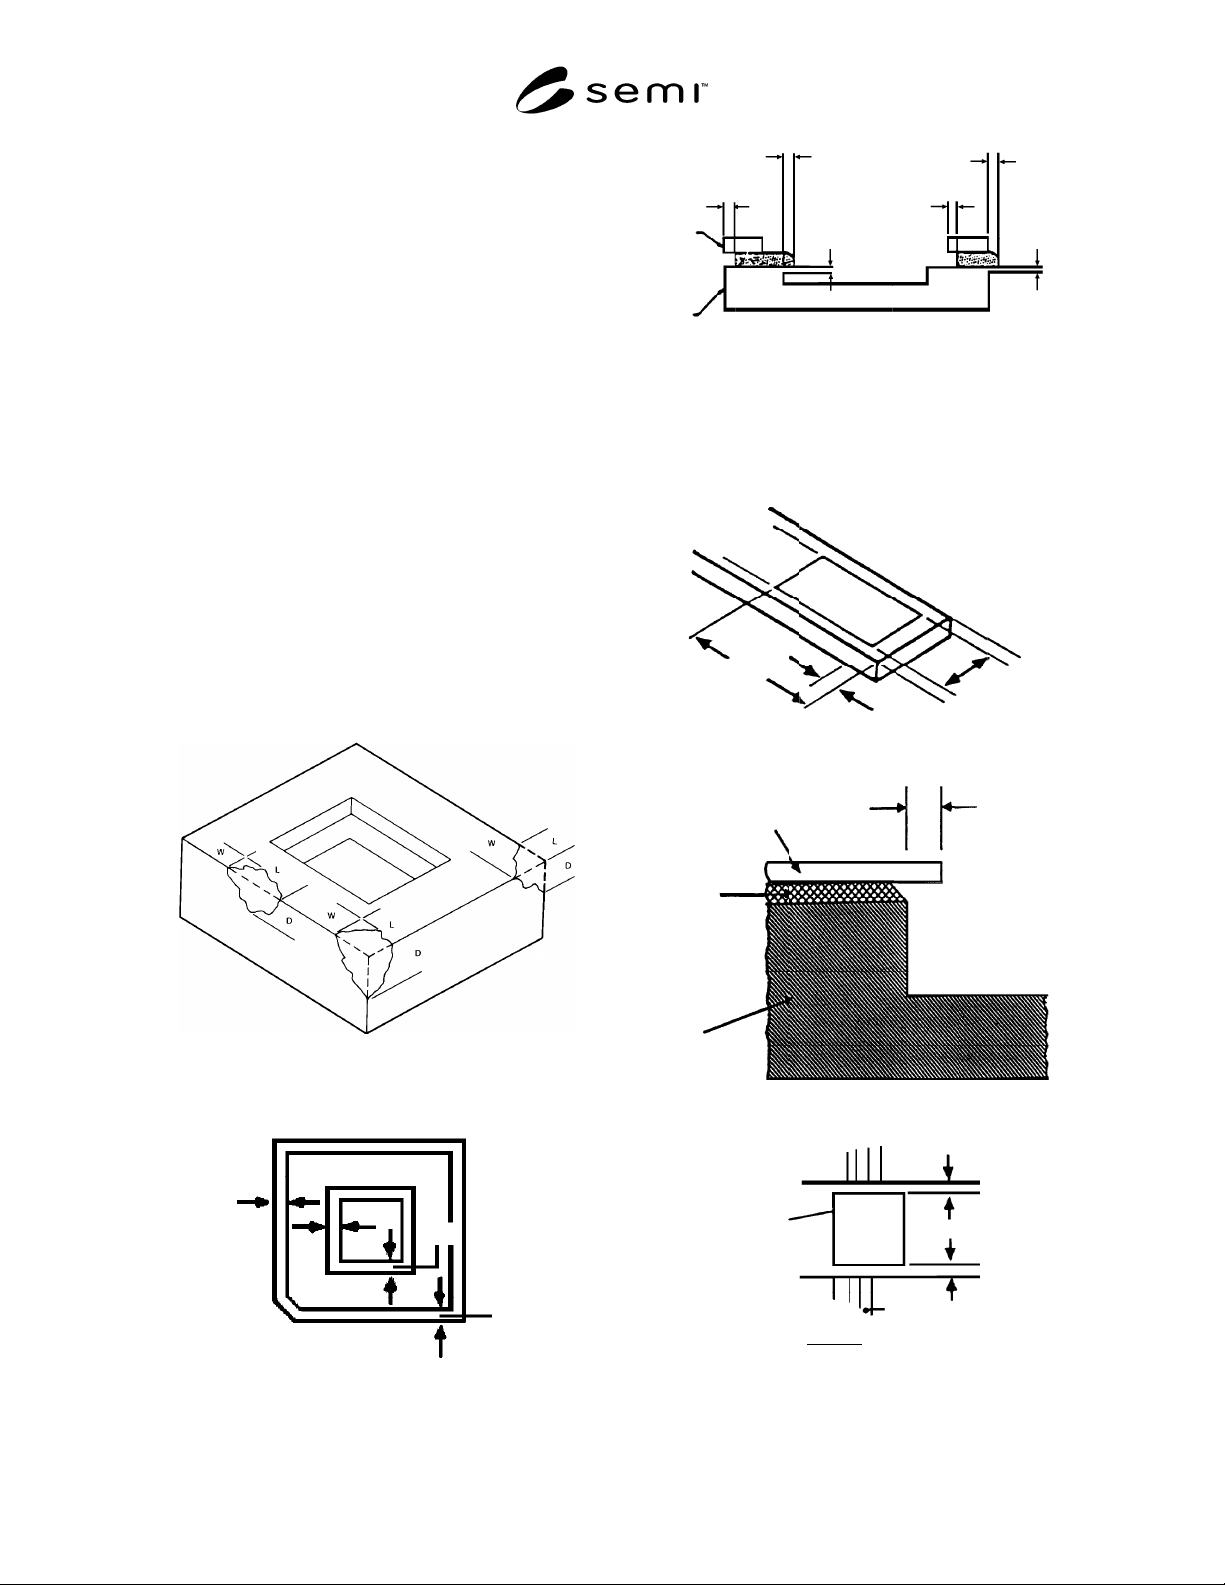
area on the lead tip is defined in Figure 4.
In these bond areas, the following defects are not
allowed:
7.4.1.1 Voids or Pits — Exposure of base material
with any dimension larger than 0.001" (0.0254 mm).
7.4.1.2 Discoloration, Blistering, or Peeling of the
Metallization
7.4.1.3 Scratches or Scrapes — Any build-up of the
metallization, or exposure of the base material.
7.4.1.4 Foreign Material including Glass Splatter or
Projections — No more than four sites, each with a
maximum dimension of 0.001" (0.0254 mm).
7.4.1.5 Glass Wetting or Cracking — Any lead finger
which is not firmly embedded in the glass.
7.4.1.6 Glass Pullback from the Lead Tip — Greater
than 0.010" (0.254 mm).
7.4.1.7 Glass Bulge between Lead Fingers — Greater
than 0.005" (0.127 mm) height above the fingers except
as agreed between vendor and customer for narrow
pitch leads where this limit may cause wire bond
interference problems.
7.4.1.8 Lead Tip Coplanarity (Pre-assembled Bases,
Leadframes, and Window Frames) — Greater than
0.006" (0.15 mm) difference in the position of the top
surface of the lead from highest lead to lowest lead.
7.4.1.9 Lead Tip Pitch — Greater than ± 0.002" (0.051
mm) variation from true position.
7.4.2 I nternal Lead Areas, excluding Lead Bond Areas
— In these areas, the following defects are not allowed:
7.4.2.1 Burrs and Projections or Pits — With a
maximum dimension greater than 0.002" (0.0508 mm)
in height or depth.
7.4.2.2 Foreign Material (including Plating
Discoloration) — With a major dimension in the
surface plane greater than 0.015" (0.381 mm) or
exceeding 0.002" (0.0508 mm) in height.
7.4.2.3 Voids which Expose Base Metal — With a
major dimension greater than 0.002" (0.0508 mm).
7.4.2.4 Blistering or Peeling of Metallization
7.4.2.5 Scratches and scrapes which cause metal build-
up or expose base material.
7.4.3 External Lead Areas
NOTE 4: Non-functional areas of the leadframe, such as tie-
bars, shall not be subjected to inspection.
7.4.3.1 Unplated Leads
NOTE 5: Plated leads shall also be required to pass these
criteria.
7.4.3.1.1 Scratches — Causing loss of more than 25%
of the leadframe thickness.
7.4.3.1.2 Voids — In violation of Section 7.4.3.1.1 or
loss of more than 10% of the design width of a
leadframe detail.
7.4.3.1.3 Burrs — In excess of 0.002" (0.051 mm) in
height and 0.005" (0.127 mm) in the major dimension.
7.4.3.2 Plated Leads
7.4.3.2.1 Scratches and Scrapes — Exposure of base
material or loss of plating integrity over 5% of the area
of a lead finger.
7.4.3.2.2 Voids — Exposure of base material.
7.4.3.2.3 Blistering or Peeling
7.4.3.2.4 Staining, Foreign Material, or
Contamination — In excess of 5% of the area of a lead
finger.
7.4.4 Lead Assembly
7.4.4.1 Lead Tip Overhang — 0.010" (0.254 mm)
maximum from the cavity wall, see Figure 5.
7.4.4.2 Lead Misalignment — 0.010" (0.254 mm)
maximum, see Figure 6.
7.4.5 Window Assembly Misalignme nt — 0.015"
(0.381 mm) maximum, see Figure 7.
8 Incoming Inspection and Functional Tests
8.1 Incoming Inspection
8.1.1 Dimensional inspection per Section 6.
8.1.2 Visual inspection per Section 7 at 10×
magnification with vertical lighting.
8.1.3 Metallization
8.1.3.1 Die Attach Metallization — Thickness shall be
measured by standard cross-sectioning without
smearing or by X-Ray fluorescence.
8.1.3.2 Lead Bond Metallization — Thickness shall be
measured by X-ray fluorescence.
SEMI G58-94 © SEMI 19945
8.1.3.3 External Lead Plating (if applicable)
8.1.3.3.1 Thickness — Shall be measured by X-ray
fluorescence.
8.1.3.3.2 Solderability — Shall be tested per MIL-
STD-883, Method 2003.
8.2 Functional Testing
NOTE 6: All procedures used to functionally test the
components shall be agreed between user and supplier.
The sequence of functional testing shall be as shown in
Figure 8.
8.2.1 Die Attach
8.2.1.1 Visual Inspection
Eutectic Bonding — Visually inspect the alloy wet-out
after die attach. The minimum wet-out requirement
shall be 100% of the die perimeter.
Silver Glass, Epoxy, or Polyimide Bonding — 100% die
perimeter coverage shall be required.
NOTE 7: 100% coverage for resin bonding is not a function
of package acceptability but is required to standardize die
shear testing. The inability of the resins to wet the surface of
the die attach area due to contamination is cause for rejection.
8.2.1.2 Die Shear Test — Perform destructive testing
per MIL-STD-883, Method 2019.
NOTE 8: This test may also be performed after environmental
testing. In the case of very large die, this test may not be
appropriate to fully evaluate the package. In these cases, die
sizes, agreed between vendor and customer, shall be used.
Alternatively, die pull testing may be used by agreement
between vendor and customer.
8.2.1.3 Radiographic Inspection for Voids — Perform
inspection per MIL-STD-883, Method 2012.
8.2.1.4 Ultrasonic Inspection for Voids, Delamination,
and Cracks — Perform inspection per MIL-STD-883,
Method 2030.
8.2.2 Wire Bond — On wire bonds that meet the
requirements of MIL-STD-883, Method 2010, perform
destructive testing per MIL- STD-883, Method 2011,
Test Condition D. Bonds which cause lifted
metallization from the leadframe fingers shall also be
cause for component rejection.
NOTE 9: This test shall be performed at pre-seal and post-
seal.
8.2.3 Seal
8.2.3.1 Visual Inspection — The glass sealant
appearance and flow shall be visually inspected for
conformance to agreed process criteria.
8.2.3.2 Cap Torque Test — This test shall be
performed per process agreement.
8.2.4 Lead Finish — Type A per MIL-M-38510 if
required.
8.2.5 Hermeticity — This test shall be performed per
MIL-STD-883, Method 1014, Test Condition A or B
and C. The package must maintain hermetic integrity
after each environmental test or sequence of tests.
8.2.6 Environmental Testing — Environmental
evaluation shall include, but not be limited to, the
following tests:
NOTE 10: The sequence of testing and the sample sizes for
each sub-group shall be agreed between vendor and customer.
8.2.6.1 Temperature Cycle — Per MIL-STD-883,
Method 1010, Condition C.
8.2.6.2 Thermal Shock — Per MIL-STD-883, Method
1011, Condition B.
8.2.6.3 Vibration Fatigue — Per MIL-STD-883,
Method 2005, Test Condition B.
8.2.6.4 Mechanical Shock — Per MIL-STD-883,
Method 2002, Test Condition B.
8.2.6.5 Constant Acceleration — Per MIL-STD-883,
Method 2001, Test Condition D, “Y” axis only.
8.2.6.6 Moisture Resistance — Per MIL-STD-883,
Method 1004.
8.2.6.7 Additional Testing — Additional tests
performed at package qualification may include
evaluation of electrical and thermal characteristics.
These tests may be performed on a periodic basis to
maintain package qualification.
These tests may include, but are not limited to, the
following:
8.2.6.7.1 Insulation Resistance — Per MIL-STD-883,
Method 1003, Test Condition as agreed between user
and supplier.
8.2.6.7.2 Lead Inductance — Per SEMI Test Method
G23.
8.2.6.7.3 Lead-to-Lead Capacitance — Per SEMI Test
Method G24.
8.2.6.7.4 Lead Resistance — Per SEMI G25.
8.2.6.7.5 Thermal Dissipation — Per MIL-STD-883,
Method 1012.
9 Sampling
The sampling plan, based on MIL-STD-105, shall be
agreed between user and supplier.
SEMI G58-94 © SEMI 1994 6
10 Packaging and Marking
10.1 Packaging — The shipping containers and
materials shall be suitability designed to provide the
components with protection against normal
transportation damage risks which include crushing and
spillage, and exposure to moisture and other corrosive
gases.
The packing materials must not cause particulate
contamination on the components.
10.2 Marking — The shipping container shall be
clearly marked with the following information:
Customer’s Part Number
Customer’s Purchase Order Number
Drawing Number (Customer’s and Vendor’s, if
appropriate)
Quantity
Vendor Lot Number
Shipping date
Figure 1
Chip Illustration
.010
.010
.015
.015
Figure 2
Critical and Non-Critical Seal Areas
overhang
overhang
rundown
external
pullback
window
frame
base
rundown
material
pullback
Figure 3
Glass Misalignment
.005
.015
75%
Figure 4
lead tip
overhang
lead
glass
ceramic base
Figure 5
A
B
L/F
cavity
A-B
2
Š .010 inch
Figure 6